Capabilities · Evidence
Sheet Metal Fabrication Capabilities: From Released Drawing to Packed Part
A buyer evaluating a new supplier needs more than a list of machines. This page states what we do in-house, which steps run through finishing partners, what evidence you can ask for at each stage, and what information we need from you to quote a custom part. The scope is written down before a drawing is sent, so there is no ambiguity later about who is responsible for what.
Drawing-based sheet metal fabrication is the manufacture of parts, enclosures and assemblies from a customer’s released 2D or 3D drawing: cutting flat blanks, conditioning and forming them, joining them, applying the specified finish, inspecting the result and packing it for shipment. The customer owns the design; the supplier is accountable for making the physical part match the drawing and for documenting that match.
Who this page is for
We work with OEM equipment builders, enclosure and cabinet manufacturers, industrial integrators and purchasing teams who already have a released design or a well-defined concept. Typical requests include custom metal enclosures, control cabinets, brackets, frames, chassis, panels and welded assemblies in carbon steel, stainless steel and aluminum.
If you are still at the concept stage, the useful starting point is our free DFM pre-review, where drawing, material, bend and finish decisions are examined before a quotation is issued. If you already have a drawing and a quantity, go to the contact page and send it with the checklist at the end of this page.
What is different in our workshop now
Two pieces of equipment were added recently. Both change what can be checked and controlled inside our own workshop rather than assumed or outsourced.
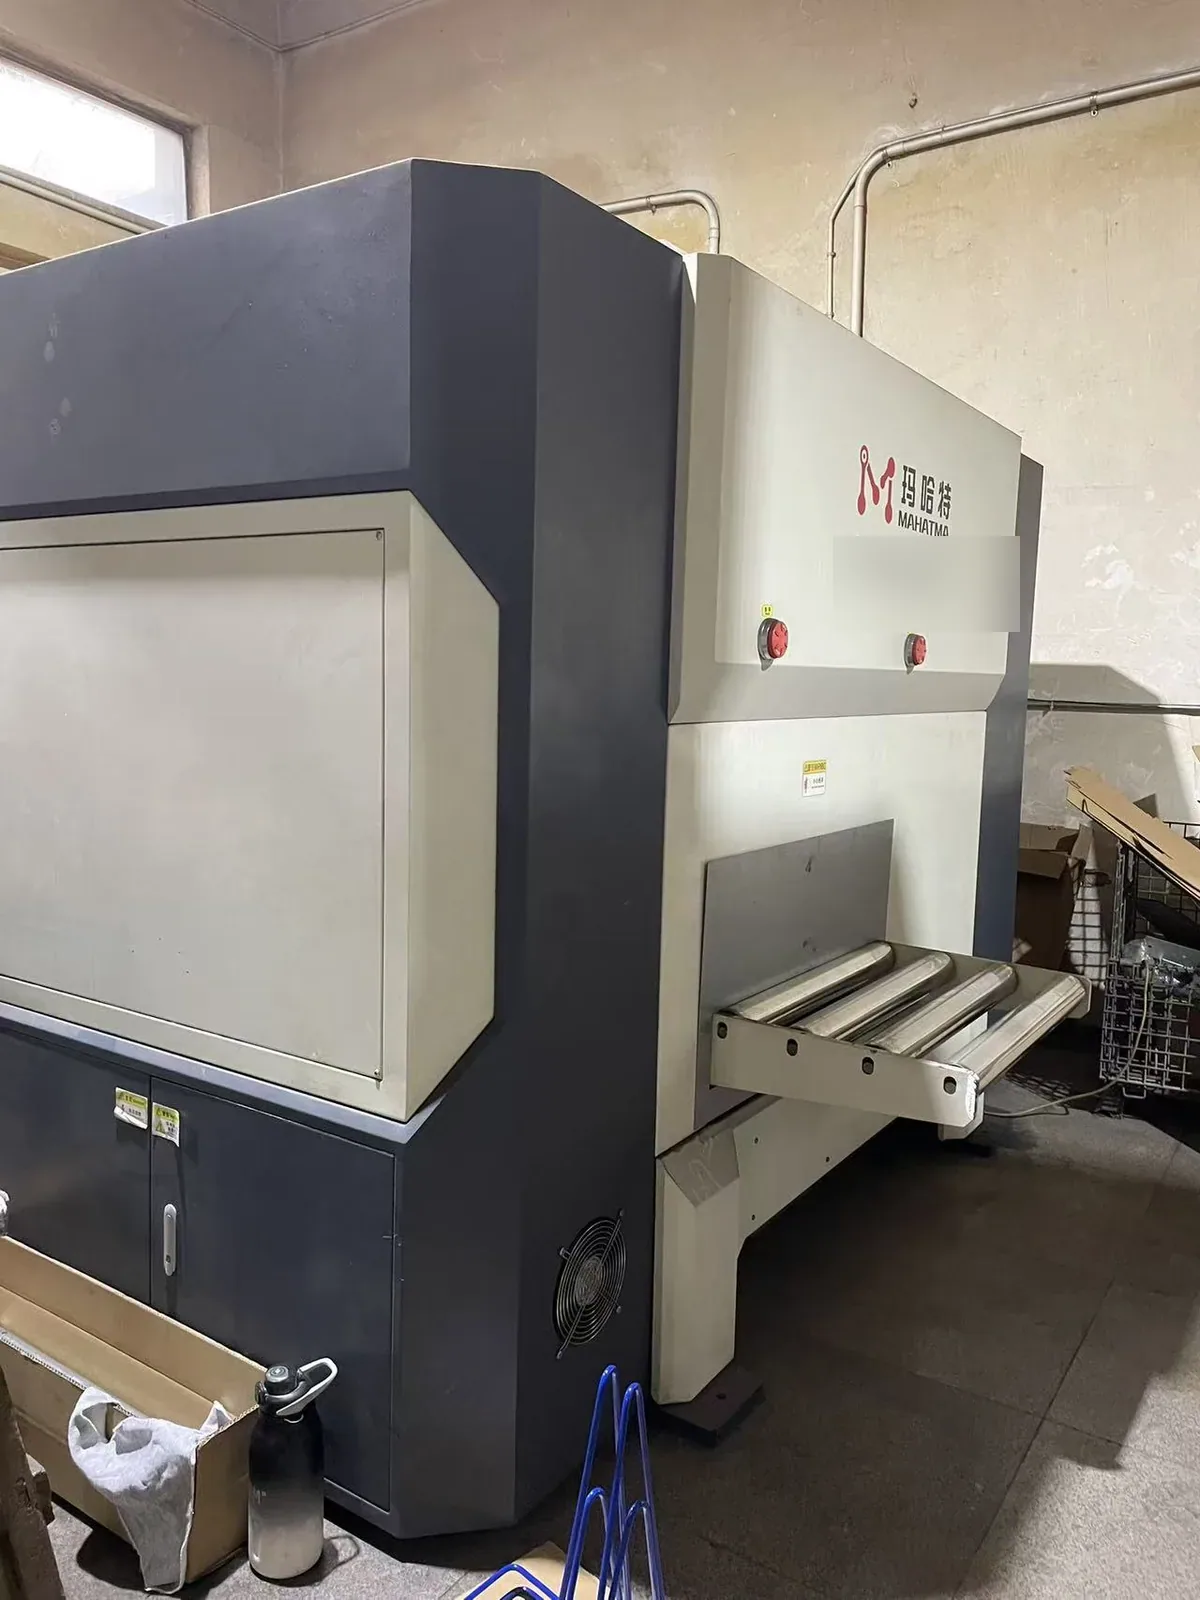
Precision leveling equipment
Used to correct flatness in sheet and cut blanks before they move on to bending. Flatness at this stage reduces variation downstream, particularly on thin or wide parts where residual stress from coil or laser cutting shows up as inconsistent bend angles. It is a conditioning step on the flat blank, not a finishing repair after a part has been welded.
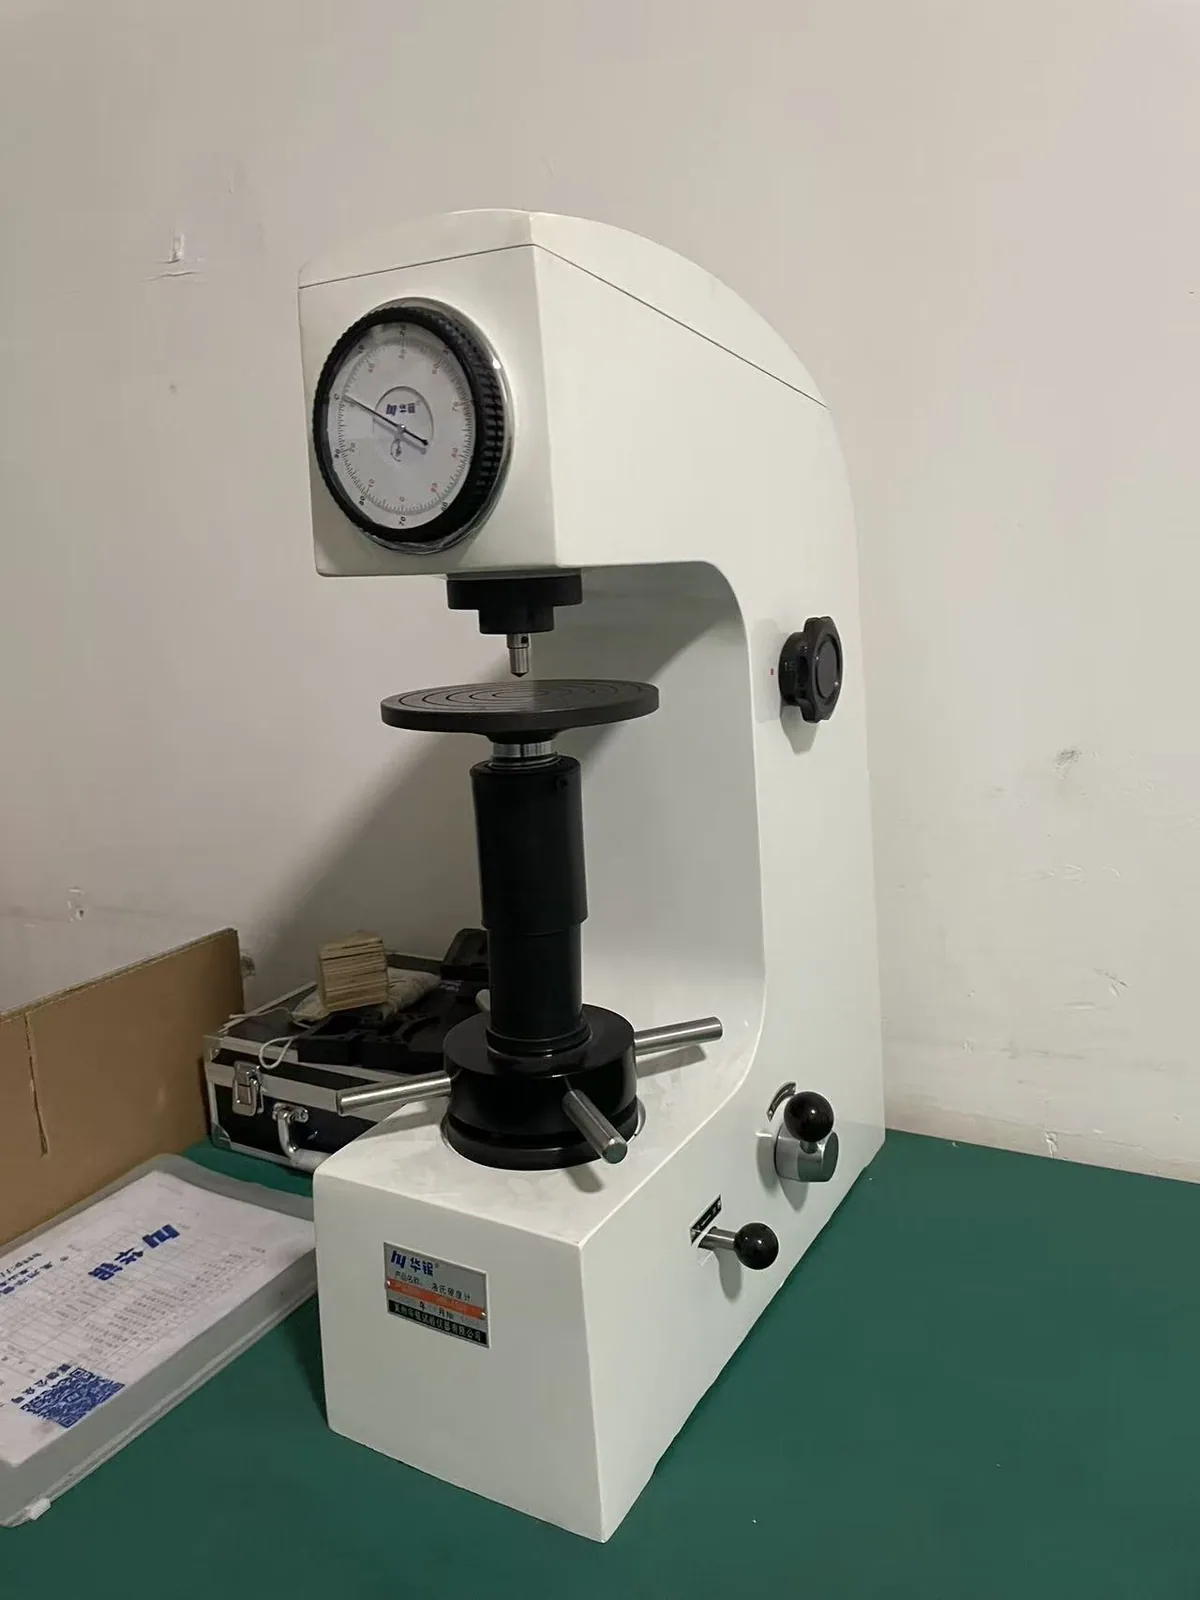
Bench hardness tester
An in-house check on incoming and processed material. Hardness test reports can be issued on request. The exact test scope for your order is agreed before production, so the record matches what your quality team actually needs.
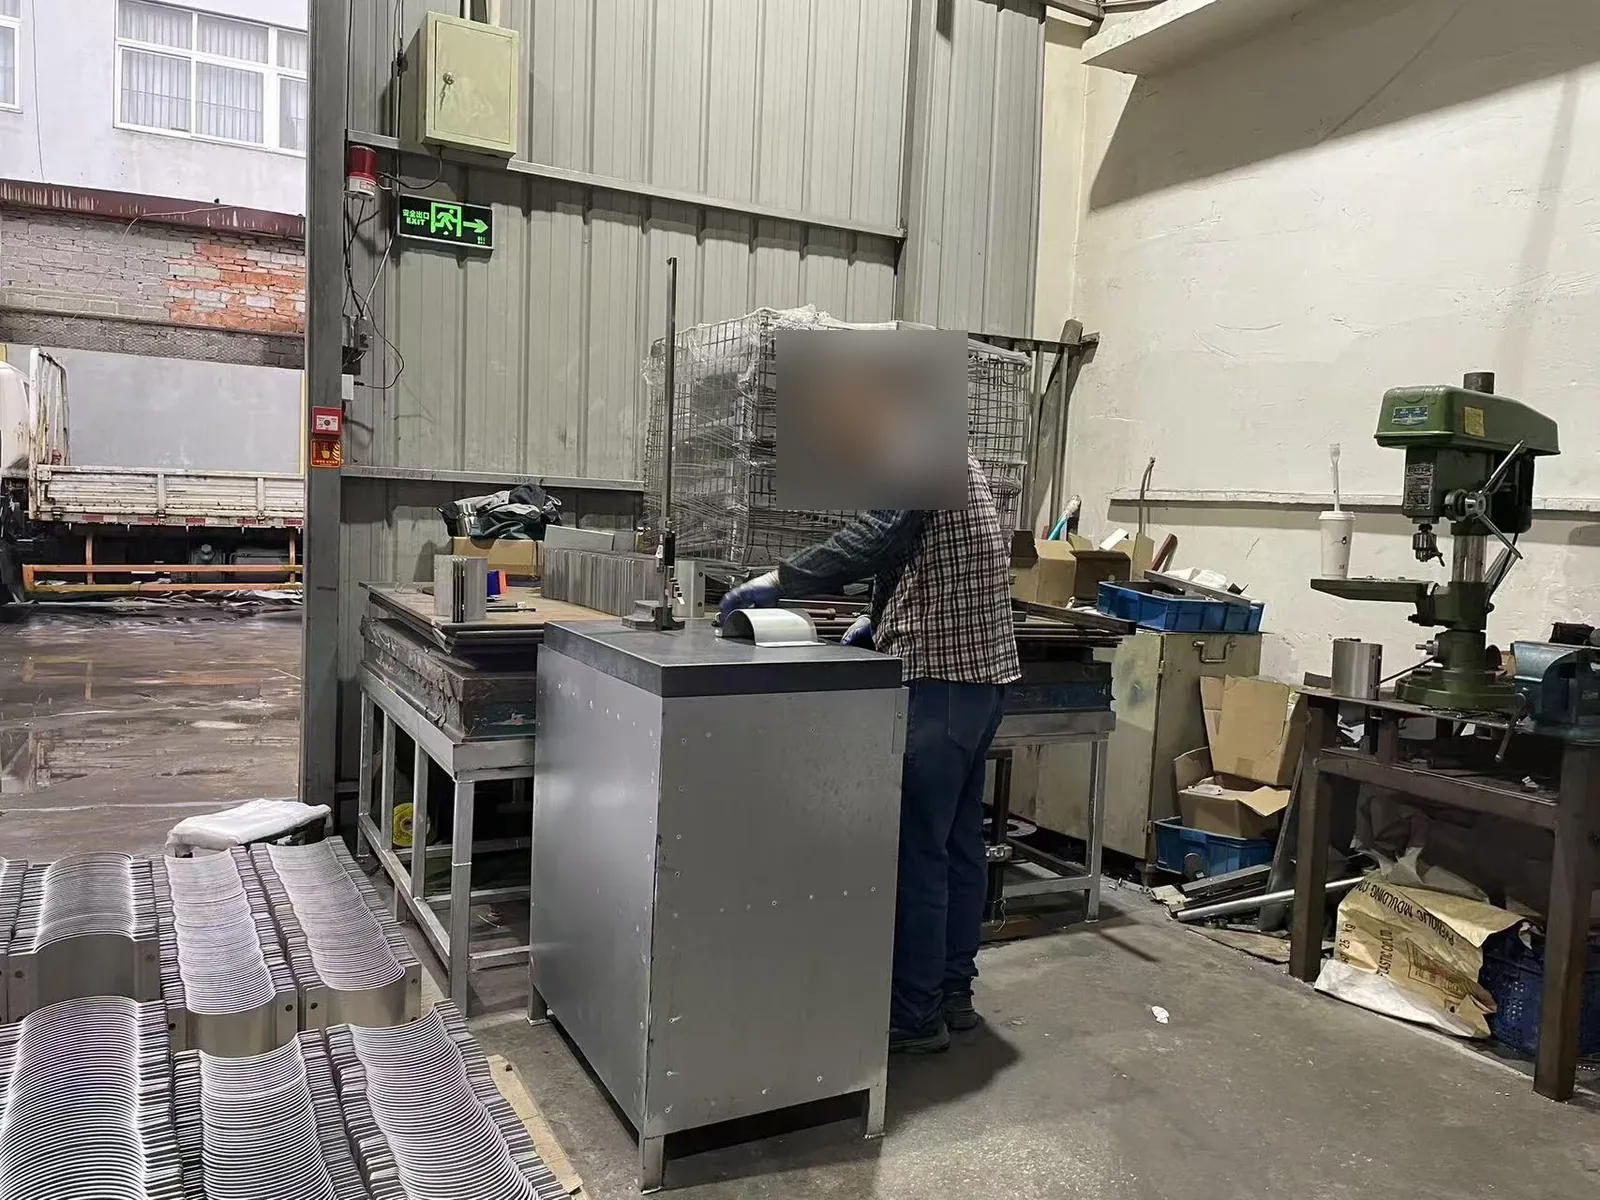
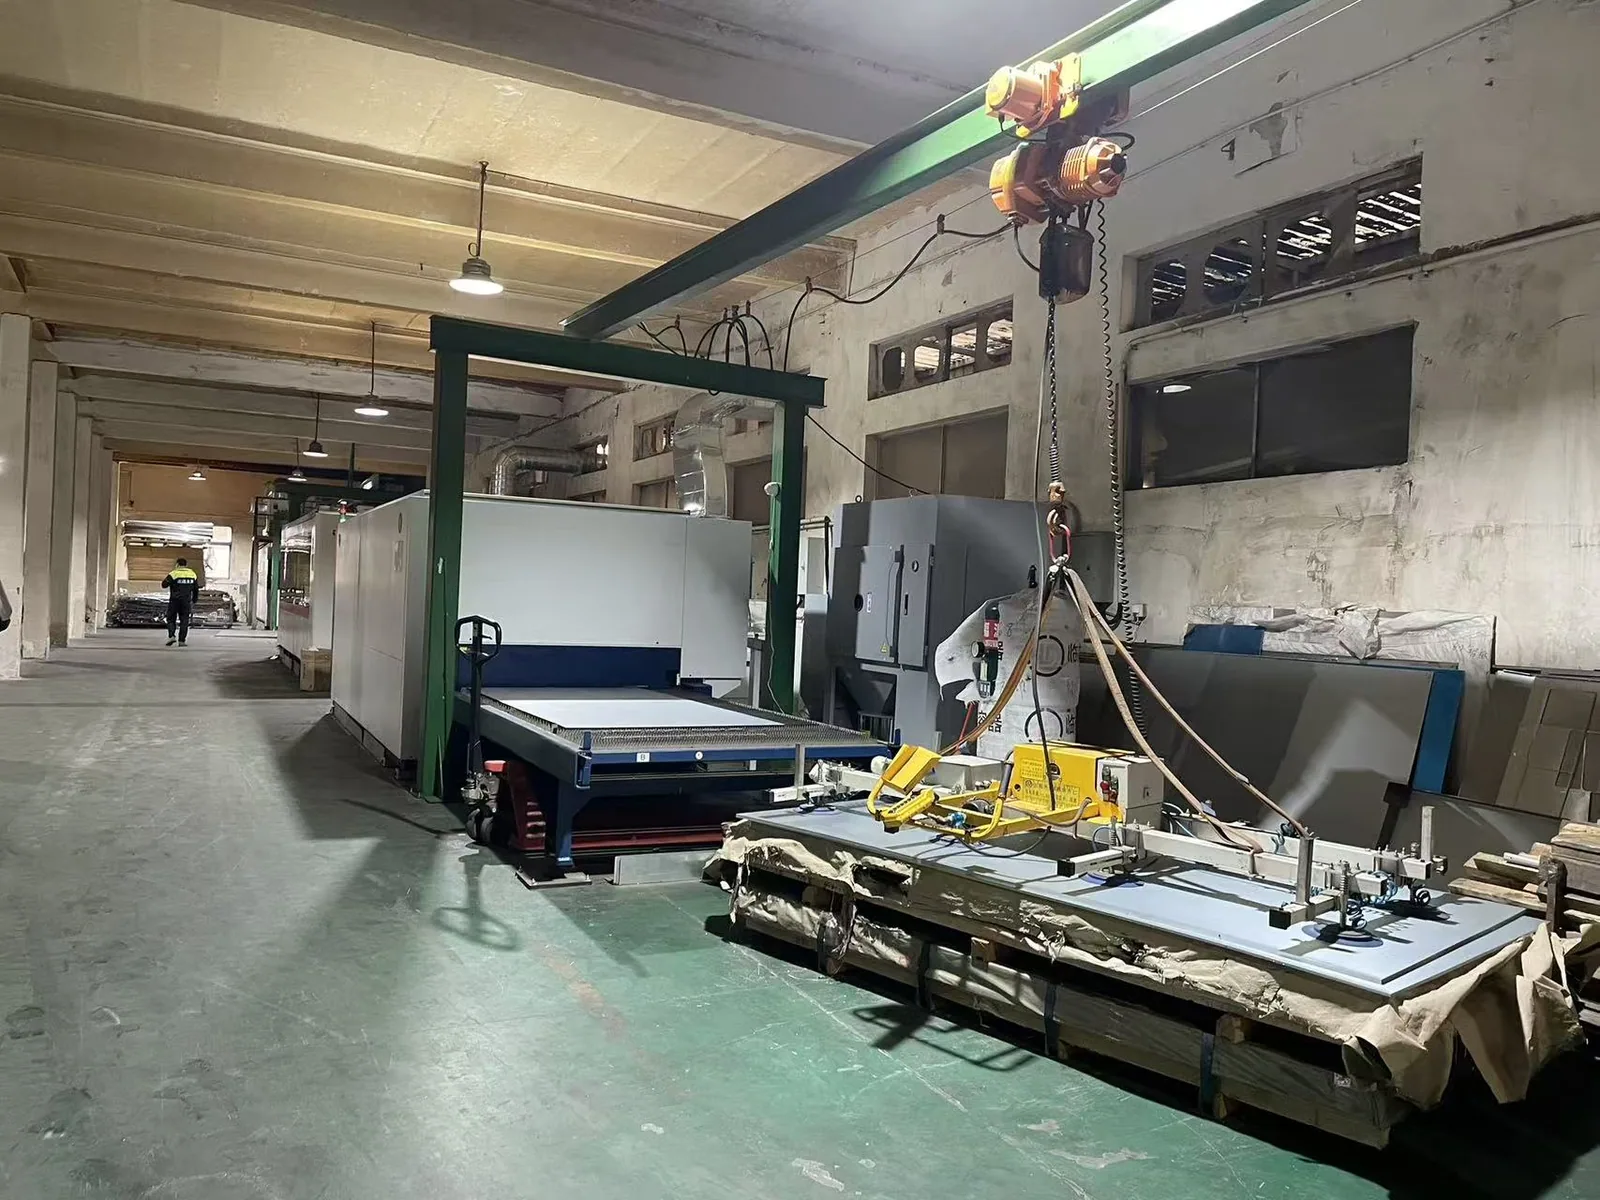
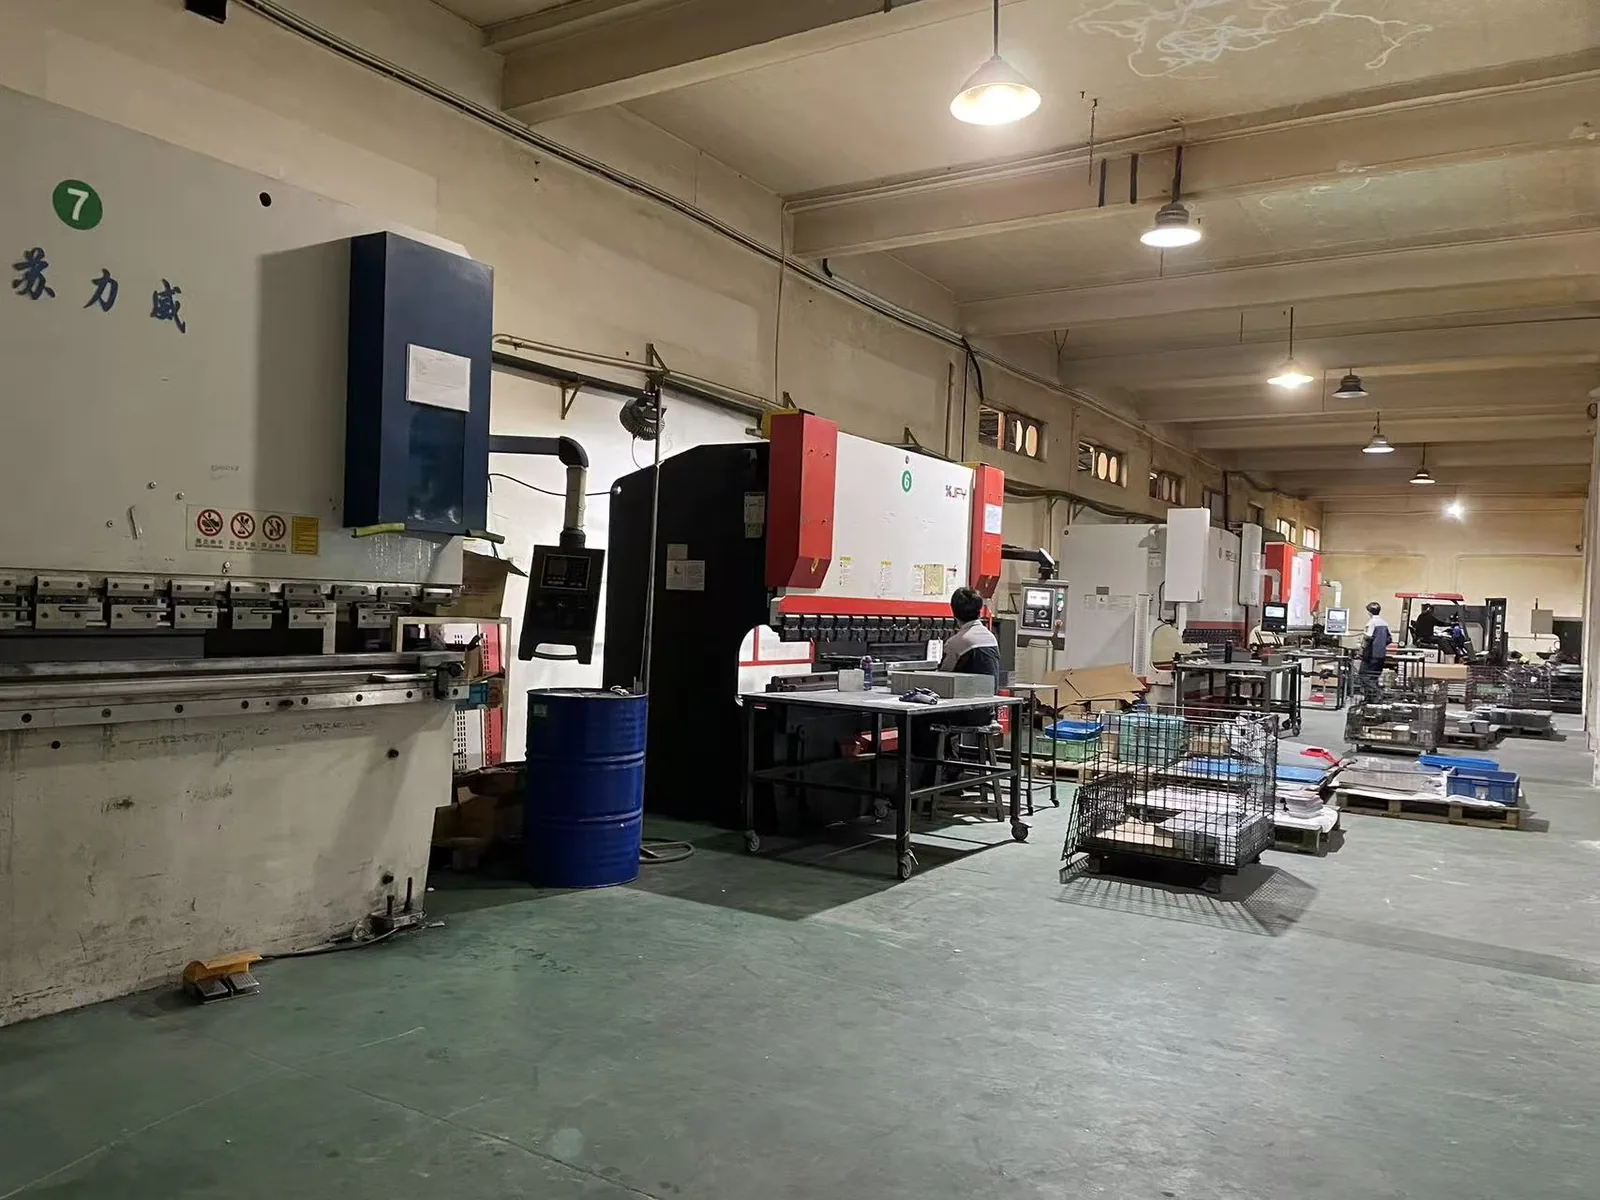
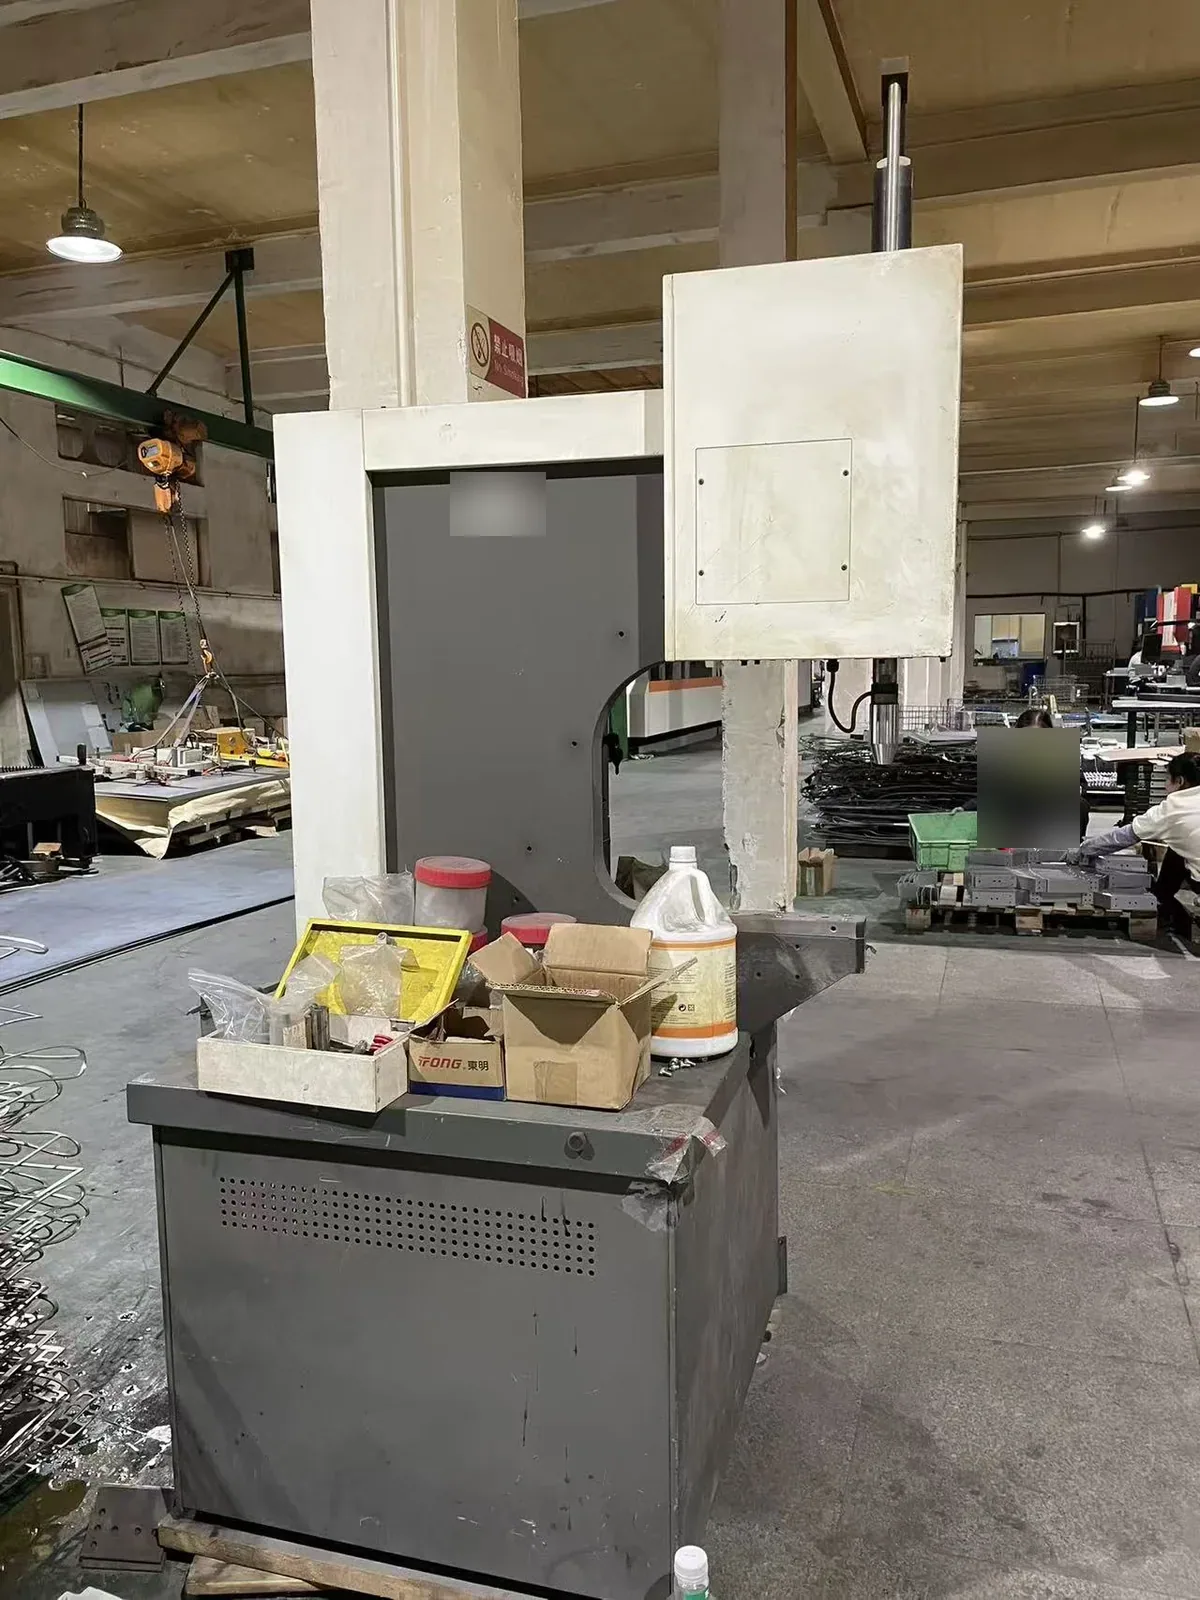
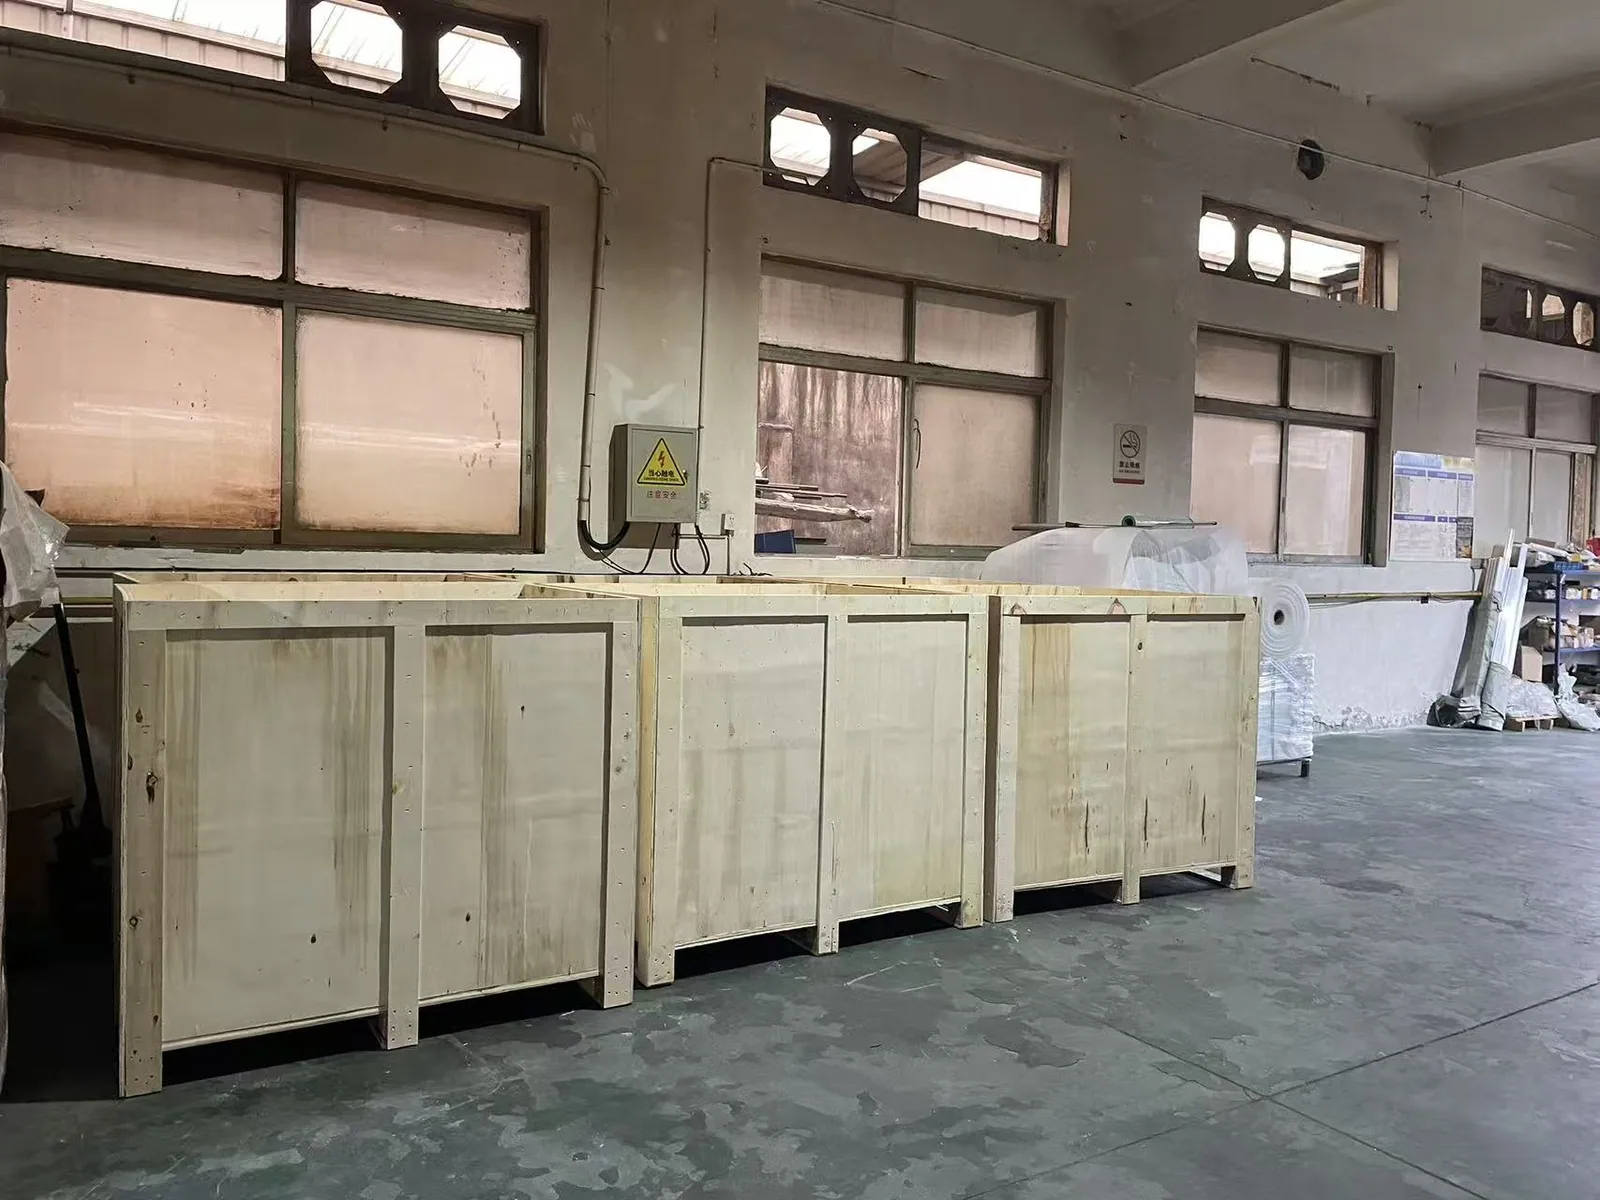
Both are operated in our own workshop. The photographs below are shop-floor evidence of equipment and working practice; they are not product photographs and they do not show customer parts.
For why flatness is decided before the press brake, see Why flatness is decided before the press brake.
Capability map
This table is a scope statement, not a performance guarantee. Every line describes a step we carry out and the kind of record a buyer can ask to see for it.
| Process | What we do | Where | Evidence you can request |
|---|---|---|---|
| DFM pre-review | Drawing, material, bend radius, hardware and finish review before quoting | In-house | Written review notes, open questions list |
| Precision leveling | Flatness correction of sheet and cut blanks before forming | In-house | Before/after part photograph |
| Laser cutting | Flat blanks cut to the released drawing | In-house | Cut part photograph, material identification |
| CNC bending | Forming to the specified angles and flange lengths | In-house | Bend sample for review before a batch continues |
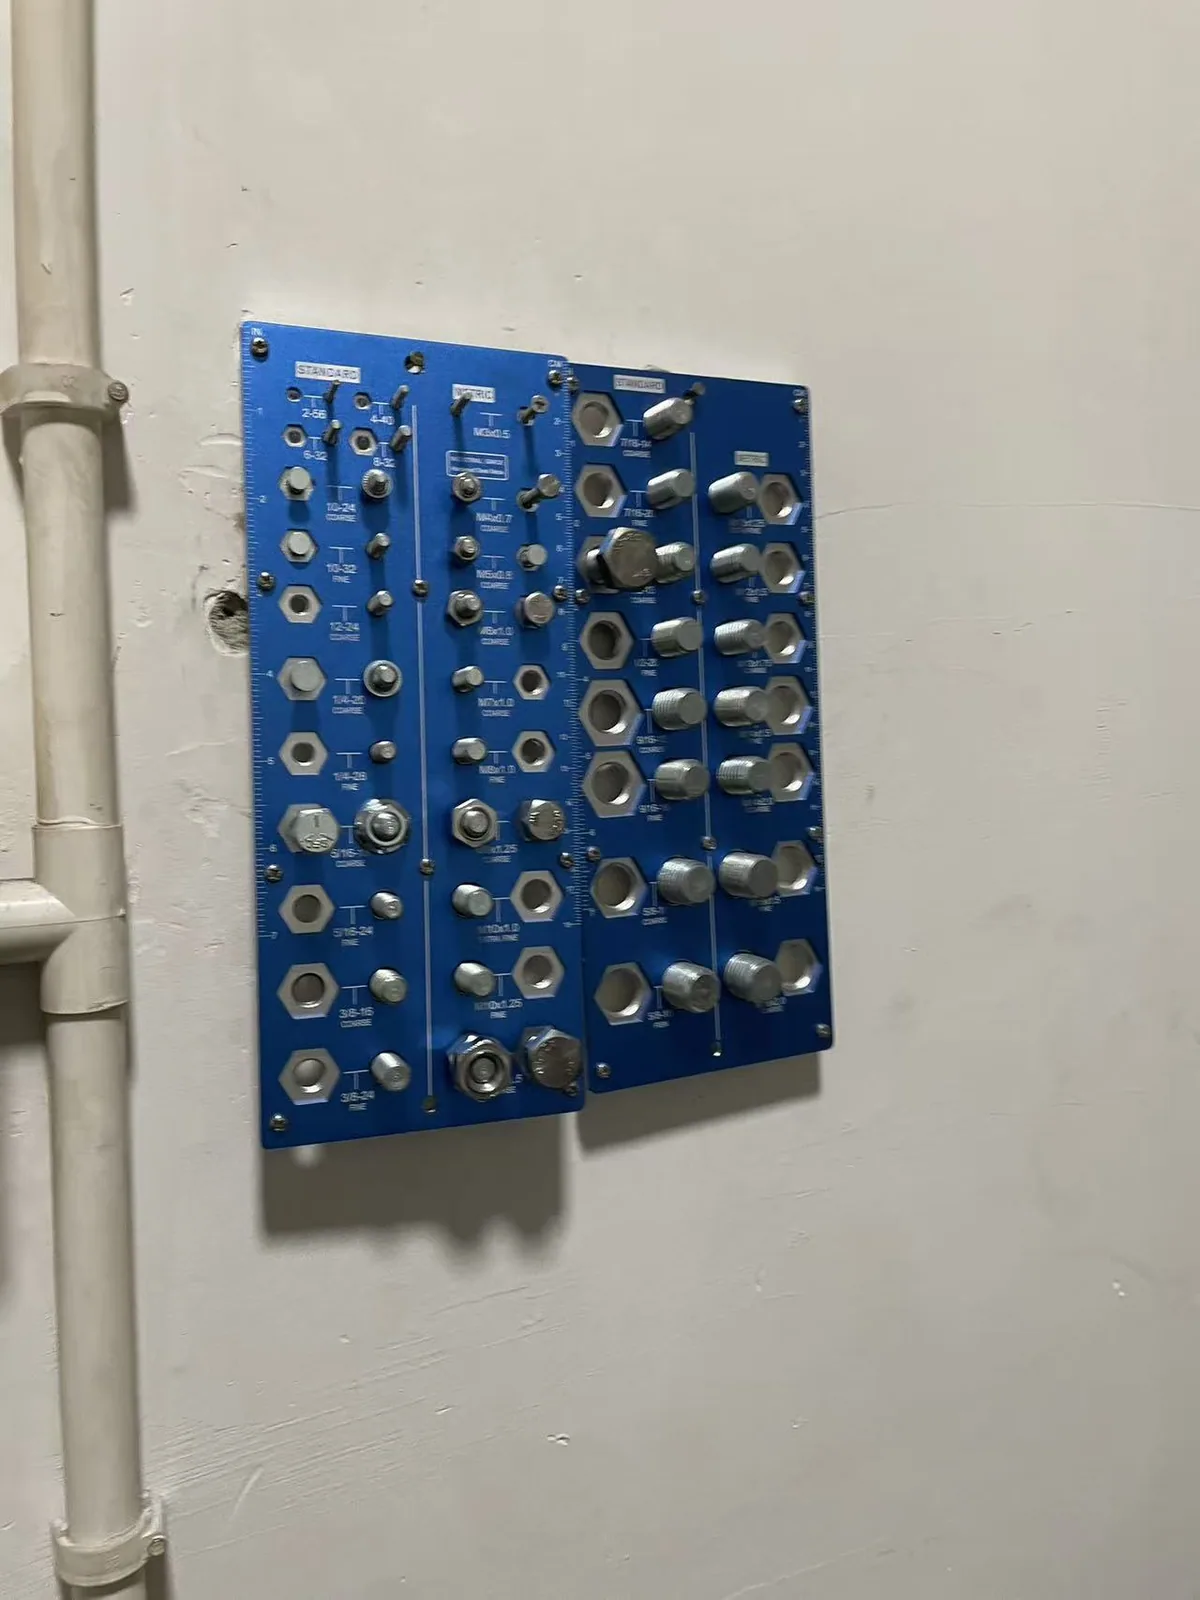
| Riveting & hardware insertion | Riveting and installation of nuts, studs and standoffs | In-house | Fastener sample board, assembly photograph |
| Welding & assembly | Frames, cabinets and housings assembled to drawing | In-house | Assembly and weld photographs |
| Brushed / mirror finish | Mechanical surface finishing of visible metal | In-house | Approved finish sample panel |
| Powder coating, anodizing, passivation, plating | Coating and conversion finishes | Finishing partners | Finish sample, coating record on request |
| Inspection | Dimensional checks and hardness testing | In-house | Dimensional record, hardness test report, photos |
| Export packing | Cartons on wrapped pallets, wooden crates for finished assemblies | In-house | Packing photographs |
Where a step runs through a finishing partner, we agree the scope of that step and the required record with you before the order is released.
Equipment and capacity
| Area | What is installed | Why it matters to a buyer |
|---|---|---|
| Workshop | 2,500 m² of production space, four production lines | Cutting, forming, joining and packing can run under one roof, with one accountable party for the whole drawing. |
| Laser cutting | Three laser cutting machines: two 3000 W and one 6000 W | Covers both thin sheet work and heavier plate within our stated thickness ranges. |
| CNC bending | Four 250 t CNC press brakes with a 3000 mm bed | Long flanges and larger enclosure panels can be formed without splitting the part. |
| Welding & assembly | Ten welding stations | Frames, cabinets and housings are assembled in-house rather than brokered out. |
| Joining hardware | Riveting equipment and a fastener sample board | Hardware can be confirmed against a physical part before assembly starts. |
| Inspection | Dimensional hand instruments and a bench hardness tester | Records can be produced against the agreed inspection scope. Hardness test reports can be issued on request. |
Plain statement about inspection equipment: our dimensional inspection uses calibrated hand instruments rather than coordinate measurement. Dimensional checks are recorded with calipers, micrometers and gauges. If your specification requires a particular inspection method, tell us at RFQ stage so we can confirm whether it is available before you commit.
Materials and thickness ranges
| Material family | Grades we work with | Thickness range |
|---|---|---|
| Carbon steel | Q235B and equivalent structural sheet | 0.5–18 mm |
| Stainless steel | SUS 304, 316, 430 | 0.5–15 mm |
| Aluminum | 5052, 5754, 6061 | 0.5–10 mm |
Ranges are for guidance against a released drawing. A specific combination of grade, thickness, bend radius and finish should be confirmed during the DFM pre-review rather than assumed from this table. If your part needs a grade that is not listed, include it on the drawing and we will confirm availability at quotation stage.
Process sequence, step by step
Not every part needs every step. The sequence is agreed during the free DFM pre-review before a quotation is issued.
- DFM pre-reviewDrawing, tolerances, bend radii, hardware, finish and packing requirements are reviewed; open questions go back to you before pricing. Output: a written scope and an open-questions list.
- Laser cuttingFlat blanks are cut from the released drawing. Output: cut blanks with material identification. Ask for: cut part photograph.
- Precision levelingWhere the part or material calls for it, blanks are conditioned for flatness before forming. Output: a flat blank ready for the press brake. Ask for: before/after photograph.
- CNC bendingBlanks are formed to the specified angles and flange lengths. Output: formed parts. Ask for: a bend sample for approval before a batch continues. See CNC bending.
- Riveting / hardware insertionNuts, studs and standoffs are installed, or joints are riveted. Output: assembled sub-parts. See PEM fastener and hardware installation and Rivets, PEM hardware or welding.
- Welding and assemblyFrames, cabinets and housings are joined to drawing. Output: welded assembly. See sheet metal welding.
- Surface finishBrushed and mirror finishing run in-house; powder coating, anodizing, passivation and plating run through finishing partners. Output: finished part. Ask for: an approved finish sample panel.
- InspectionDimensional checks are recorded against the agreed scope; hardness testing is available in-house with reports on request. See quality inspection and first article inspection.
- Export packingFinished parts are packed in cartons on wrapped pallets or in wooden crates. See export packaging.
Surface finishing: what is in-house and what is not
| Finish | Where | What to settle on the drawing |
|---|---|---|
| Brushed / mirror | In-house | Direction of the grain, which faces are visible, and whether a sample panel must be approved first. |
| Powder coating | Finishing partner | Colour reference, gloss level, coverage of edges and holes, and whether an approved sample is required. |
| Anodizing | Finishing partner | Aluminum grade compatibility, colour, and which surfaces must be masked. |
| Passivation | Finishing partner | Stainless grade and the required surface condition before treatment. |
| Plating | Finishing partner | Coating type, thickness requirement if specified, and functional surfaces that must stay uncoated. |
Colour approval is handled against a physical sample rather than a screen image. We keep colour approval sample panels in the workshop so that a finish is agreed on a real part before a batch is released. Colour references are project-specific; we do not publish colour codes or substitute one customer’s approved colour for another’s.
Inspection and records
Dimensional checks are recorded with calipers, micrometers and gauges. Hardness testing is available in-house and hardness test reports can be issued on request. The report set for your order is agreed before production, which avoids the common problem of receiving a generic inspection sheet that does not match the drawing’s critical dimensions.
Our quality system is documented to ISO 9001. We do not hold a third-party ISO 9001 certificate and do not claim one. Third-party audit references are available on request. Any method-specific requirement beyond the above should be raised at RFQ stage.
Lead-time bands and ordering
| Stage | Typical band | What moves the date |
|---|---|---|
| Simple sample | 3–7 days | Drawing completeness, material availability, whether a finish is required. |
| Complex first article | 15–20 days | Number of forming steps, hardware, welding, external finishing and approval rounds. |
| Volume production | 25–35 days | Batch size, approved sample, finishing capacity and packing specification. |
These are planning bands for custom work, not fixed delivery promises. A firm schedule is stated in the quotation once the drawing and quantity are known. Pricing is quoted case by case against the released drawing; we do not publish a price list because material, forming, joining, finishing and packing all depend on the part.
What we do not publish
We do not show one customer’s design to another buyer, and we do not publish customer company names, drawings, part dimensions or load values. Confidential by default — your drawings are used only for your own project, are never shared, resold or reused. Our documented product cases describe process routes and materials, not customer identities. Read the full information protection page before sending a drawing if your compliance team needs it.
What we need from you to quote
The fastest quotations come from a complete package. Send as much of the following as you have; missing items become open questions rather than assumptions.
- Released 2D drawing with critical dimensions and tolerances, plus a 3D model or flat pattern if available.
- Material grade and thickness, or the performance requirement if the grade is still open.
- Quantity for the sample, first article and expected volume, plus any repeat-order pattern.
- Finish requirement, visible faces, and whether a colour or finish sample must be approved first.
- Hardware part numbers or accepted equivalents, and the joining method if it is specified on the drawing.
- Inspection scope and the records your quality team needs with the shipment.
- Packing and shipping requirement: pallet, wooden crate, labelling, destination and incoterm.
Shop-floor evidence
The photographs below show equipment and working practice in our own workshop. They are process evidence, not a product catalogue, and they contain no customer-specific parts.
FAQ
- Do you work from our drawing or do you design the part?
- We fabricate from a customer’s released drawing. We do not take ownership of product design, but we do review drawings for manufacturability during the free DFM pre-review and raise open questions before quoting.
- Which parts of the process are outsourced?
- Powder coating, anodizing, passivation and plating run through finishing partners. Cutting, leveling, bending, riveting, hardware insertion, welding, assembly, inspection and export packing are in-house. The split is stated in the quotation, not hidden in the small print.
- Can I get inspection records with my order?
- Yes. Dimensional checks are recorded with calipers, micrometers and gauges, and hardness test reports can be issued on request. Agree the exact report set before production so it matches your drawing.
- Do you hold an ISO 9001 certificate?
- Our quality system is documented to ISO 9001. We do not hold a third-party ISO 9001 certificate and do not claim one. Third-party audit references are available on request.
- Do you use coordinate measurement for inspection?
- No. Our dimensional inspection uses calibrated hand instruments. If your specification requires a particular inspection method, raise it at RFQ stage so we can confirm whether it is available before you commit.
- What thicknesses and materials can you handle?
- 0.5–18 mm carbon steel, 0.5–15 mm stainless steel (SUS 304 / 316 / 430) and 0.5–10 mm aluminum (5052 / 5754 / 6061). Confirm a specific combination during the DFM pre-review.
- How long does a custom order take?
- Planning bands are 3–7 days for a simple sample, 15–20 days for a complex first article and 25–35 days for volume production. A firm date is stated in the quotation once the drawing and quantity are known.
- How is pricing set?
- Pricing is quoted case by case against the released drawing, material, forming steps, joining, finishing, inspection scope and packing. We do not publish a price list for custom work.
- Will my drawing or part be shown to other buyers?
- No. Confidential by default — your drawings are used only for your own project, are never shared, resold or reused. See how we protect your information.
- Where do you ship?
- We have quoted buyers in and shipped to 30+ countries. Packing is specified per order; see export packaging.
Send a drawing, get a defined scope
Send your released drawing, material, quantity, finish and inspection requirements. We will come back with a free DFM pre-review, the open questions, and a quotation that states clearly what runs in-house and what runs through a finishing partner.