
Repeat-production assembly knowledge
Sheet Metal Assembly: Process, Fixtures and Quality Gates
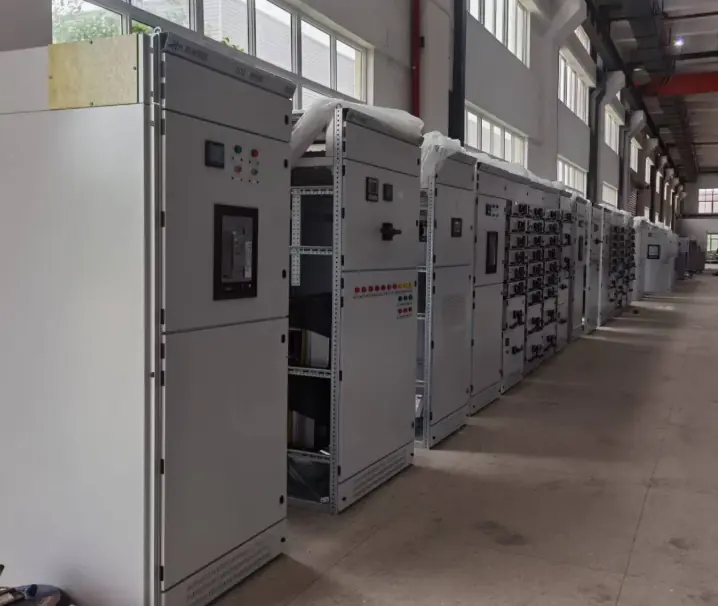
Sheet metal assembly is the stage where separately fabricated parts become one working product. It depends on a controlled BOM, a defined work sequence, stable mating geometry, correct hardware and a check at the end of each step — not one inspection at the end of the build.
Buyer summary
What Sheet Metal Assembly Covers
Assembly is not one operation. It is a sequence of steps with different risks at each one, which is why the useful questions at enquiry stage are about sequence, ownership and gates rather than about labour rate.
| Scope | Sub-assembly and final assembly of fabricated sheet metal parts — brackets, panels, frames, housings and closures |
|---|---|
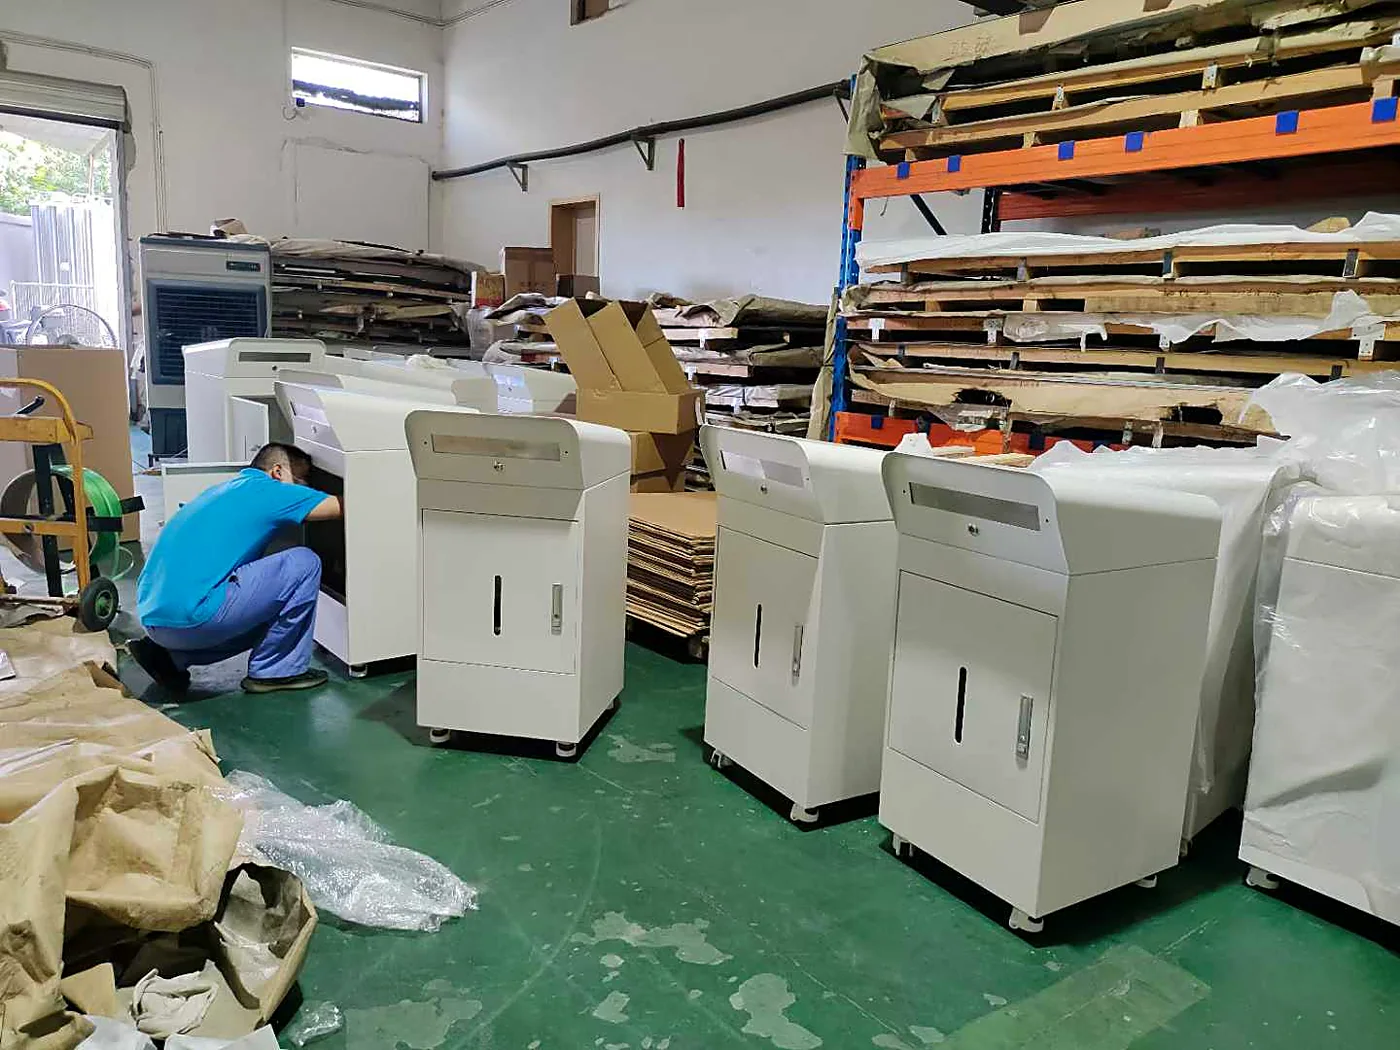
| Typical products | Enclosures and cabinets, machine guards, trolleys and carts, shelving and display units, equipment frames |
| Materials in scope | SPCC cold-rolled steel, galvanised steel, SUS304 / SUS316L, 5052 aluminium |
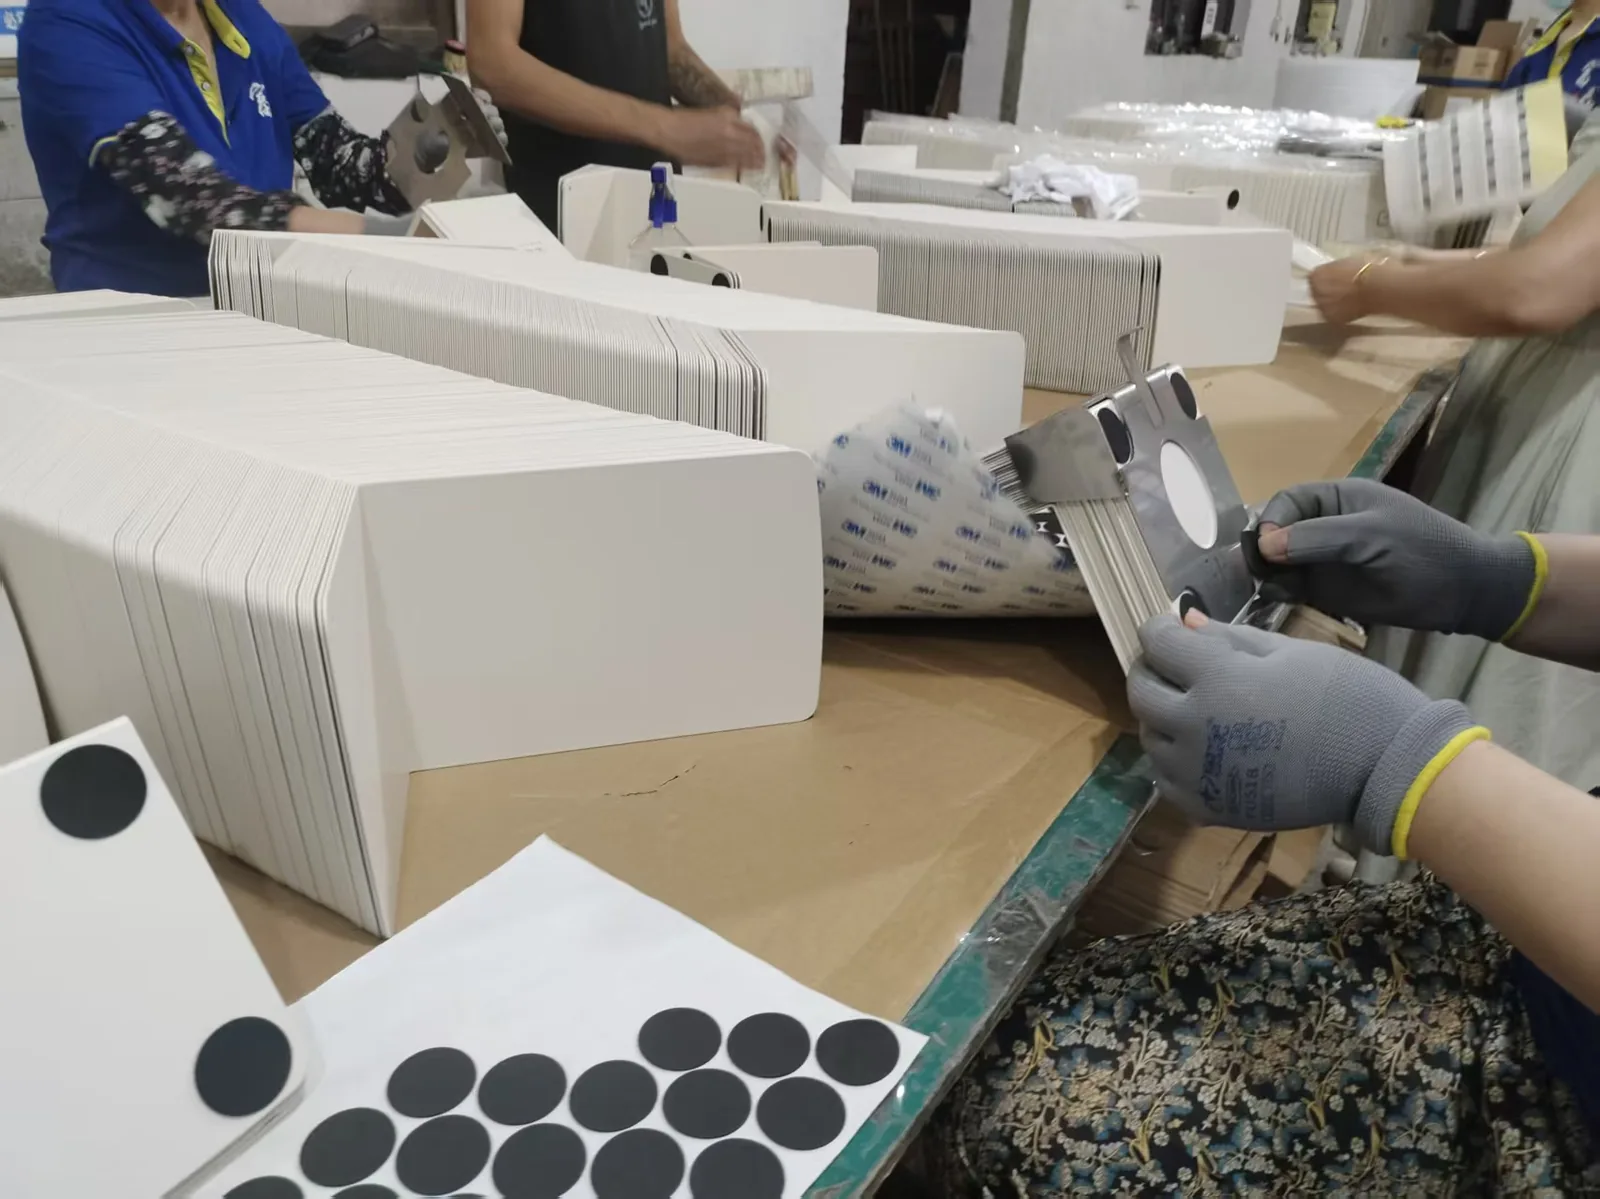
| Joining methods | Mechanical fasteners, rivets, rivet nuts, self-clinching hardware, spot and MIG / TIG welding, adhesive pads |
| Hardware | Buyer-supplied or sourced — hinges, locks, handles, castors, rails, seals, gaskets, earth studs |
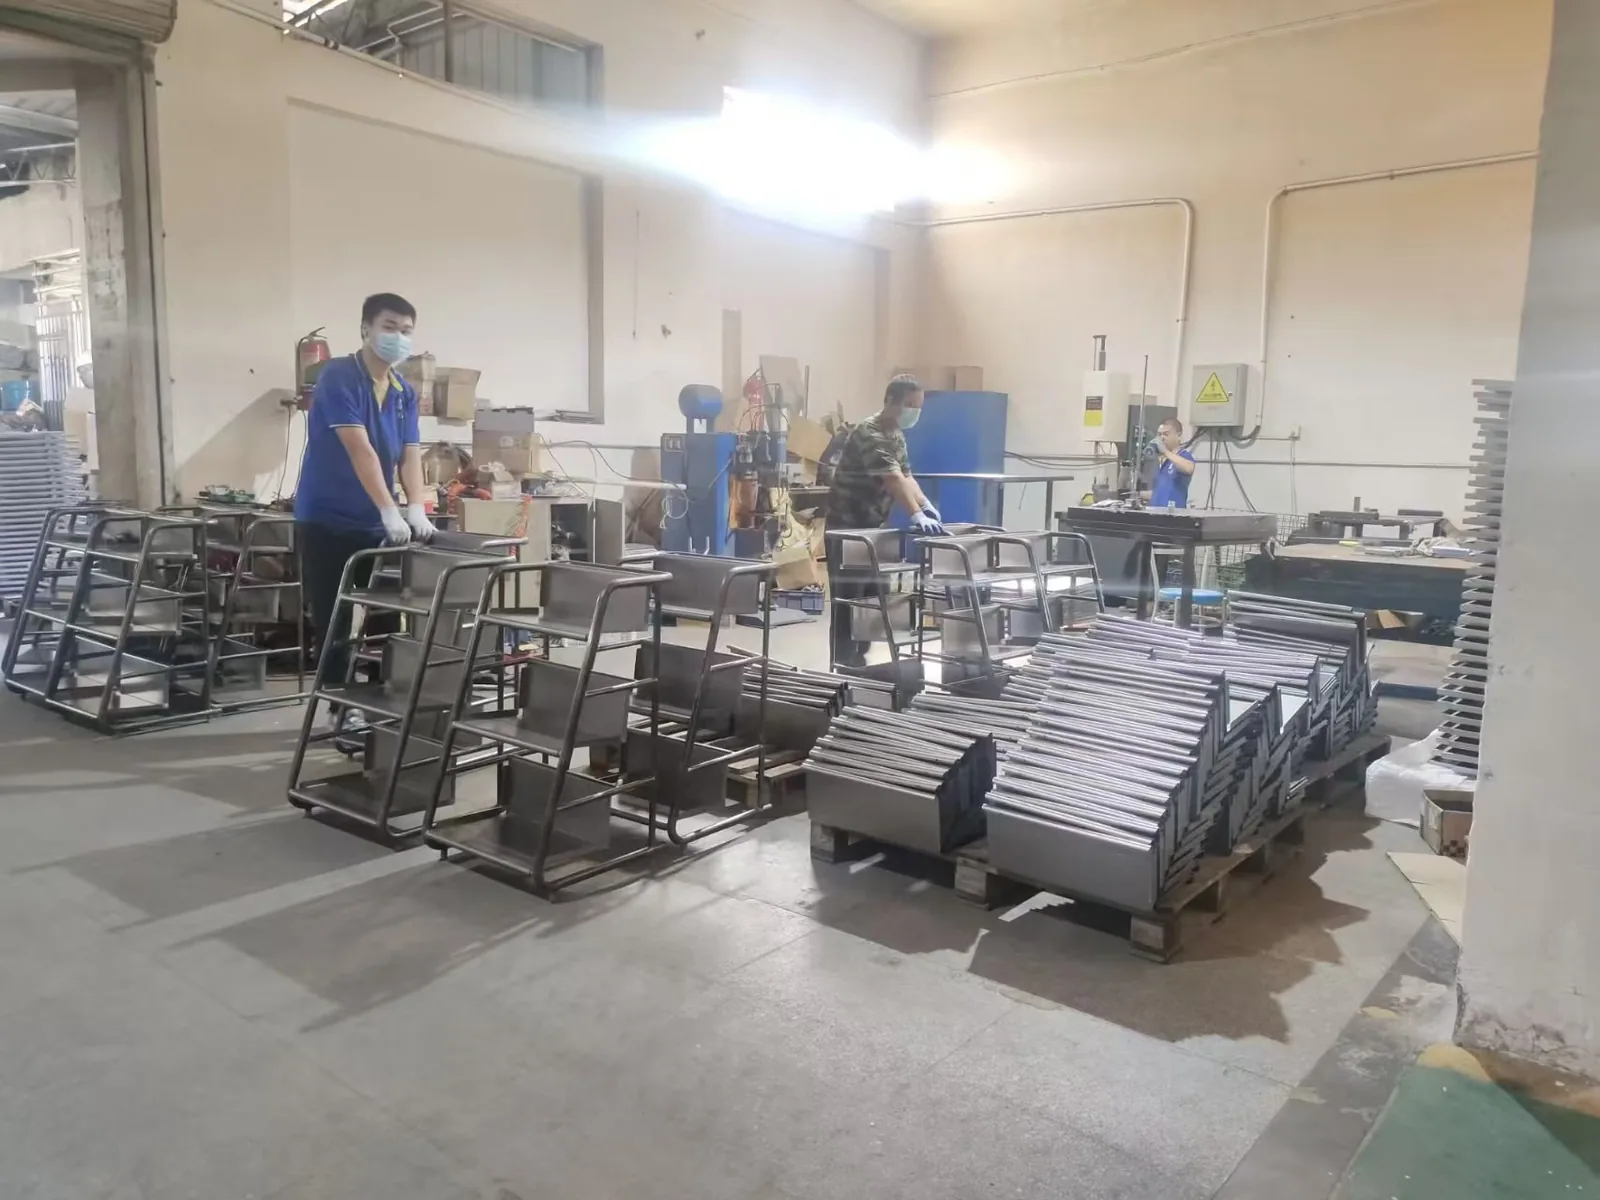
| Fixtures | Assembly jigs and locating fixtures where the geometry repeats across a batch |
| Batch size | Single prototype units through to repeat production batches |
| Quality gates | In-process checks at defined points, plus a final functional and cosmetic inspection before packing |
| Documentation | Approved work sequence, first-piece record, and project-agreed inspection or packing photographs |
Sequence
Assembly Sequence, and the Check That Ends Each Step
A sequence is only repeatable if each step has an exit condition. These are the eight steps we run on a repeat build, and what has to be true before the unit moves on.
- Incoming verification of fabricated partsParts arrive from cutting, bending, welding and coating. Each is checked against the drawing before it enters the assembly area: hole positions, formed angles, coating film and the condition of any tapped thread. A part that is out of tolerance is far cheaper to correct before five others have been bolted to it.
- Kit the hardware for the unitHardware for one unit is picked as a kit before assembly starts, not collected as the operator goes. A missing fastener found halfway through is the most common reason a unit stalls and then gets finished from memory instead of from the sequence.
- Set the datum and locate the frameThe first parts position everything that follows, so the datum surface or fixture is established before anything else is fixed. On units where doors or panels have to sit flush, this is the step that decides whether the finished gaps are even.
- Build the sub-assembliesDoors, panels and brackets are built as sub-assemblies wherever the design allows. A sub-assembly on a bench is easier to check and easier to correct than the same work done inside a closed shell.
- Install internal fittings before closing panelsRails, gland plates, mounting plates, earth studs and cable management go in while the unit is still open. Anything fitted through an aperture after the panels are on is slower and more likely to end up at an angle.
- Fit doors, panels and closuresHinges, gaskets, locks and handles are fitted and adjusted with the unit square on a flat surface, not standing on an uneven floor. Gasket compression and lock engagement are checked with the door closed against the finished gasket, because that is the condition the seal has to work in.
- Apply hardware torque to specificationFasteners are tightened to the stated torque rather than until they feel tight. Where the drawing calls for thread locking or a sealing washer, it is applied at this step — not added later by someone who assumes it was already done.
- Final function and cosmetic check, then packDoors operate, hardware engages, the accessory kit is counted and the coating is checked for handling damage. Packing is the last gate, because transit damage and missing accessories are both found by the customer if they are not found here.
Design decisions
Six Decisions That Decide Whether It Assembles
Most assembly problems we are asked to sort out are not assembly faults. They were decided at drawing stage, and then had to be solved on the bench.
Datums and common reference points
A unit can contain panels that each pass inspection and still not assemble, because the error is in the reference rather than in the parts. State the datum scheme on the assembly drawing so hole positions, door gaps and panel alignment are all measured from the same place.
What we need: the assembly drawing with datums marked, or a written note on what the alignment is measured from.Tolerance stack, not single-part tolerance
Every part in a chain can be inside its own tolerance while the assembly is out of tolerance. Identify the parts that actually set door gaps, panel flushness and mating hole positions, tighten only those, and leave the rest at general tolerance. Loosening a non-critical part is usually free.
What we need: which dimensions are functional, and which are reference only.Fastener access and installation order
A fastener that cannot be reached with the specified tool, or that has to be fitted before another part is already in place, will be discovered on the bench rather than on the drawing. Check the order in the 3D assembly: what has to go in first, and with what.
What we need: the assembly model, or a note listing any component that must be installed in a fixed order.Component ownership and revision control
The BOM has to state which item is supplied by the buyer and which by the factory, and it has to sit under revision control. A visually similar hinge or fastener with a different length or material changes the fit, and sourcing it locally is not a substitute for approval.
What we need: a controlled BOM with ownership marked, and the approval route for substitutions.Fixture strategy, chosen per project
Fixtures pay for themselves where the geometry repeats: door frames, multi-panel enclosures, parts carrying several hinges. On a one-off unit, locating blocks and a check against the drawing are usually more sensible than a welded jig. This should be a decision per project, not a default.
What we need: the batch size and a view on how much re-orientation is acceptable.Service access after delivery
Assembly has to leave the unit serviceable: hinges, filters, fans, gland plates and internal rails replaceable without dismantling unrelated structure. It is a design decision, and it is cheapest to make before the parts are cut.
What we need: any maintenance requirement, and which items the end user is expected to reach.Quality
Quality Gates and What Each One Catches
Checking every feature only at final assembly hides the cause of the problem. Each gate below exists because it catches something that becomes expensive later.
Incoming check on fabricated parts
Catches cut and formed dimensions, hole positions, thread condition and coating quality before anything is built on top of them. This gate saves the most rework, because every step downstream inherits whatever it misses.
Sub-assembly check
Catches orientation and hardware errors while the sub-assembly is still open and accessible. A door built the wrong way round costs minutes to correct at this point and a complete rebuild if it is found after the unit is closed.
Fit check with doors and closures
Catches uneven gaps, frame twist, gasket compression and lock engagement. The check has to be done with the unit square and against the finished gasket, or it measures the wrong condition.
Torque and hardware audit
Catches fasteners tightened by feel, missing washers and thread locking that was assumed rather than applied. It is a short check, and it is the only way to know the torque specification was followed on a unit you did not watch being built.
Final function, count and cosmetic check
Catches inoperative doors and locks, missing accessories and coating damage from assembly and handling. It is the last point before the carton, so it is the last chance to find these things ourselves rather than let the customer find them.
Layout
Assembly Layout, Matched to Volume and Mix
Assembly layout is a function of two numbers: how many units are built, and how many different variants pass through. Everything else follows from those.
| Layout | Suited to | Footprint and investment | Trade-off |
|---|---|---|---|
| Fixed position | Large or heavy products built in one place, at low volume | Low investment, high space per unit | Materials and tools come to the product, so handling dominates |
| Process or workshop layout | High mix, low volume | Moderate investment, familiar equipment grouping | Long travel paths and high work in progress between operations |
| Cellular layout | Medium mix and medium volume, with a definable product family | Moderate investment, compact | Requires the parts to be grouped into families, which is a design and planning task |
| Flow line or conveyor | High volume, low mix | Higher investment, efficient use of space | Inflexible; a variant change is expensive |
| Mixed-model line | High volume with several variants | Highest planning effort | Needs balanced work content across variants, or imbalance reappears with each mix change |
| U-shaped cell | Medium volume with variable staffing | Compact, flexible operator count | Requires multi-skilled operators |
Two decisions should be made before the layout is chosen, because both are expensive to reverse. The first is whether the product family can be defined well enough for a cell, which depends on the design more than on the assembly method. The second is how much mix the line has to absorb, because a layout optimised for one variant degrades quickly as variants are added.
For the arithmetic behind several of these decisions, line balancing covers how work content is distributed across stations, and assembly line efficiency covers where time is actually lost once the line is running.
What to Send for an Assembly Quote
The technical reply is only as useful as the inputs. These are the items that change the answer.
- Controlled BOM, with ownership marked for every component
- Assembly drawing or 3D model, with datums and functional dimensions identified
- Torque values, orientation notes and any thread-locking or sealing requirement
- Functional and cosmetic acceptance criteria, including what counts as a rejectable mark
- Component list for buyer-supplied items, with delivery timing into the build
- Accessory kit contents, labels and the packing arrangement
- Batch size and how many variants share the same sequence
- Any maintenance or service-access requirement the end user has asked for
If the drawing is not final, send what exists. The review is more useful before the design is frozen than after, because the datums, the tolerance stack and the installation order are all decided on paper and are all expensive to change once parts have been cut.
Go deeper
Related Assembly and Fabrication Guides
Also useful: torque control, fastener selection, error-proofing (poka-yoke), assembly tolerance management, modular design, verification and testing and enclosure assembly service.
Buyer questions
FAQ on Sheet Metal Assembly
Short answers to the questions that come up most often. Final values and acceptance criteria are always confirmed against the project drawing and purchase requirements.
What files are needed for a metal product assembly quote?
An assembly model or drawing, a controlled BOM with component ownership marked, torque and orientation notes, the functional checks the unit has to pass, and the packaging configuration. If any of those are still open, send what exists and say which parts are provisional.
Can buyer-supplied components be installed?
Yes, subject to a review of incoming inspection, quantities, delivery timing into the build, handling and storage, and who carries responsibility for defective or short items. The important thing is that it is written down, because the answer changes who absorbs the delay when a component arrives late.
How is repeat assembly consistency controlled?
Four things together: an approved work sequence, fixtures where the geometry repeats, BOM revision control, and in-process gates at defined points. Any one of them alone is not enough — a good sequence with an uncontrolled BOM still produces the wrong unit.
What is the difference between sheet metal assembly and fabrication?
Fabrication turns sheet into parts: cutting, forming, welding and coating. Assembly joins those parts and the bought-in hardware into a finished unit. They are usually quoted together, but the risks are different, which is why the sequence and the gates are decided separately from the fabrication route.
How do you make sure the torque specification is actually followed?
By making it a gate rather than an instruction. The specified values are written into the work sequence, the tools are set to them, and the hardware is audited at the end of the step. That audit is what turns a torque value on a drawing into something that is true of the delivered unit.
Can the assembly be built to our sequence rather than yours?
Yes, and on repeat production it is usually the better arrangement, because your sequence is the one your service and warranty process is written around. Send it and we will review it for access, tooling and gate placement before confirming.
From research to RFQ
Send the Assembly Drawing for Review
Send the current files, quantity, material, finish and assembly context. We will come back with the questions needed for a practical manufacturing review — and, where the design allows it, with the options that reduce assembly time.
What stands behind this quotation
- Manufacturing since 20162,500 m² Ningbo plant — 3 laser cutting machines (including newer TRUMPF), 4 CNC press brakes and 10 welding stations.
- Shipped to more than 30 export marketsEnclosures, cabinets and formed parts supplied to OEM buyers across Europe, North America and Asia.
- 123 documented product casesMedical device housings, HVAC and heat pump enclosures, agricultural and livestock equipment, industrial hydraulics, material handling trolleys and EV charging cabinets.
- Factory evidence you can checkTUV Rheinland audit reference MIC-ASI243729 and Bureau Veritas reference MIC-ASR263630 available for buyer review on request.
Before you send drawings: project confidentiality is default · first-article inspection is carried out before a batch continues · pricing is staged from prototype quantity to repeat volume · pre-shipment photos and packing records are prepared when the project needs them.