
Surface finishing knowledge
Surface Preparation for Plating and Coating
Surface preparation for plating or coating removes or controls oil, oxide, weld residue, scale and edge conditions so the selected finish can contact a suitable substrate. The required preparation depends on metal, finish process and service environment.
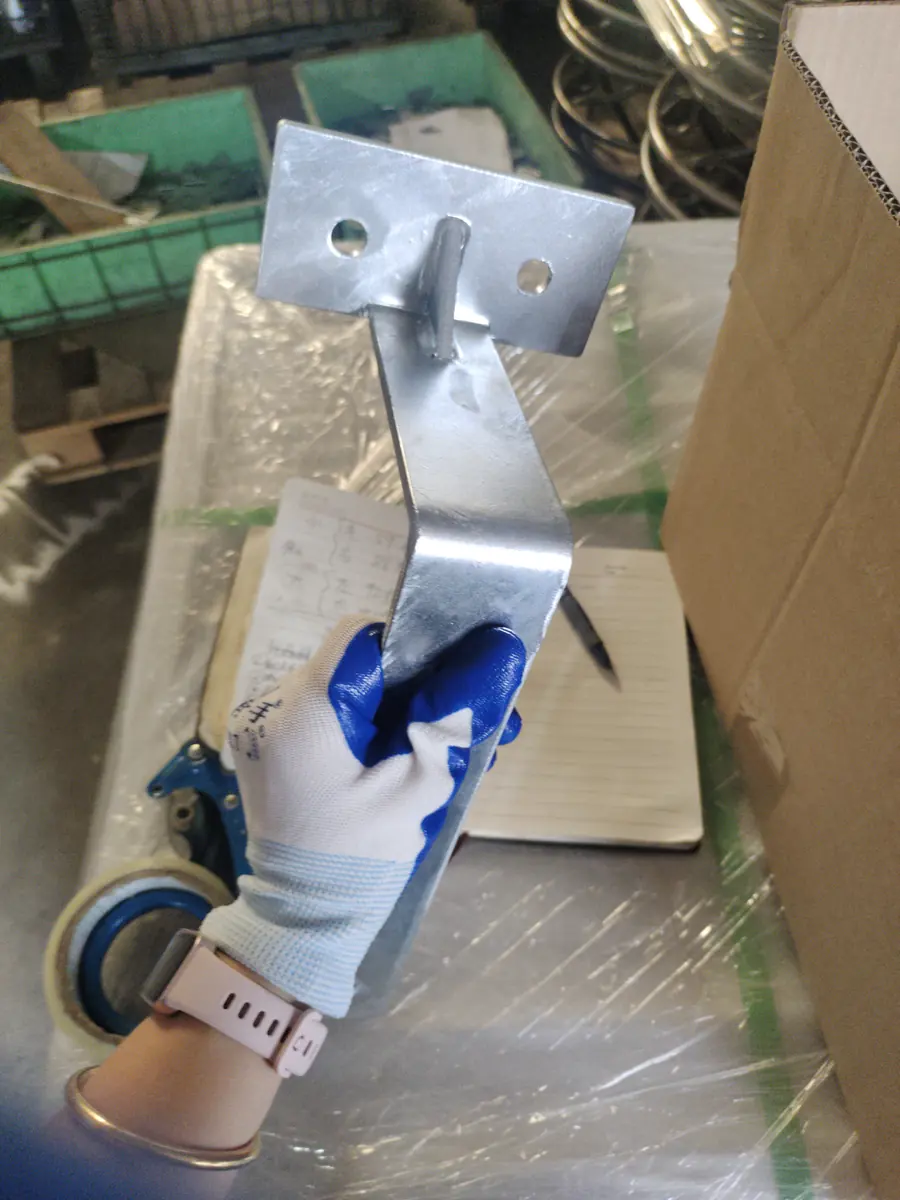
Buyer summary
Surface Preparation at a Glance: Inputs, Route and Inspection Basis
| Input condition | Base metal, mill finish, welds, grinding and contamination |
|---|---|
| Finish route | Specified coating or plating process and responsible supplier |
| Protected areas | Threads, grounding points, mating faces and cosmetic references |
| Inspection basis | Appearance, adhesion or other project-agreed evidence |
Preparation Begins Before the Finishing Supplier
Laser dross, sharp edges, weld spatter and heavy grinding marks are fabrication conditions. If they are not controlled before pretreatment, the final finish can reveal or magnify them.
The drawing should separate cosmetic faces from hidden structure and identify whether edge coverage or weld smoothing is functionally important.
Cleaning and Pretreatment Must Match the Substrate
Steel, galvanized sheet, stainless steel and aluminum do not use one universal preparation route. Chemical compatibility, storage time and the selected coating system must be reviewed by the responsible process supplier.
Fulei Metal coordinates finish requirements as part of the project, and some surface treatments may be completed by outside partners. The quotation should identify the responsible scope and documents.
Masking and Handling Protect Functional Interfaces
Threads, press-fit holes, grounding points, gasket surfaces and tight mating areas may need masks or drawing allowance. Handling after preparation is also important because fingerprints, moisture or dirty racks can reintroduce contamination.
The first article should be assessed after the complete finish and assembly sequence, not only immediately after coating.
What Each Pretreatment Stage Actually Removes
A pretreatment line is a sequence, and each stage has one job. Shortening or skipping a stage does not make the line faster in any useful sense — it moves the cost from the tank to the inspection bench. Degreasing removes drawing lubricants, forming oils and handling residue. Rinse then removes the degreasing chemistry, which matters more than it sounds: cleaner carried into the next tank contaminates it and shortens its life.
On steel, abrasive blast or chemical treatment removes mill scale and rust. On aluminium, an alkaline etch and deoxidiser remove the oxide film and the die lines left by rolling or extrusion. A conversion coating or phosphate stage then grows the crystalline film that gives the coating something to key into and adds a corrosion-inhibiting reserve. A final rinse in clean water, ideally deionised, stops dissolved salts being baked under the film. The order is not interchangeable: a conversion film grown on an oily surface looks correct and performs badly. See powder coating and surface finishing.
How Preparation Is Checked Before the Part Is Coated
Preparation is verified, not assumed, and four checks cover most of what goes wrong. The water-break test is the quickest: if a clean water film stays continuous across the surface for the specified time, the surface is free of the oils that cause fish-eyes and craters. Cleanliness of blasted steel is graded visually against ISO 8501-1 reference photographs, and the anchor pattern is compared against ISO 8503 comparators or measured with a roughness gauge. Conversion coating weight is checked on a coupon or by coating-weight measurement rather than by appearance alone.
The interval between treatment and coating is also controlled, because a prepared surface left in a humid workshop starts degrading before anyone notices. It is worth asking which of these are recorded against your batch: a preparation record tied to a batch number is what turns a later adhesion failure into something diagnosable instead of arguable. Related: quality inspection service, certification and traceability and powder coating standards.
Buyer questions
Surface Preparation Questions Buyers Ask Before Release
These answers define the discussion points. Final values and acceptance criteria are confirmed against the project drawing and purchase requirements.
Why does coating fail even when the powder is correct?
Oil, oxide, weld residue, sharp edges, poor pretreatment, moisture or handling contamination can undermine adhesion and appearance before powder is applied.
Which areas normally require masking?
Threads, grounding points, gasket interfaces, bearing or press-fit areas and dimensionally tight mating surfaces are common candidates, but the drawing must define them.
Is surface preparation the same for steel and aluminum?
No. Substrate chemistry, oxide condition and the selected finish require different preparation routes confirmed with the responsible finishing process.
RFQ checklist
What to Send With a Surface Preparation RFQ
- Define substrate and finish specification
- Mark cosmetic faces and edge expectations
- Identify weld dressing and deburring scope
- Show masks, grounding points and tight interfaces
- Agree finish evidence and handling protection
Substrate Condition Determines Which Preparation Is Non-Negotiable
Preparation is the step that decides whether a coating adheres, and it is the step most often reduced when a schedule tightens. Matching the preparation to the substrate condition is the cheapest insurance available.
| Substrate condition | Required preparation | Standard or check | What happens if it is skipped |
|---|---|---|---|
| Mill scale and rust on steel | Abrasive blast cleaning, typically to Sa 2.5 for demanding duty; power tool cleaning to St 2 or St 3 where blasting is not possible | ISO 8501-1 for the visual grade, ISO 8503 for the surface profile | Coating bridges the scale and detaches with it later |
| Oil, grease and forming lubricants | Alkaline or solvent cleaning followed by rinsing | Water-break test: an unbroken water film indicates a clean surface | Fish-eyes, craters and adhesion loss |
| Aluminium with oxide and extrusion die lines | Degrease, alkaline etch and deoxidise, then a conversion or chrome-free pre-treatment | Water-break test plus coating weight check | Powder detaches in sheets |
| Galvanized surface to be coated | Sweep blasting or chemical etching, plus cleaning | Profile and cleanliness check before coating | Poor adhesion on an apparently sound surface |
| Weld zones on stainless | Remove heat tint and scale by pickling or mechanical means, then passivate | ASTM A380 for cleaning and descaling, ASTM A967 for passivation | Rust staining at the weld despite a stainless substrate |
| Sharp edges and burrs | Round or deburr before coating | Visual and tactile check | Coating pulls back from the edge, and the edge rusts first |
The water-break test deserves more use than it gets. It takes seconds, needs no instrument, and it catches the single most common cause of coating failure: a surface that looks clean but still carries a thin oil film. Where a part has been through forming, machining or handling, that film is the usual explanation for adhesion failures that no amount of coating change will fix.
From research to RFQ
Send the Substrate and Finish Specification for Review
Send the current files, quantity, material, finish and assembly context. We will identify the questions needed for a practical manufacturing review.
What stands behind this quotation
- Manufacturing since 20162,500 m² Ningbo plant — 3 laser cutting machines (including newer TRUMPF), 4 CNC press brakes and 10 welding stations.
- Shipped to more than 30 export marketsEnclosures, cabinets and formed parts supplied to OEM buyers across Europe, North America and Asia.
- 123 documented product casesMedical device housings, HVAC and heat pump enclosures, agricultural and livestock equipment, industrial hydraulics, material handling trolleys and EV charging cabinets.
- Factory evidence you can checkTUV Rheinland audit reference MIC-ASI243729 and Bureau Veritas reference MIC-ASR263630 available for buyer review on request.
Before you send drawings: project confidentiality is default · first-article inspection is carried out before a batch continues · pricing is staged from prototype quantity to repeat volume · pre-shipment photos and packing records are prepared when the project needs them.