
Thin-gauge welding knowledge
Welding Thin Sheet Metal Without Distortion
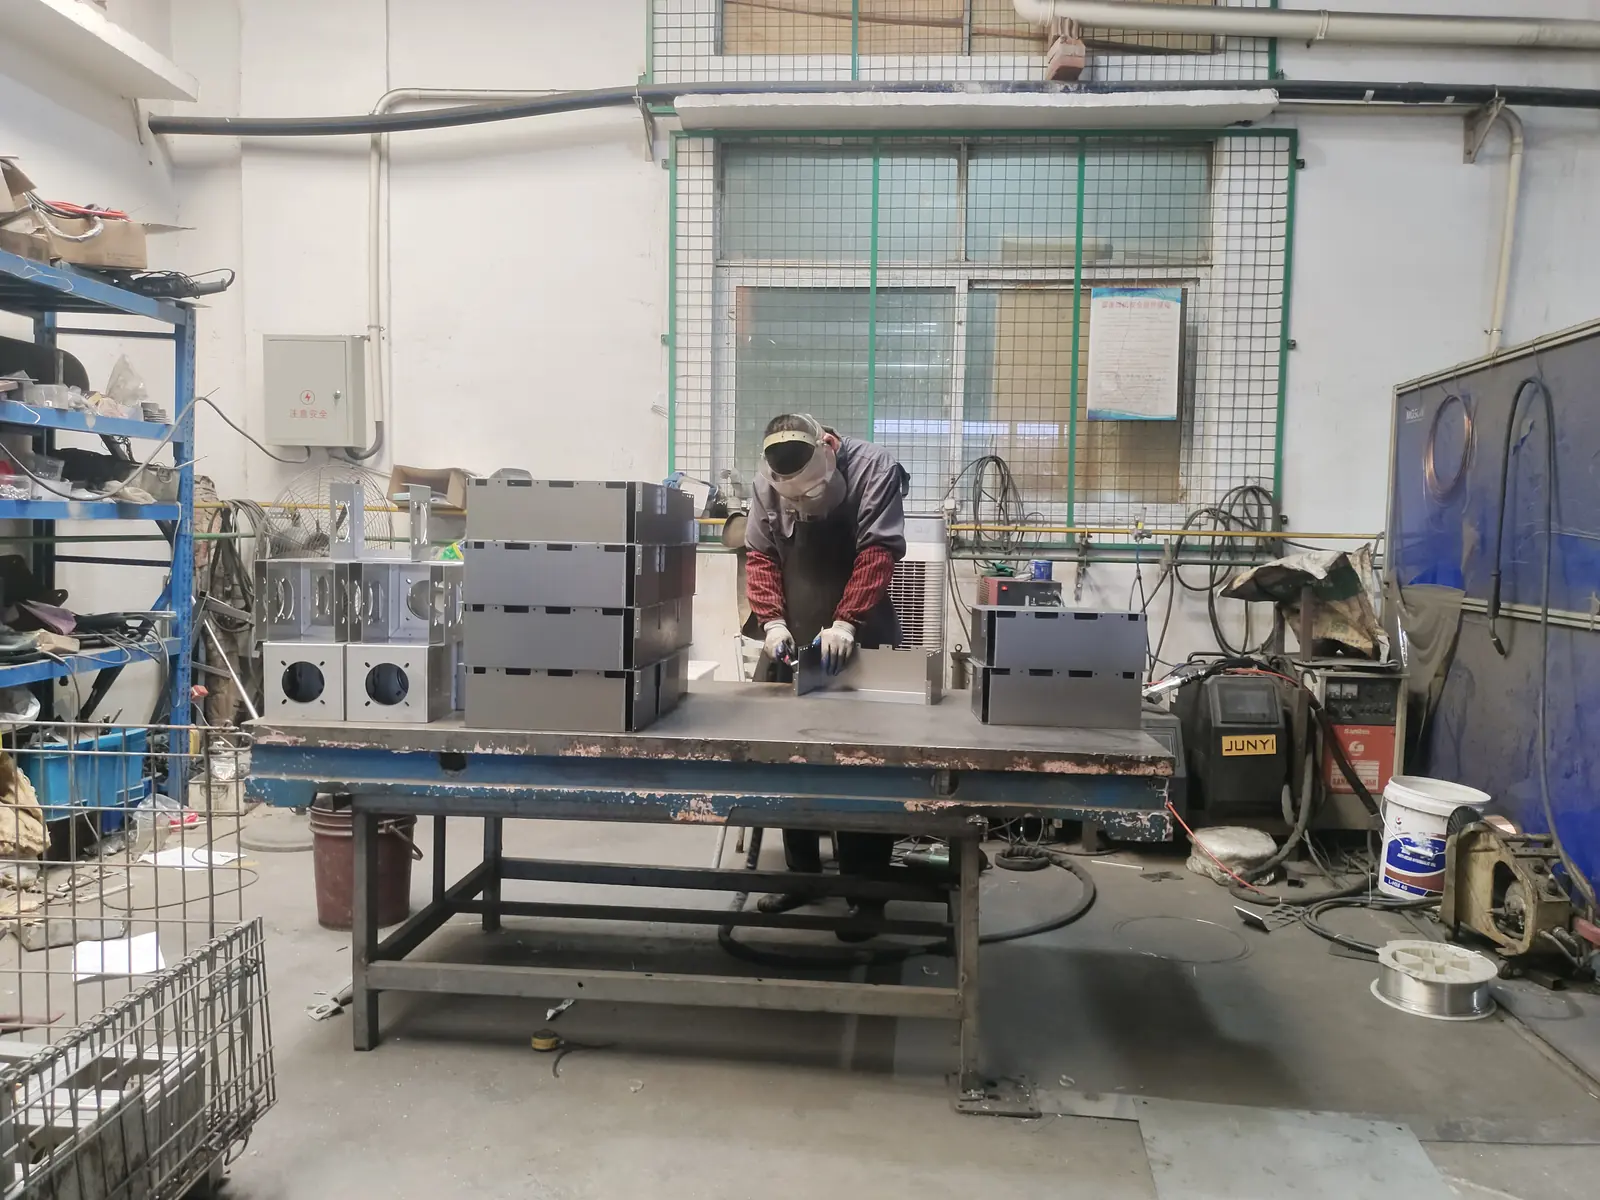
Thin sheet metal can be welded successfully when fit-up, joint design, tack pattern, fixture contact, heat input and sequence are treated as one system. The most common mistake is trying to correct poor fit-up with a longer or hotter weld.
Buyer summary
Thin-Sheet Welding at a Glance: Risks, Levers and Checks
| Typical products | Enclosure doors, covers, panels, trays and light assemblies |
|---|---|
| Primary risks | Burn-through, waviness, angular distortion and visible grind marks |
| Design levers | Joint type, formed stiffness, weld length and access |
| Verification | First-piece fit, flatness, squareness and cosmetic finish |
Design the Joint to Need Less Correction
A lap, corner or tabbed joint may locate thin panels more consistently than an open butt joint. Formed returns and ribs can add stiffness before welding. The best choice depends on the service function and visible surfaces.
Cutting and bending accuracy matter because small gaps change how the arc behaves. The assembly should reach the welding station with repeatable contact and a clear datum, not depend on the welder to manually rebuild the geometry.
Control Heat by Sequence, Not Only Machine Settings
Short welds, spaced tacks, alternating sides and allowing heat to distribute can reduce concentrated shrinkage. A fixture should support the functional shape without hiding the joint or forcing the part into an artificial geometry that springs back after release.
Machine parameters are material- and joint-specific. The useful buyer decision is to define the required strength, sealing and appearance so the factory can select and validate a practical process.
Approve the Product After the Required Finish
A panel may look flat before grinding and coating but show waves after cosmetic dressing or reflection from a smooth finish. The first article should therefore be reviewed in the condition that matters to the buyer.
Critical door gaps, mounting faces and connector openings should be measured after the relevant welding and finishing steps. That makes the batch acceptance plan match the delivered product.
Why Thin Sheet Distorts: What Happens Inside the Metal
Distortion is not a mystery, and it is not caused by a wrong machine setting alone. It comes from the weld metal and the heat-affected zone trying to expand while the surrounding cold sheet holds them back. During heating the joint is compressed plastically — it is effectively upset. On cooling it tries to shrink back, but it cannot return to its original length, so it drags the surrounding sheet with it.
On thick plate that shows up as angular distortion. On sheet below roughly 1.5 mm the panel does not have the stiffness to resist, so instead of bending it buckles: the waviness that appears between stiffeners is a stability failure, not a bending failure. That difference explains why turning the current down only partly works. Total heat input matters, but so does how long the heat stays in the part and how much stiffness the formed shape provides. A flange, a bead or a returned edge often does more for flatness than any change to the welding parameters — more in how to reduce welding distortion.
Measuring Distortion Instead of Describing It
"Looks a bit wavy" is not an acceptance criterion, and it is not something two parties can agree on at goods-in. Flatness should be measured against defined datums — the mounting face, the door opening, the specified set of holes — with the part supported the way it will be supported in service. A feeler gauge on a surface plate answers most questions about a panel; a dial indicator answers questions about a machined or machined-adjacent feature. Door gaps and mating dimensions belong to the assembled product rather than to the individual panel, which is why first-piece checks are done built up instead of laid out flat.
One sequencing point catches people out: acceptance belongs after the final finish, not before. Grinding, blasting and coating all move a thin panel. A part that measured flat in the weld shop can fail after powder coating, and finding that out at goods-in costs far more than finding it on the first article. Related: sheet metal quality inspection and material certification and traceability.
Buyer questions
Thin-Sheet Welding Questions Buyers Ask Before Release
These answers define the discussion points. Final values and acceptance criteria are confirmed against the project drawing and purchase requirements.
How do you reduce burn-through on thin sheet?
Stable fit-up, practical joint geometry, controlled heat input and an appropriate tack and weld sequence are reviewed together.
Why can a flat panel distort after welding?
Localized heating and uneven shrinkage pull the panel away from its original geometry. Long unsupported seams and excessive dressing can increase the risk.
Should cosmetic welds be ground completely flat?
Only when the drawing and approved sample require it. Excessive grinding can thin the material, change contours and add visible variation after coating.
RFQ checklist
What to Send With a Thin-Sheet Welding RFQ
- Define material and exact gauge
- Mark visible faces and acceptable weld appearance
- State sealed or structural joint requirements
- Identify critical post-weld geometry
- Approve a finished first article before repeat production
Process Settings and Fixturing by Sheet Thickness
On thin sheet the failure modes are burn-through at the start of the run and distortion after it. Both are controlled more by fixturing and settings discipline than by welder skill.
| Sheet thickness | Dominant risk | Setting that helps | Fixturing that helps |
|---|---|---|---|
| Up to 0.8 mm | Burn-through and melted edges | Pulsed MIG or pulsed TIG at low average current, high travel speed | Copper backing bar acting as a heat sink, and skip welding |
| 1.0-1.5 mm | Burn-through at starts, and panel waviness | Pulsed transfer, short arc length, controlled starts | Tacks at 150-300 mm spacing plus clamps close to the seam |
| 2.0-3.0 mm | Angular distortion on long seams | Moderate heat input, balanced or double-sided where accessible | Clamping along both sides of the seam, with a preset where the joint allows it |
| 3.0-6.0 mm | Undercut and lack of fusion at the root | Sufficient heat for the root, controlled weave width | Rigid fixturing; restraint is safe at this thickness on mild steel |
Heat input targets differ by an order of magnitude between these bands. Thin sheet work sits in roughly the 0.1-0.4 kJ/mm range, while sections above 3 mm tolerate 0.5-1.5 kJ/mm. Crossing that boundary is what turns a flat panel into a buckled one. Where a long seam runs down a thin panel, intermittent welding at a defined pitch often halves the total heat input for a modest reduction in joint strength, which is the more economical trade in most enclosure and cabinet work.
From research to RFQ
Send the Thin-Wall Assembly for a Weld Review
Send the current files, quantity, material, finish and assembly context. We will identify the questions needed for a practical manufacturing review.
What stands behind this quotation
- Manufacturing since 20162,500 m² Ningbo plant — 3 laser cutting machines (including newer TRUMPF), 4 CNC press brakes and 10 welding stations.
- Shipped to more than 30 export marketsEnclosures, cabinets and formed parts supplied to OEM buyers across Europe, North America and Asia.
- 123 documented product casesMedical device housings, HVAC and heat pump enclosures, agricultural and livestock equipment, industrial hydraulics, material handling trolleys and EV charging cabinets.
- Factory evidence you can checkTUV Rheinland audit reference MIC-ASI243729 and Bureau Veritas reference MIC-ASR263630 available for buyer review on request.
Before you send drawings: project confidentiality is default · first-article inspection is carried out before a batch continues · pricing is staged from prototype quantity to repeat volume · pre-shipment photos and packing records are prepared when the project needs them.