
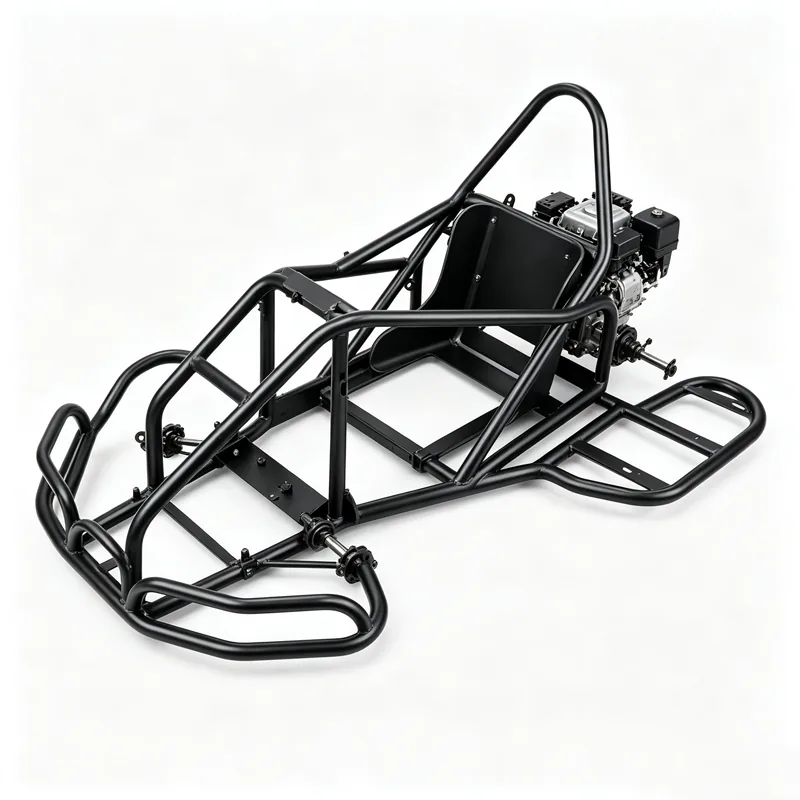

Tractor Enclosure
SKU: FL-AK-004
Tractor cab and fender enclosure. Heavy-gauge steel, powder coated.
| Material | SPCC steel (1.5-2.0mm) |
|---|---|
| Manufacturing Process | Laser cutting + bending + welding + powder coating |
| Surface Finish | Powder coating (custom colors) |
| Tolerance | ±0.5mm |
| Dimensions | Custom per model |
| Sound reduction | Yes |
| AC ready | Yes |
| Glass | Tempered (not included) |
| MOQ | 10 units |
| Lead Time | Quoted after drawing review and process confirmation |
| Sample Time | Not applicable |
| Sample Fee | N/A |
| Price Range | USD 1200-3500/unit |
| Applications | Tractors, agricultural machinery |
| Compliance | OECD Code 6 |
| Export Markets | USA, Germany, Brazil, India |
Modern tractors require enclosure components that protect operators from weather, house controls and equipment, and provide comfortable working environments. These components must withstand outdoor agricultural conditions including UV exposure, chemical contact, and vibration.
Tractor Enclosure Component Types
Cab frame components provide structural support for operator cabs. Fender components cover rear wheels and provide step access. Hood components cover engine compartments. Fuel tank housings protect fuel tanks. Battery box housings protect batteries. Tool box housings provide on-board tool storage. Instrument panel housings house operator controls and displays.
Material Selection for Tractor Cab Panels
Powder-coated steel provides cost-effective enclosure components with good durability and color options. We use 1.5 to 3.0 mm sheet. For premium components, stainless steel (grade 304) provides superior corrosion resistance against agricultural chemicals and weather. Aluminum provides weight reduction for non-structural components. All materials must withstand UV exposure, chemical contact, and vibration. Powder coatings must be UV-resistant and chemical-resistant.
Design Considerations for Cab Panels
Enclosure components must withstand vibration from tractor operation and rough terrain. All components must resist corrosion from agricultural chemicals, fertilizers, and weather. Edges must be smooth or reinforced for operator safety. Components must accommodate thermal expansion from engine heat and sun exposure. Designs must provide access for maintenance and service. Aesthetic design should complement tractor branding and styling. Components must meet agricultural equipment safety standards.
How Tractor Enclosures Are Fabricated
Our TRUMPF fiber laser cuts enclosure panels, frame components, and mounting brackets from flat sheet stock with precise cutouts for access, ventilation, and component interfaces. CNC press brake machines form panel profiles, fender shapes, and mounting flanges. Component assembly uses MIG welding for steel and TIG welding for stainless steel and aluminum. Surface treatments include UV-resistant and chemical-resistant powder coating, electropolishing, and anodizing.
Field Notes: Tractor Cab and Body Components
Tractor cab components are specified around visibility and noise as much as around strength. The cab structure has a glazed area that is unusually large for the size of the vehicle, which means the frame members are narrow and heavily loaded, and every one of them takes the load of the cab in a rollover rather than simply holding a window. That makes the fabrication of these parts a question of material grade and weld quality rather than of section size, and it is why cab frames are welded to a procedure and inspected rather than assembled and checked by eye. Beyond the structure, the components that come through this route are the mounting brackets, steps and panel fixings, and those are judged on whether they survive the vibration of a working tractor – which means captive fasteners and positive location rather than fasteners that can work loose.
A tractor enclosure — the cab skin and its supporting panels — has to do three unrelated jobs: keep operator noise down, survive vibration that never stops, and leave room for glass, HVAC and controls that other suppliers design. Being good at one of those does not help with the others.
Why Cab Panels Fail Differently From Other Sheet Metal
The panels on this page are formed from 1.5–2.0 mm SPCC and finished to the buyer’s colour, but thickness and finish are not what governs service life. A cab is mounted on a machine that vibrates continuously and flexes over rough ground, so a panel that is stiff in isolation will still crack if it is tied into two parts of the structure that move differently. The failure appears at the welds and at the fixing points first.
Noise reduction and air-conditioning readiness push in the same direction: both need sealed joints, defined gaps at the glass aperture and room for ducting. Those three requirements are why the glass aperture on a cab panel is dimensioned on the drawing rather than cut to suit on assembly — the glass is supplied and fitted to the vehicle, and the aperture has to be right before the panel is painted.
Decisions Worth Settling Before the First Panel Is Cut
- How the panel meets the structure — rigidly welded, or through isolation mounts. This is the single biggest driver of whether welds crack in service.
- Glass aperture tolerances — the opening is sized around the glass the vehicle builder specifies, and checked against a sample of that glass.
- Access for service — panels that have to come off for routine maintenance need captive fixings and a defined removal sequence, or they will be left off after the first service.
- Ducting and wiring pass-throughs — positions have to be agreed with whoever supplies the HVAC unit, before the panel is formed.
Where a cab has to satisfy an agricultural tractor safety standard such as OECD Code 6, that approval and its testing belong to the vehicle manufacturer or to the approved test station they nominate. Our scope is the enclosure as drawn: the panels, the joints, the apertures and the finish stated on the drawing.
How Cab Panels Are Made and Checked
Laser cutting, CNC bending, welding and powder coating. Distortion control is the recurring issue on large thin panels, so the weld sequence is fixed before production starts and the panels are checked on the fixture rather than free-standing. Apertures are verified with the glass or a representative template. Coating is inspected for coverage on edges and inside returns, which is where corrosion starts on a machine that lives outdoors.
Inspection follows the buyer drawing and the approved sample, with general tolerances to ISO 2768. Material and coating documentation is issued with the batch — traceability records are kept per order. Panels are packed face-to-face with separation so coated surfaces do not rub in transit; for export consignments see export packaging standards.
Do you supply the glass and the HVAC unit?
No. The glass aperture and the duct openings are produced to the dimensions given by whoever supplies those items. Send their interface drawings and the panel is built around them.
Can you make panels for an existing cab design?
Yes — send the panel drawings, or the panels themselves for reverse engineering. The aperture dimensions and the mounting points are what have to be exact.
Information Needed to Quote Tractor Enclosure
Panel geometry or samples, the interface drawings for glass and HVAC, material, colour, and quantity. Timing is quoted after drawing review and process confirmation.
Payment Terms
How a project is paid for is agreed before production starts, and the structure that applies to your order is stated on the quotation and on the order confirmation, so there is no ambiguity later.
- 30% advance payment with the order and the 70% balance before shipment — our standard structure.
- 70% advance payment with the order and the 30% balance before shipment — used for some projects.
- 100% payment in advance before production starts — used for some projects.
If your finance team works to a fixed structure, say so in the first enquiry and we will confirm what applies to your order before you commit. Request a quotation.
Questions buyers ask before sending drawings
The questions that come up most often before a project starts, answered the way we answer them by email.
What do you need from me to quote Tractor Enclosure?
2D drawings as PDF, DWG or DXF, or 3D files as STEP, IGES or SolidWorks, together with material grade, sheet thickness, surface finish, quantity and destination country. If the drawing is not finished yet, send a photo, a sketch or the existing part instead — we review what can be measured from it and reply with the questions that still need answering.
How long does a quotation take?
Enquiries are answered within one business day. Simple laser-cut and bent parts are quoted within 24 hours. Welded frames, assembled units and multi-part structures are quoted after the drawing review and process confirmation, and the date is confirmed in our reply.
Is there a minimum order quantity?
Prototypes are made from a single piece and small batches of 10–50 pieces are routine. Prototype, first batch and repeat volume are quoted together so the numbers stay consistent as the project scales.
Can you work from a sample or a photo if I have no drawing?
Yes. Send the part itself, clear photographs with a rule or caliper in frame, or a dimensioned sketch. We measure what can be measured, list what is still undefined, and confirm it with you before production.
Need a Similar Part?
Most enquiries that start on a page like this are not an order for Tractor Enclosure — they are a search for a factory that can make something like it. Send us your drawing, 3D model or sample and we will review the manufacturing process and the quotation requirements, then come back with a process plan, a price and a lead time.
We work from 2D drawings, STEP / DWG / DXF / PDF files, or a physical sample if that is all you have.
No complete drawings yet? Describe the part, send photos or a sketch, or send a sample — we can start from there. Discuss your project.
Trade Terms and Delivery
We quote under the standard Incoterms your logistics team already works with, and build the packing and documentation around the one you choose.
- EXW — you collect from our Ningbo facility and run export clearance through your own forwarder.
- FOB Ningbo — we deliver to the vessel at Ningbo port and handle export clearance.
- CIF — we cover carriage and insurance to your named destination port.
- DDP — we handle carriage, insurance, import clearance and duties through to your door.
Send your destination country, target delivery date and preferred trade term together with the drawing. Request a quotation.
Quotation Time
We quote from your drawings. How long that takes depends on what the part asks for:
- Simple parts — quoted within 24 hours. Laser-cut blanks and bent components, supplied with complete 2D or 3D drawings. Mon–Fri, GMT+8.
- Complex assemblies — quoted after the drawing review. Payment kiosks, multi-part welded frames, enclosures with purchased hardware, or anything needing a coating or assembly trial. We confirm a quotation date once the scope is clear.
Production lead time is quoted separately, after drawing review and process confirmation. Send your drawings.
What stands behind this quotation
- Manufacturing since 20162,500 m² Ningbo plant — 3 laser cutting machines (including newer TRUMPF), 4 CNC press brakes and 10 welding stations.
- Shipped to more than 30 export marketsEnclosures, cabinets and formed parts supplied to OEM buyers across Europe, North America and Asia.
- 123 documented product casesMedical device housings, HVAC and heat pump enclosures, agricultural and livestock equipment, industrial hydraulics, material handling trolleys and EV charging cabinets.
- Factory evidence you can checkTUV Rheinland audit reference MIC-ASI243729 and Bureau Veritas reference MIC-ASR263630 available for buyer review under NDA.
Before you send drawings: an NDA is signed on request · first-article inspection is carried out before a batch continues · pricing is staged from prototype quantity to repeat volume · pre-shipment photos and packing records are prepared when the project needs them.