
Master First Article Inspection for sheet metal parts. Learn about FAI requirements, planning, documentation, and best practices for new product validation.
The Problem First Article Inspection (FAI) Solves
First Article Inspection (FAI) is a comprehensive verification of the first part produced from a new or modified design. It confirms that the manufacturing process can produce parts that meet all requirements. At Fulei Metal, we perform FAI for every new product to ensure quality from the start.
What is First Article Inspection?
How First Article Inspection (FAI) Is Defined
FAI is a complete inspection of the first part or parts produced using a new manufacturing process, new design, or modified process. It verifies that all dimensional, material, and functional requirements are met before production continues.
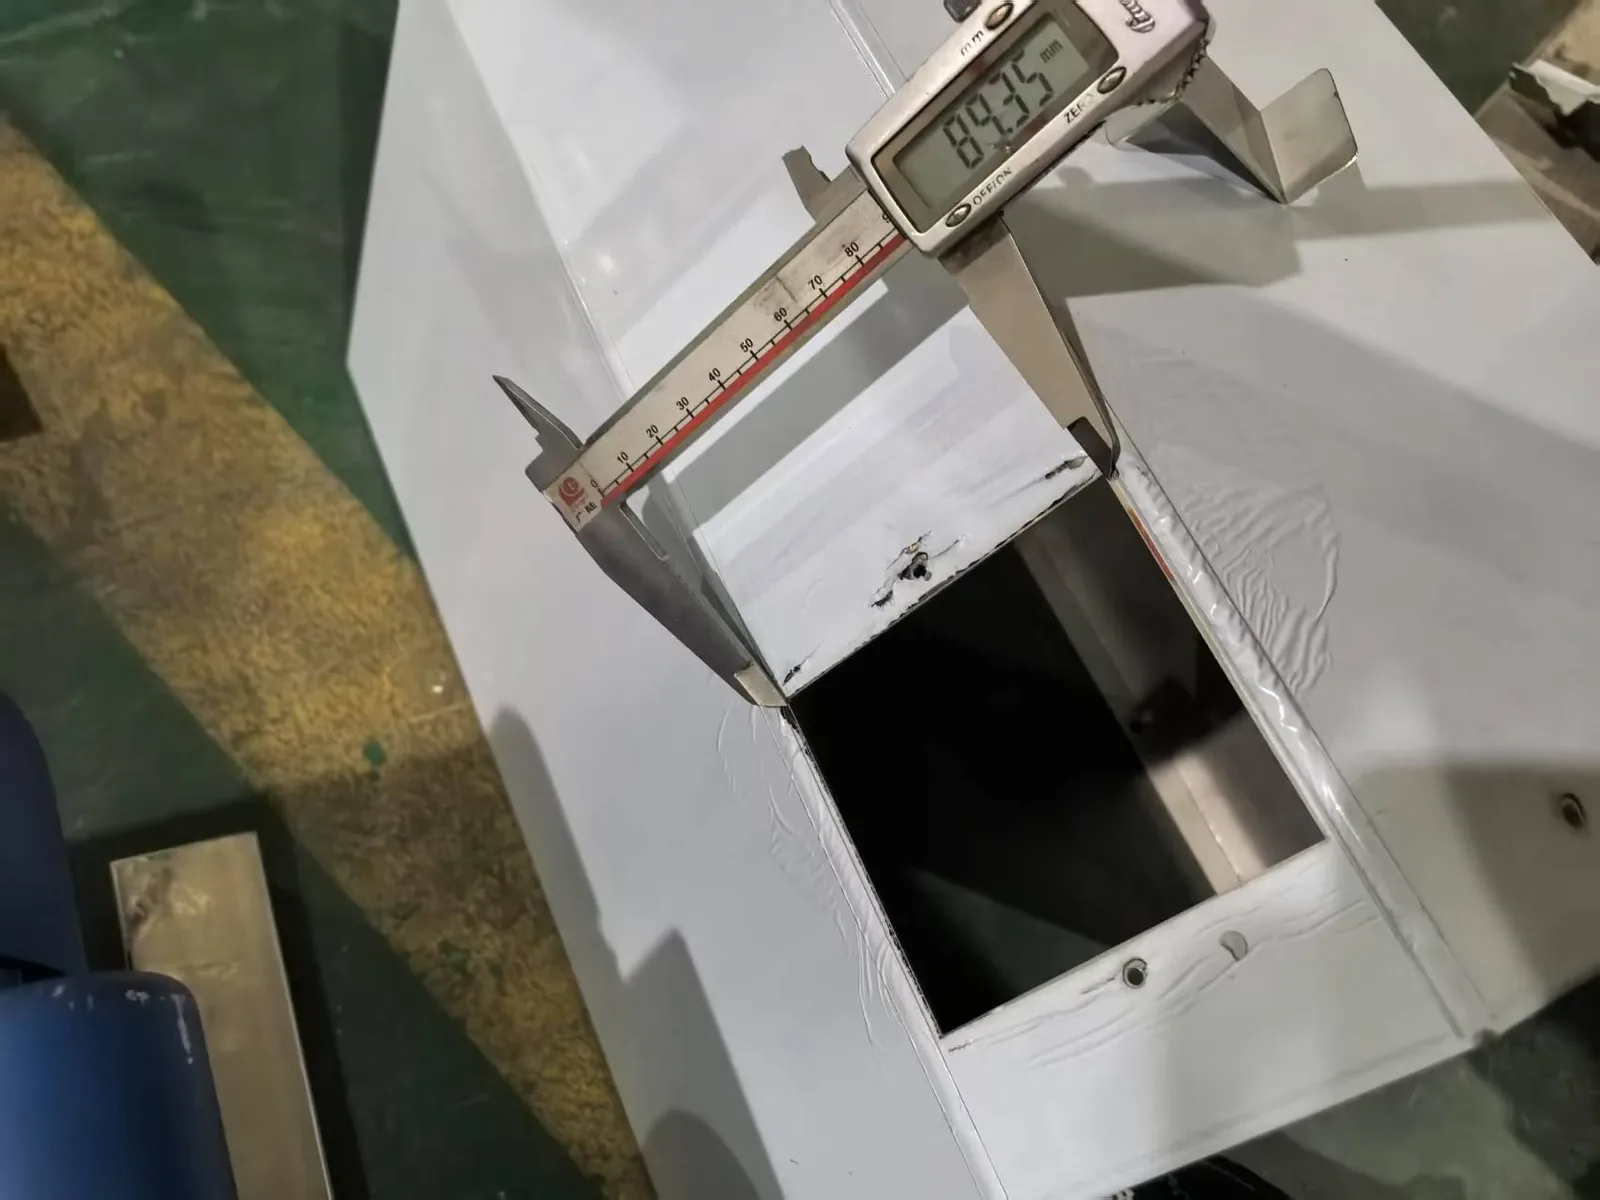
What First Article Inspection (FAI) Is For
Verify manufacturing process: confirm the process can produce conforming parts. Verify product design: confirm the design is manufacturable and meets requirements. Verify tooling and fixtures: confirm tooling produces correct parts. Establish baseline: create reference for future inspection. Customer approval: provide evidence for customer source approval. Prevent production of non-conforming parts: catch problems early.
When FAI is Required
New product: first production run. Design change: modification to part design. Process change: new manufacturing method or equipment. Tooling change: new or modified tooling. Material change: different material grade or supplier. Location change: production moved to different facility. After extended production break: resuming production after gap. Customer requirement: customer specifies FAI frequency.
FAI Planning
FAI Procedure
Document the FAI process. Define: what to inspect, how to inspect, acceptance criteria, documentation requirements, who performs inspection, who approves results.
Identification of Characteristics to Inspect
All dimensional characteristics: every dimension on the drawing. All geometric tolerances: flatness, perpendicularity, position, etc. All material requirements: grade, properties, certification. All surface finish requirements: roughness, coating, treatment. All functional requirements: performance tests if applicable. All marking and labeling requirements. All special requirements: customer-specific, regulatory.
Inspection Plan
Create detailed inspection plan. List each characteristic: feature description, nominal value, tolerance, measurement method, measurement tool, acceptance criteria. Sequence: plan measurement order for efficiency. Assign: inspector, equipment, estimated time.
Resource Preparation
Ensure: measurement equipment available and calibrated, inspection fixtures available, material certification available, drawing and specification current, FAI form or software ready, qualified inspector available.
FAI Process
Step 1: Produce First Article
Manufacture the first part using the production process. Use production tooling, equipment, and procedures. Document production parameters. Ensure process is set up correctly.
Step 2: Verify Material
Verify material certification matches specification. Verify material grade and properties. Verify heat number traceability. Record material certification reference.
Step 3: Dimensional Inspection
Inspect all dimensions on the drawing. Use appropriate measurement tools. Record: nominal, tolerance, measured value, result. Use CMM for complex geometries. Verify all geometric tolerances.
Step 4: Visual Inspection
Inspect surface finish, appearance, defects. Verify coating/paint if applicable. Check for burrs, sharp edges. Verify marking and labeling.
Step 5: Functional Testing
Perform functional tests if applicable. Verify mechanisms operate correctly. Verify assembly with mating parts if applicable. Perform any special tests specified.
Step 6: Documentation
Complete FAI report. Include all inspection results. Include material certification. Include any test reports. Include production records. Review for completeness.
Step 7: Review and Approval
Review FAI results. Verify all characteristics conform. Identify any non-conformances. If non-conformances found: investigate root cause, correct process, produce new first article, repeat FAI. If all conform: approve for production. Obtain customer approval if required.
Step 8: Production Release
Release for production after FAI approval. Maintain FAI records. Use FAI as baseline for production inspection. Schedule next FAI if required (after changes).
FAI Documentation
FAI Report Content
Part identification: part number, part name, revision. Drawing: number, revision, date. Material: grade, specification, heat number, certification reference. Production: work order, date, quantity. Manufacturing process: method, equipment, parameters. Inspection results: all dimensions and tests. Measurement equipment: tools used, calibration status. Inspector: name, signature, date. Quality approval: name, signature, date. Customer approval: if required.
Dimensional Results Table
For each dimension: feature description, dimension ID (balloon number), nominal value, upper tolerance, lower tolerance, measured value, result (pass/fail). Organized by drawing view or feature type. Complete coverage of all drawing dimensions.
Material and Process Results
Material grade and specification. Material certification reference (MTC number, heat number). Special processes: surface treatment, welding, heat treatment. Process parameters: relevant production parameters. Process certification: welder qualification, WPS reference.
Non-Conformance Documentation
If any characteristic does not conform: describe the non-conformance, record specification and actual value, investigate root cause, document corrective action, plan re-inspection after correction.
FAI Standards
AS9102 (Aerospace)
Standard FAI form for aerospace industry. Three forms: Part 1 (Part Number), Part 2 (Product Definition), Part 3 (Characteristics). Required for aerospace parts. Comprehensive and structured.
General Industry
No single standard for all industries. FAI format may be: customer-specified, company-specific, based on industry practice. Key: all requirements verified and documented.
Customer-Specific FAI
Customer may specify: FAI format, content, approval process, submission requirements. Follow customer requirements when specified.
FAI Best Practices
Planning
Plan FAI before production starts. Ensure all resources available. Create inspection plan. Review drawing for completeness. Identify critical characteristics.
How First Article Inspection (FAI) Is Measured
Use calibrated equipment. Use appropriate measurement methods. Verify gauge R&R if needed. Take multiple measurements for critical features. Use CMM for complex geometries. Document all measurements.
Objectivity
Inspect objectively. Do not adjust results to pass. If non-conformance found: report it. Investigate root cause. Correct the process. Re-inspect.
Documents That Come With First Article Inspection (FAI)
Document completely. Every dimension inspected. Every test performed. Every result recorded. Include all supporting documentation. Review for completeness before submission.
Communication
Communicate FAI results to all stakeholders. Engineering: design issues identified. Production: process issues identified. Quality: inspection results. Customer: FAI approval if required.
Common FAI Issues
Missing Dimensions
Problem: not all dimensions on drawing inspected. Cause: oversight, incomplete inspection plan. Prevention: use balloon method to identify all dimensions, create comprehensive inspection plan, review for completeness.
Inadequate Measurement
Problem: measurement tool not accurate enough. Cause: wrong tool selected, tool not calibrated. Prevention: select tool with adequate accuracy (10:1 rule), verify calibration, conduct gauge R&R.
Design Issues
Problem: design is not manufacturable as specified. Cause: design errors, unrealistic tolerances, missing specifications. Solution: work with engineering to resolve, modify design if needed, document deviations.
Process Issues
Problem: process cannot produce conforming part. Cause: inadequate process, wrong parameters, tooling issues. Solution: adjust process parameters, modify tooling, improve process.
Material Issues
Problem: material does not meet specification. Cause: wrong material supplied, material defect. Solution: verify material at receiving, obtain correct material, investigate with supplier.
Partial FAI
When Partial FAI is Appropriate
Design change affects only some characteristics. Process change affects only some operations. Only some characteristics need re-verification. Partial FAI covers affected characteristics only.
Partial FAI Requirements
Identify affected characteristics. Inspect affected characteristics. Reference previous FAI for unaffected characteristics. Document what changed and why partial FAI is appropriate. Obtain approval if required.
How Fulei Metal Builds First Article Inspection (FAI)
Our FAI program includes: documented FAI procedure. Comprehensive inspection of all characteristics. FAI report with complete documentation. Material certification verification. CMM inspection for complex parts. Customer FAI format support. FAI approval process. FAI records maintenance. We perform FAI for every new product, ensuring that our manufacturing processes produce conforming parts from the first article, providing confidence to our global clients.
Full FAI or Partial FAI: How the Scope Is Decided
A first article inspection is not one fixed document. Its scope follows the change that triggered it, and getting that wrong costs money in one of two ways: an inspection nobody uses, or a gap that only surfaces once the parts are in service.
The choice below is made before anything is measured, because it decides both the inspection workload and how much of the lot remains unexplained afterwards.
| What changed | Full FAI | Partial FAI | When the partial route actually holds up |
|---|---|---|---|
| A new part, with no inspection history | Every characteristic on the drawing, ballooned and numbered | Not available – there is nothing to compare against | Never. A first article with no baseline is a full first article by definition |
| A revision that changes one feature family | All characteristics, on the reasonable fear that something else moved | Only the characteristics the revision touches | When the earlier FAI is closed out, traceable, and was produced on the same process route |
| New tooling, new press, new fixture | All characteristics that the tooling or fixture can influence | Usually the affected characteristics plus a safety margin | Only if the change can be shown not to reach the untouched characteristics |
| A shift of one operation to a different machine | The characteristics that operation produces, at minimum | The operation output plus the interface dimensions downstream | When the downstream operations are unaffected and the interface is re-verified |
| A tooling repair or a re-ground punch | Rarely needed in full, but the affected geometry yes | The geometry the tool produces | When the repair restored the original geometry rather than changing it |
| The first run after a long gap in production | The characteristics the process is least stable on | The characteristics that drifted before, if records exist | When the previous runs records identify a stable set to re-check |
Partial FAI is not a discounted version of the same report. It is only defensible when a full FAI already exists, is closed out, and still describes the route the part is made on. If the route moved anywhere the report does not cover, the baseline is gone and the honest answer is a full inspection. Send the drawing with its revision history through the RFQ form and we will say which one applies before either of us spends time on it.
EMPB, ISIR and PPAP: The Same Idea Under Different Names
FAI describes what is done. The documents that ship it vary by programme, and the naming is where most confusion starts. ISIR (Initial Sample Inspection Report) is widely used across European and Asian OEM supply chains. EMPB is the German-language initial sample report format met most often on programmes run out of German-speaking engineering departments. PPAP (Production Part Approval Process) sits on the automotive side and reaches further into process evidence than either of the others.
They share one principle: measure the first parts from production tooling, record every result against the drawing characteristic it belongs to, and hand it over for approval before series parts ship. The differences that matter to scheduling are all about scope:
- Which characteristics are covered. Some programmes require every numbered characteristic on the drawing; others only those marked as critical. The first is several times the measuring work.
- Whether process data is attached. Capability figures, control plans and gauge information sit inside PPAP but usually not inside EMPB.
- What supporting certification travels with it. Mill certificates, coating records and calibration evidence referenced in our traceability notes.
- Whose form is used. We complete the customer form. We do not substitute our own sheet for it, because a buyer receiving an unfamiliar layout loses more time than the shortcut saves.
One thing worth agreeing early: if a requested form asks for data we cannot honestly produce – process capability over a run we have not made, or verification requiring equipment we do not hold – we say so at quotation rather than leaving a blank looking like an oversight. Witnessed or third-party inspection is arranged by whoever requires it; our contribution is the parts and the measured results.
What the Sample Quantity Does to the Quote
Sample cost confuses people because most of it is not material. Programming, setup, first-piece checks and any fixture work cost broadly the same whether one piece is made or five. What scales with quantity is the measuring and the paperwork.
Full coverage of every drawing characteristic across several pieces therefore does not mean the same inspection five times over at no extra thought. Each additional piece carries close to another full round at the bench, plus report compilation, and that labour is real. It is also why a request to report on every feature of every sample changes the quote noticeably while the parts themselves barely change.
We list first-article and documentation effort as separate lines rather than folding them into unit price, for one practical reason: those lines do not repeat in series production, so burying them keeps the volume price from ever coming down where it should. If you do not need full coverage on all pieces, saying so is one of the cheaper things you can specify – applying a defined sampling plan to the non-critical pieces usually gives everybody the evidence they need.
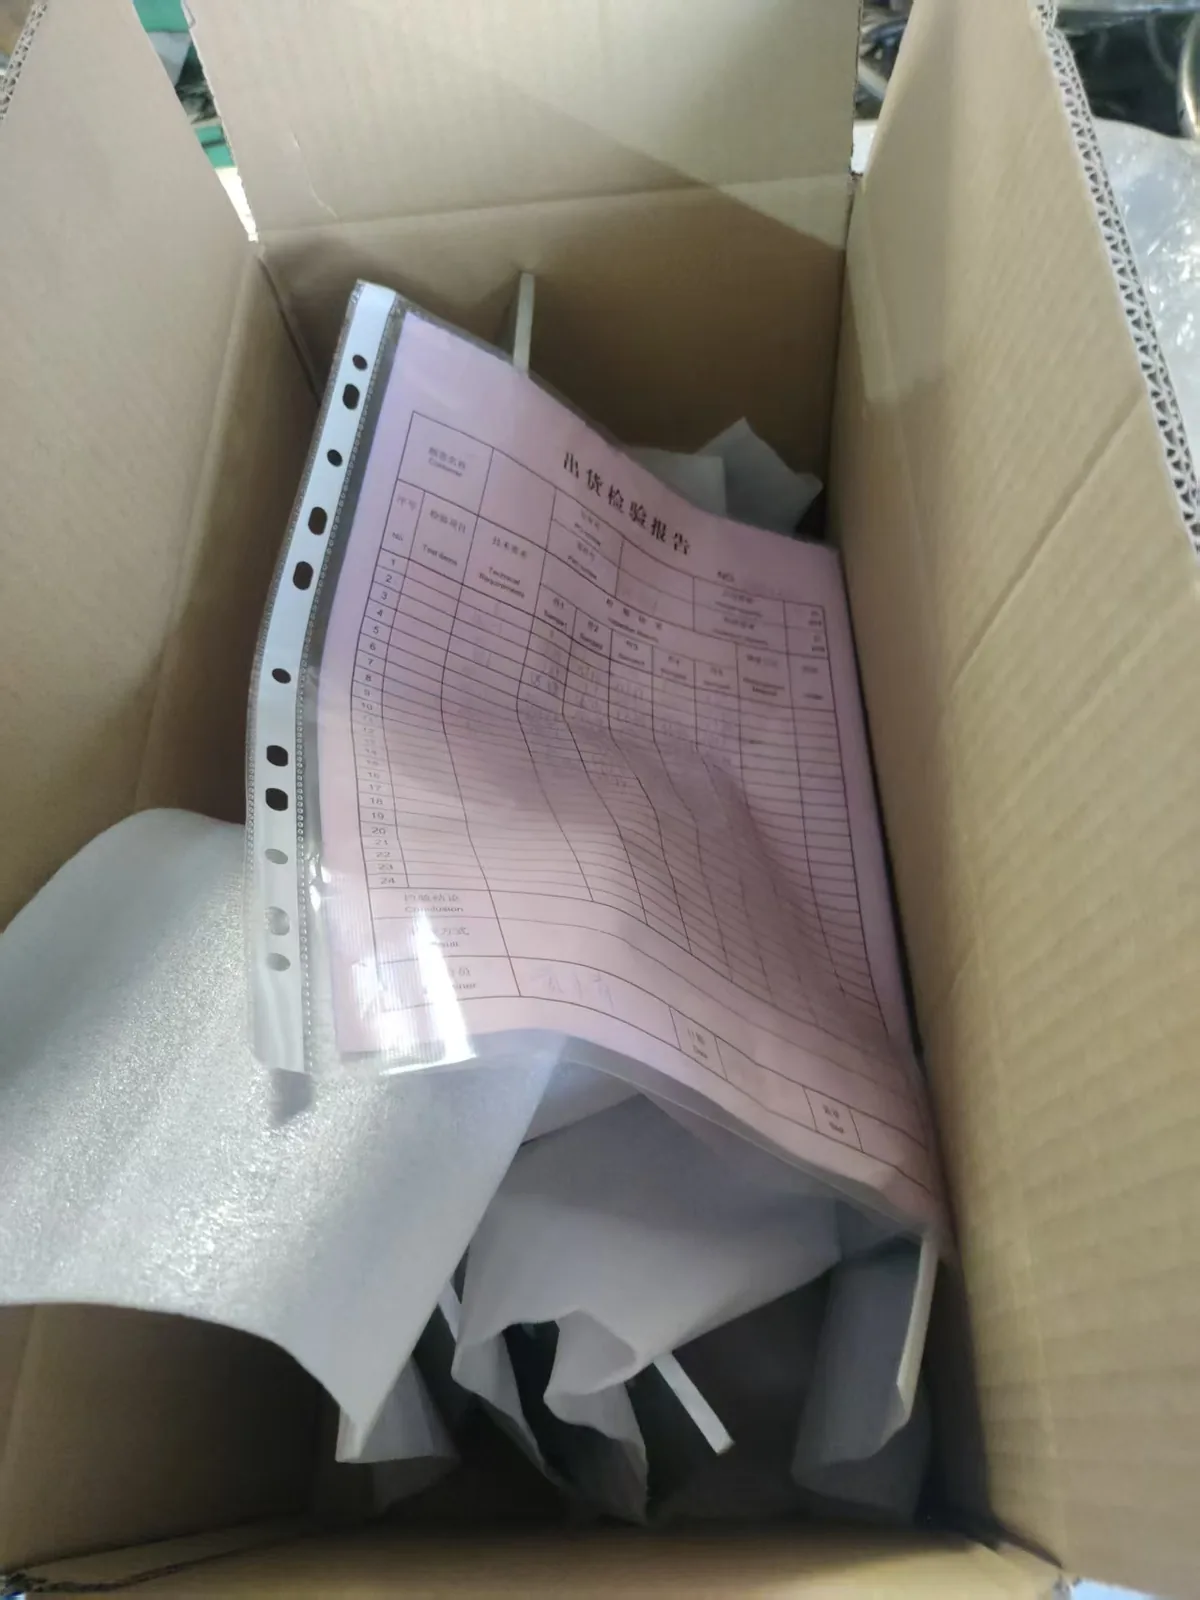
The measurements themselves are taken using the methods set out in our dimensional inspection guide, and the formats they are reported in are covered under inspection documentation. Both sit alongside this page rather than repeating it.
First Article Inspection (FAI): Common Buyer Questions
How long does a first article report stay valid?
There is no fixed expiry in the way a certificate has one. It is event-driven: the report describes the process route as it stood on the day it was signed, so it stays valid for as long as that route is unchanged. A new machine, a repaired tool, a change of material supplier or a revision all shorten it. This is also why we record the route on the report rather than only the results.
Who pays for the first article?
It is part of the set-up, so on a new part it is normally built into the price rather than invoiced separately, and on a repeat part it is not charged again unless the scope changes. What matters more than who pays is that the scope is agreed in writing first – an inspection plan written after the fact tends to describe what was measured rather than what mattered.
What happens if the first article fails?
It does not ship, and it is not shipped as “pending approval” either. The deviation is measured, the cause is traced to the process rather than the part, the process is corrected and a new first article is produced against the same plan. Shipping a failed first article on a promise is how a whole lot becomes suspect – once one part is known to be out of specification, every part made on that set-up carries the same question.
Questions about a specific part are usually faster to answer against the drawing — send it through the route below.
How We Quote First Article Inspection (FAI)
First Article Inspection is a critical step in validating new products and processes. At Fulei Metal, our thorough FAI process ensures that we can produce parts that meet all requirements before entering production, preventing quality issues and providing confidence to our international clients from the very first part.
If you are sourcing this type of part, our quality inspection service page covers the tolerances, batch sizes and inspection we work to, and custom sheet metal fabrication shows the wider range we produce in Ningbo, China. For background reading before you request a quote, see Outgoing Inspection.
Related at Fulei Metal: sheet metal quality inspection service · inspection report documentation
What stands behind this quotation
- Manufacturing since 20162,500 m² Ningbo plant — 3 laser cutting machines (including newer TRUMPF), 4 CNC press brakes and 10 welding stations.
- Shipped to more than 30 export marketsEnclosures, cabinets and formed parts supplied to OEM buyers across Europe, North America and Asia.
- 123 documented product casesMedical device housings, HVAC and heat pump enclosures, agricultural and livestock equipment, industrial hydraulics, material handling trolleys and EV charging cabinets.
- Factory evidence you can checkTUV Rheinland audit reference MIC-ASI243729 and Bureau Veritas reference MIC-ASR263630 available for buyer review on request.
Before you send drawings: project confidentiality is default · first-article inspection is carried out before a batch continues · pricing is staged from prototype quantity to repeat volume · pre-shipment photos and packing records are prepared when the project needs them.