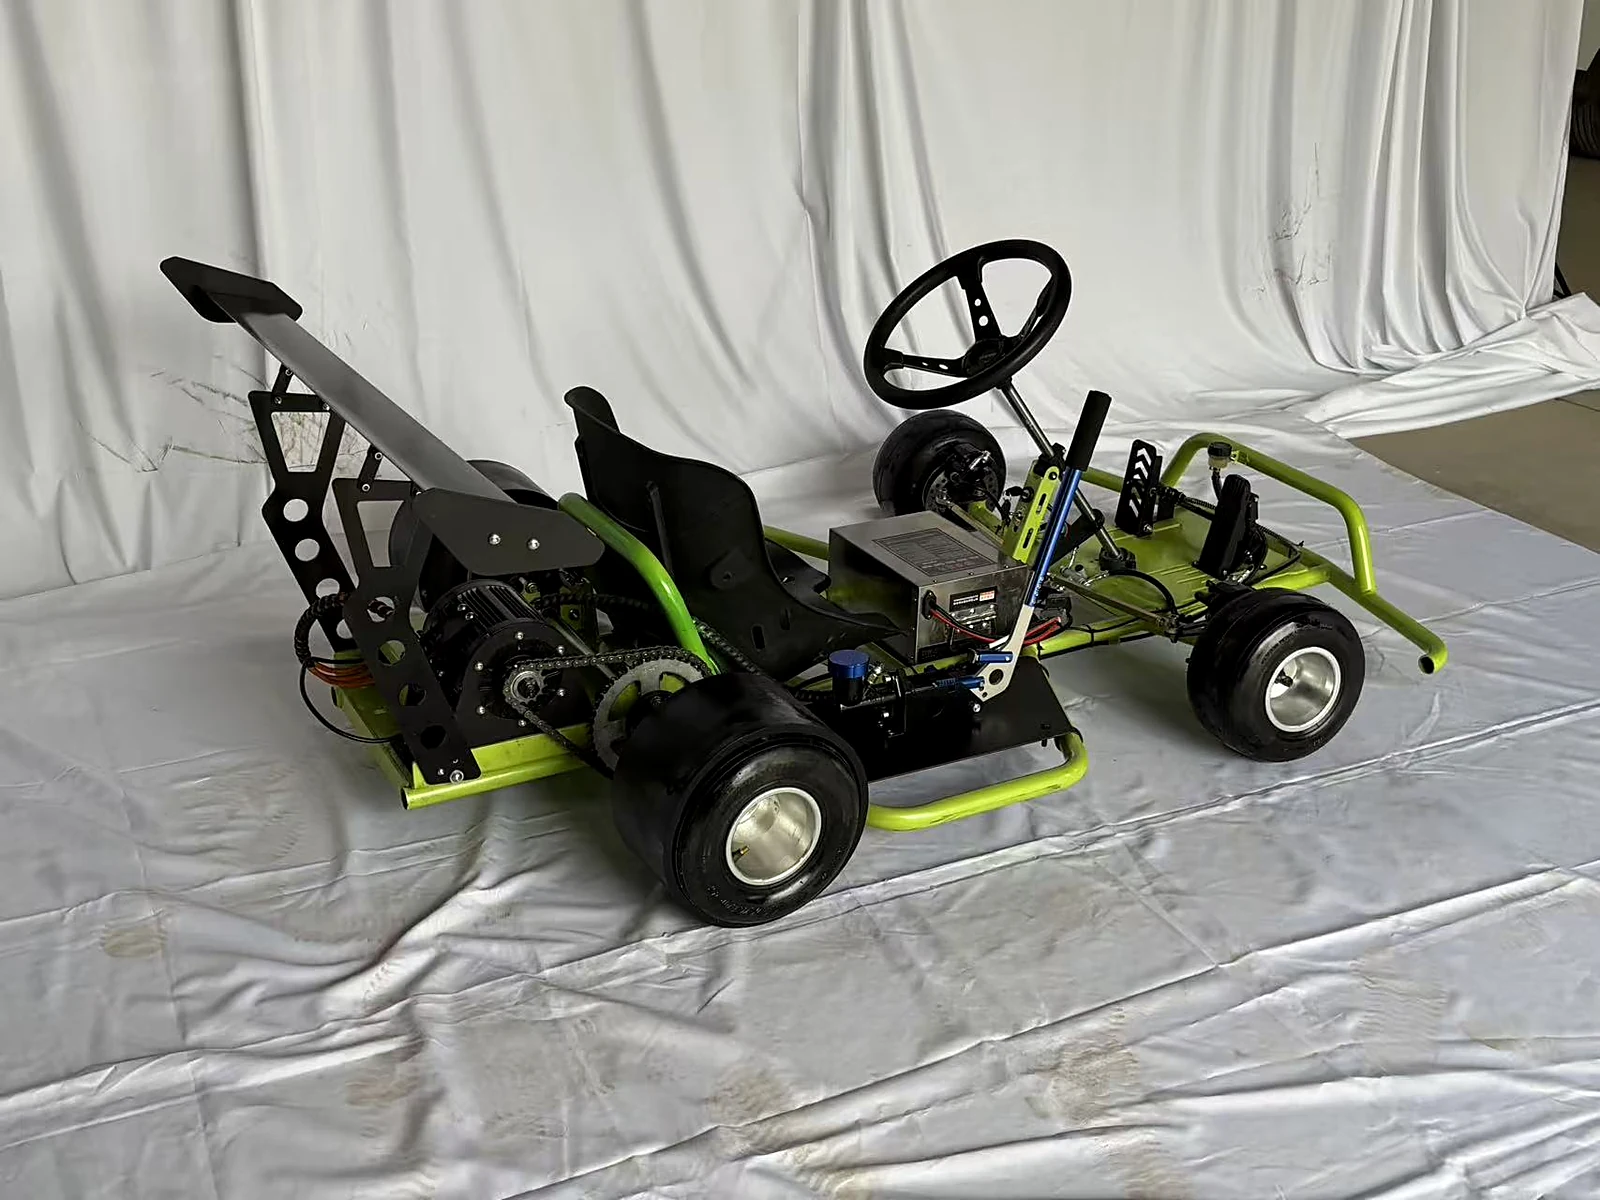
Description
Our go-kart frame chassis is manufactured from ERW cold-drawn steel tubing (Φ25mm-Φ32mm, wall 1.5-2.0mm), CNC bent to exact racing specifications. The frame is fully TIG welded at all critical junctions for maximum structural integrity, then stress-relief annealed to eliminate welding distortion. Each chassis is jig-welded on a precision fixture ensuring dimensional accuracy within ±1mm. Final finish is epoxy primer + powder coating for corrosion protection and professional appearance.
Specifications
| Parameter | Value |
|---|---|
| Material | ERW Cold-drawn Steel Tube (Q345) |
| Tube Diameter | Φ25mm / Φ28mm / Φ32mm |
| Wall Thickness | 1.5mm / 1.8mm / 2.0mm |
| Wheelbase | 1040mm (standard) / custom |
| Overall Length | 1720mm (standard) / custom |
| Track Width | 1100mm front / 1150mm rear |
| Weight | 18-22kg (depending on configuration) |
| Welding | TIG at critical joints / MIG at secondary |
Materials
- Q345 ERW Steel Tube
- 4130 Chromoly (optional upgrade)
Processes
- CNC Tube Bending
- Jig Welding (TIG+MIG)
- Stress Relief Annealing
- Powder Coating
Manufacturing Notes
A go-kart chassis is a welded structure that has to be straight, and it has to stay straight through the heat of welding and the heat of coating. Most of the process planning goes into controlling distortion.
- Tube specification and wall thickness: Chassis tube wall thickness is selected from the intended use and the class rules — a recreational frame and a race frame do not use the same wall. Send the class or the target weight and we will specify from there rather than defaulting to a heavy wall.
- Cutting and notching: Tubes are laser cut and fish-mouthed to fit the mating tube, so joints close up without gaps. Gap-filling with weld wire is what pulls a frame out of alignment as it cools.
- Welding sequence and fixturing: The frame is built in a jig and welded in a sequence designed to balance heat input on opposite sides of the structure. Weld-on tabs and brackets are positioned in the jig, not measured afterwards.
- Post-weld correction and finish: After welding the frame is checked for twist and corrected while it is still on the fixture. Coating is powder coat or wet paint depending on the finish specified, with the frame supported so it does not sag while curing.
Surface Finishes
- Epoxy Primer + Powder Coat
- Powder Coat Only (economy)
Order Information
- MOQ: 30 frames per design
- Lead Time: 30-45 days (new design requires 15-day tooling/fixture setup)
- Sample Policy: 1 prototype frame available; prototype cost $450-800 depending on complexity, deductible from orders ≥100 units
- Packaging: Individual bubble wrap + carton; or steel rack loading for container shipment
Applications
- Recreational go-karts
- Racing karts (cadet/junior/senior)
- Amusement park karts
- Off-road buggy frames
- Custom motorsport projects
Inspection & Quality Control
A chassis is a single assembly, so every frame is checked individually rather than by sampling.
- Incoming material: Tube outer diameter and wall thickness checked on the batch; material certificate held for the tube grade used.
- Jig and fixture check: The welding jig is verified before each production run so the reference dimensions in the jig are still correct.
- Dimensional check on the frame: Key mounting points, wheelbase, track width and engine or motor mount positions are measured on every frame after welding and recorded.
- Twist and straightness: The frame is set on a flat reference and checked for twist across the diagonals; out-of-tolerance frames are corrected before they leave the jig.
- Weld inspection: Visual inspection of all welds on every frame, with penetration checked on sample joints from each run.
Key Features
- Jig-welded on precision fixtures (±1mm dimensional accuracy)
- Stress-relief annealed for dimensional stability
- TIG welded at all critical stress points
- Engine mount, seat mount, and pedal mounts pre-fabricated
- Compatible with standard Honda GX200 / GX160 engine mounts
Send drawings and we will check them against our DFM engineering review capability before quoting. You can also see how this fits into our custom metal enclosure manufacturing work, or read Network Cabinet Enclosure Manufacturing Guide first if you are still comparing options.
Frequently Asked Questions
Do you build from our drawings or do you design the chassis?
Both are possible. Most customers send a drawing or a CAD model. If you have a design concept but no drawings, we can fabricate from a reference frame or a dimensional specification, but the structural design remains the customer’s responsibility.
Can you add brackets for our components?
Yes. Engine or motor mounts, seat mounts, bearing hangers, pedal brackets and brake mounts are all positioned in the welding jig, so they are located off the same datum as the rest of the frame.
How do you keep the frame from distorting during welding?
The frame is welded in a jig in a balanced sequence, with the heat spread on opposite sides of the structure. Fit-up is controlled by laser-cut, fish-mouthed tube ends so no gap has to be filled with extra weld.
What is the MOQ?
10 frames for a fabricated welded assembly of this size. Prototype frames can be quoted separately if you need to validate the design before committing to a production run.