
Repeat production program
SUS304 Industrial Brackets for OEM Programs
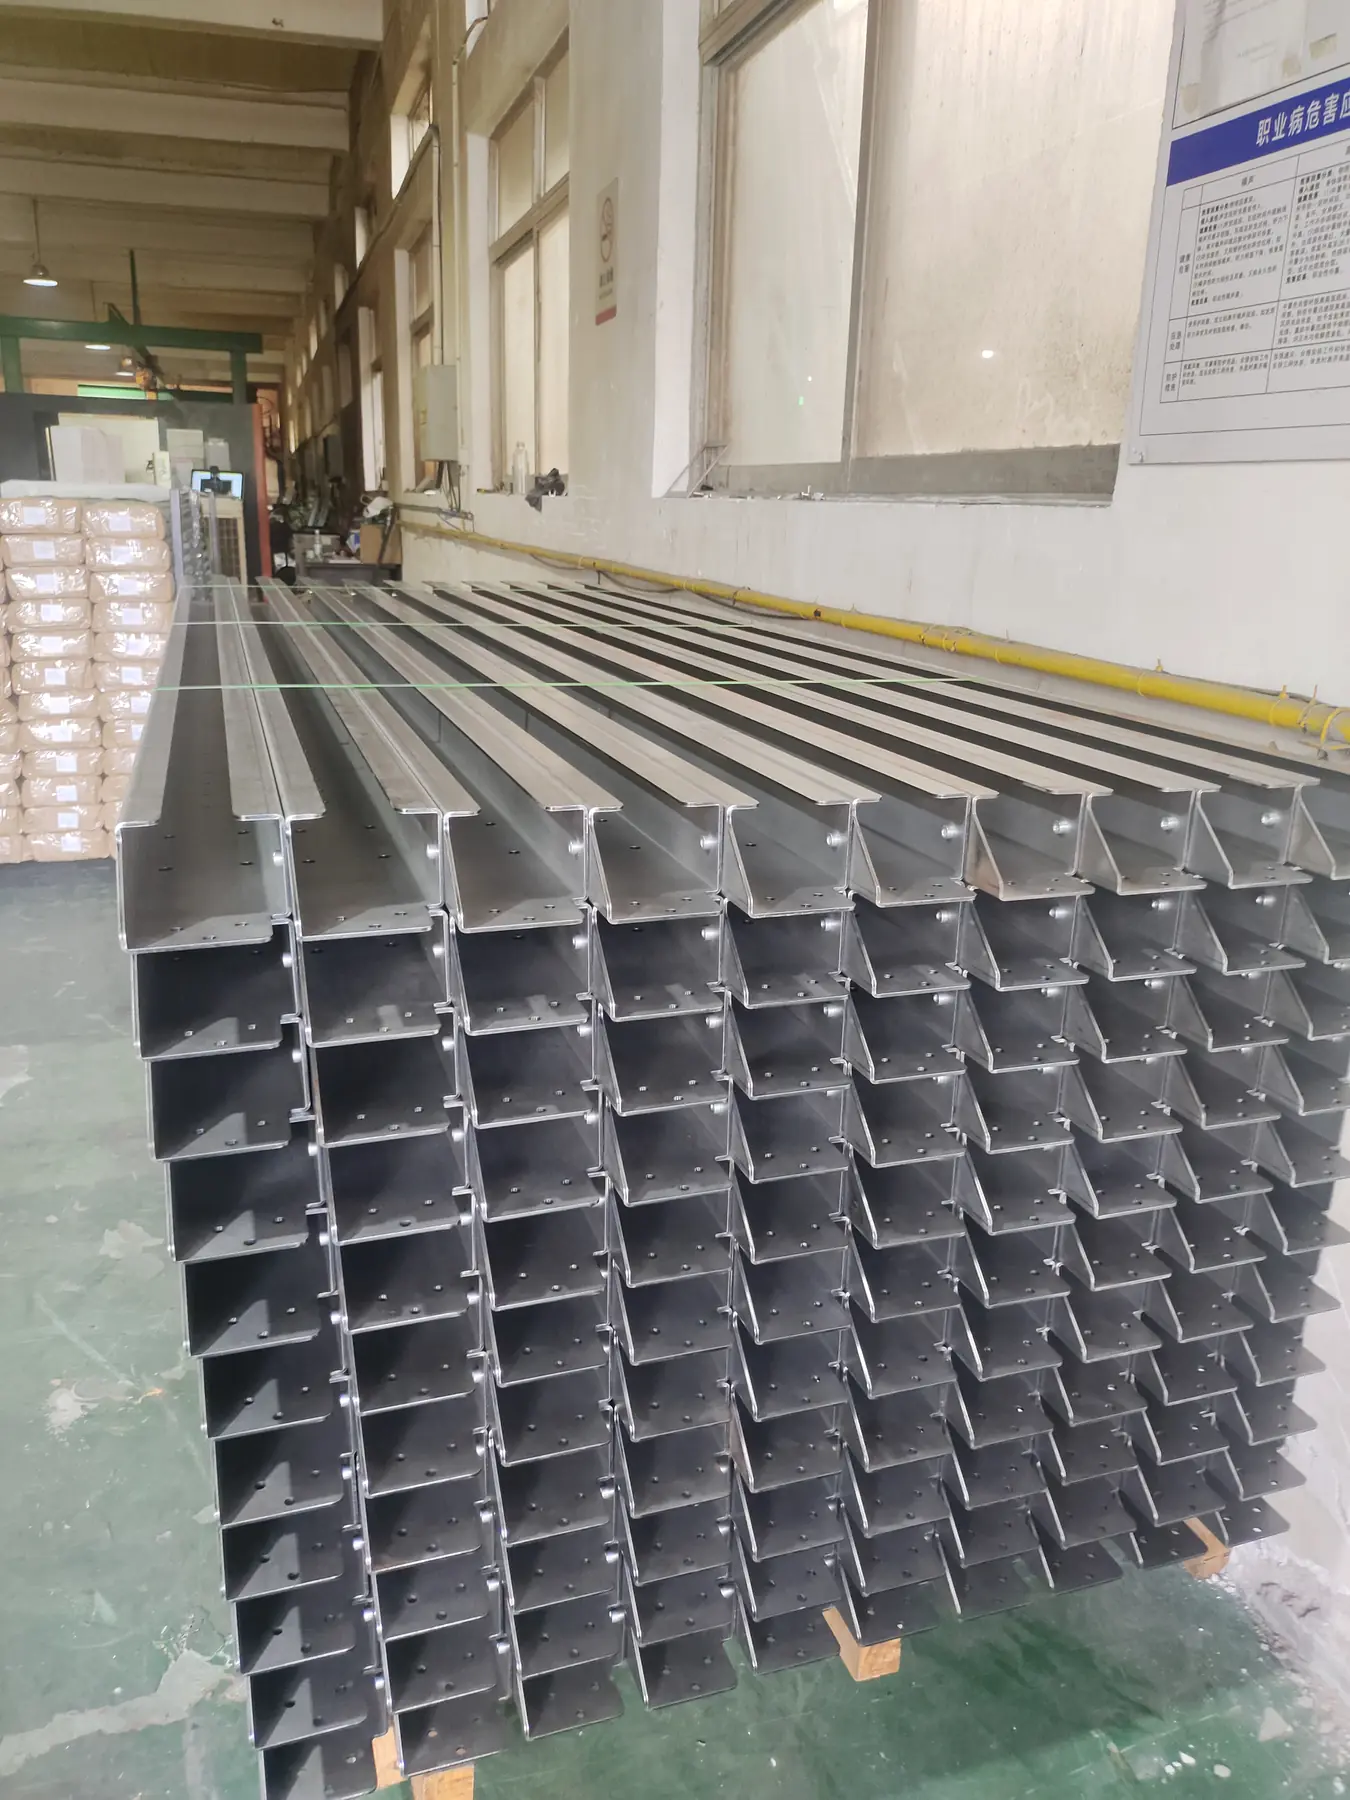
These brackets are produced in 1.5 mm SUS304 with a natural stainless steel finish, for industrial applications.
What the Bracket Programme Has Already Fixed
| Product type | SUS304 Industrial Brackets |
|---|---|
| Material and thickness | SUS304, 1.5 mm |
| Surface finish | Natural stainless steel |
| Drawing formats accepted | STEP, DWG, DXF, PDF and SolidWorks |
| Project tolerances | Confirmed against the buyer drawing and manufacturing review |
Application context
What a Bracket Has to Carry and Keep Aligned
The photographed parts are long formed brackets produced in batch quantities. For an OEM program at this scale, the manufacturing challenge is not only making one acceptable sample. Hole position, flange geometry, straightness, joining points and part-to-part consistency must remain controlled across repeat orders.
Engineering review
Decisions That Change How a Bracket Is Formed
The drawing review should identify functional holes, mating faces, bend orientation, edge conditions and any welded or inserted hardware. Consistent bend radii and a practical relationship between holes and bend lines help reduce deformation. Critical dimensions should be separated from general dimensions so inspection effort is focused where the assembly actually depends on it.
Manufacturing route
How a Bracket Programme Reaches Repeat Orders
- Drawing and load-path reviewMounting holes, slot direction, bend line and the way the load enters the bracket are read together, because a bracket that fits can still fail at the bend.
- Sample bend and hole checkOne piece is formed and the hole positions are checked against the mating frame before the batch setting is fixed.
- Batch manufactureCutting, bending and any welding to the confirmed setup, with the same tooling held for repeat orders.
- Inspection and packingDimensions are checked from the agreed datums, and parts are packed so that hole faces and finished faces are not damaged in transit.
Quality approach
How Bracket Dimensions Are Checked Against the Drawing
Production checks should follow the approved drawing and sample. Typical checkpoints include incoming material confirmation, first-piece verification, bend-angle and key-distance checks, joining-point inspection, burr and sharp-edge review, and final quantity and packing verification. Acceptance criteria are agreed with the buyer rather than assumed from a generic tolerance statement.
Request a project review
Planning a Bracket Programme Like This One?
Send the mounting interface, the load case if one is defined, the trial quantity and the annual demand, plus material, thickness and finish. On a bracket the datum scheme is worth agreeing early: it decides how hole position is measured, and it is the most common reason a first article is rejected. See how bending is controlled and what a drawing review covers.
Holding Consistency Across a Repeat Production Run
This page already sets out the route from drawing to repeat order. The question that decides whether a repeat program works is narrower than that: whether part number 5,000 is the same as the one that was approved. That is a different discipline, and it is mostly about what gets recorded.
| Stage | What happens | What is checked |
|---|---|---|
| Nesting and blank layout | How the parts come off the sheet, including the grain direction the part needs | The layout is agreed before the first sheet is cut. Changing nesting later changes the grain direction of every part after it, and a bracket formed across the grain behaves differently |
| First-off confirmation | The first part of the run is produced and held before volume begins | Every dimension the drawing calls critical, plus the hole positions that the fixture is checked against. The first-off is the record for the run |
| Bend sequence and tooling | The order in which the bends are made, and the tooling used for each | That the sequence is written down. A bracket bent in a different order can land inside tolerance and still not be identical, which shows at assembly rather than at goods-in |
| Tool wear and consumable count | Punch and die condition through the run, and the count between changes | That consumables are changed on a count rather than on appearance, because the last parts before a change are where a burr appears |
| Interval checking | Sampling at a set interval while the run continues | The critical dimensions and the hole positions, so a drift is caught while the run is still running rather than at the end of it |
| Edge and surface condition | How the edges are treated on a part with no coating to hide them | That the edge condition is consistent part to part, since on natural stainless the edge is the whole finish |
| Packing and batch identification | Parts counted, packed and identified per batch | That a delivered batch can be traced back to its material certificate and its production record |
Changes That Do Not Force New Tooling on Brackets
On a repeat program the useful changes are the ones that do not disturb the approved characteristics.
| What can be changed | What it affects | What it does not affect |
|---|---|---|
| Thickness | Stiffness, weight and how the part forms | The bend sequence, provided the radii stay the same |
| Grade: 304 or 316 | Corrosion behaviour where the bracket is used | The forming operations, if the grade still takes the same radii |
| Edge treatment: as-cut, deburred or dressed | Handling safety and the appearance of the finished part | The dimensions |
| Tolerance on non-critical dimensions | Cost, by taking inspection effort off dimensions that do not matter | The characteristics the drawing calls critical |
| Packing: bulk, bagged or kitted | How the parts are handled and issued on your line | The part |
| Run length and delivery schedule | How the run is planned, and whether a dedicated fixture is justified | Nothing on the drawing |
Grain Direction on a Formed Bracket Is a Specification Item Most Drawings Omit
Rolled sheet has a grain, and a bend made across the grain behaves differently from one made along it. On a 1.5 mm stainless bracket this matters for two reasons: a bend across the grain is more likely to crack at a tight radius, and a bend along it springs back differently. Both show up as inconsistency rather than as failure – the first-off fits, the tenth part is a degree out, and the cause is that the nesting put the parts on the sheet in a different orientation.
- If a bracket has a critical bend, say which way it runs relative to the sheet. It costs nothing to nest correctly and it removes a variable.
- Springback on stainless is larger than on carbon steel and it varies with the material condition. The compensation is set from the first-off and then held for the run.
- A bracket that is laser cut has a heat-affected edge. On stainless that edge can show a slight discolouration which a natural finish does not hide.
Why the First-Off Is Held Before a Bracket Run Starts
A bracket programme is defined by consistency rather than by the first part, because the tenth and the thousandth are what the customer assembles. The first-off exists to fix the variables – bend sequence, tooling, springback compensation, hole positions – and once they are fixed they are recorded so that a repeat order six months later is made the same way. Without that, a repeat order is a fresh setup with a fresh set of small differences, and the differences are what a customer notices when the parts go into a fixture.
What we hold from the first-off is the nesting and grain direction, the bend sequence and the tooling used for each bend, and the compensation values. That is the record that makes a repeat order a repeat. If your brackets are checked in a fixture at your end, tell us which datums the fixture uses – we will inspect to those rather than to our own, because a part that is in tolerance on our datum scheme and out on yours is still a problem at your assembly line. Lead time is quoted after drawing review and process confirmation.
Questions Buyers Ask About Bracket Programmes
How do we keep a repeat order identical to the last one?
By sending the previous order reference. The bend sequence, the tooling and the first-off record are held against the part, so a repeat order is run to the same settings rather than re-derived from the drawing. That is the difference between a repeat program and a series of similar orders.
What changes when the quantity goes up?
Usually two things: the nesting and the fixture. A larger run can justify a dedicated fixture, which removes set-up variation between batches, and it usually improves material utilisation because the layout can be optimised over more parts. Both are worth costing rather than assuming.
Why does the packing matter on a simple bracket?
Because a natural stainless bracket arrives with its edges as the finish, and a part that has rubbed against another in a box is a rejected part. Packing also carries the batch identification, which is what allows a delivered batch to be traced back to the material certificate if a question is raised months later.
Consistency is a record-keeping discipline as much as a manufacturing one. Send the drawing and the order reference for the previous run through the RFQ form and the repeat is planned to the same settings. Related: material certification, in-process inspection and export packaging.
Payment Terms
How a project is paid for is agreed before production starts, and the structure that applies to your order is stated on the quotation and on the order confirmation, so there is no ambiguity later.
- 30% advance payment with the order and the 70% balance before shipment — our standard structure.
- 70% advance payment with the order and the 30% balance before shipment — used for some projects.
- 100% payment in advance before production starts — used for some projects.
If your finance team works to a fixed structure, say so in the first enquiry and we will confirm what applies to your order before you commit. Request a quotation.
Questions buyers ask before sending drawings
The questions that come up most often before a project starts, answered the way we answer them by email.
What do you need from me to quote SUS304 Industrial Brackets for OEM Programs?
2D drawings as PDF, DWG or DXF, or 3D files as STEP, IGES or SolidWorks, together with material grade, sheet thickness, surface finish, quantity and destination country. If the drawing is not finished yet, send a photo, a sketch or the existing part instead — we review what can be measured from it and reply with the questions that still need answering.
How long does a quotation take?
Enquiries are answered within one business day. Simple laser-cut and bent parts are quoted within 24 hours. Welded frames, assembled units and multi-part structures are quoted after the drawing review and process confirmation, and the date is confirmed in our reply.
Is there a minimum order quantity?
Prototypes are made from a single piece and small batches of 10–50 pieces are routine. Prototype, first batch and repeat volume are quoted together so the numbers stay consistent as the project scales.
Can you work from a sample or a photo if I have no drawing?
Yes. Send the part itself, clear photographs with a rule or caliper in frame, or a dimensioned sketch. We measure what can be measured, list what is still undefined, and confirm it with you before production.
Need a Similar Part?
Most enquiries that start on a page like this are not an order for SUS304 Industrial Brackets for OEM Programs — they are a search for a factory that can make something like it. Send us your drawing, 3D model or sample and we will review the manufacturing process and the quotation requirements, then come back with a process plan, a price and a lead time.
We work from 2D drawings, STEP / DWG / DXF / PDF files, or a physical sample if that is all you have.
No complete drawings yet? Describe the part, send photos or a sketch, or send a sample — we can start from there. Discuss your project.
Trade Terms and Delivery
We quote under the standard Incoterms your logistics team already works with, and build the packing and documentation around the one you choose.
- EXW — you collect from our Ningbo facility and run export clearance through your own forwarder.
- FOB Ningbo — we deliver to the vessel at Ningbo port and handle export clearance.
- CIF — we cover carriage and insurance to your named destination port.
- DDP — we handle carriage, insurance, import clearance and duties through to your door.
Send your destination country, target delivery date and preferred trade term together with the drawing. Request a quotation.
Quotation Time
We quote from your drawings. How long that takes depends on what the part asks for:
- Simple parts — quoted within 24 hours. Laser-cut blanks and bent components, supplied with complete 2D or 3D drawings. Mon–Fri, GMT+8.
- Complex assemblies — quoted after the drawing review. Payment kiosks, multi-part welded frames, enclosures with purchased hardware, or anything needing a coating or assembly trial. We confirm a quotation date once the scope is clear.
Production lead time is quoted separately, after drawing review and process confirmation. Send your drawings.
What stands behind this quotation
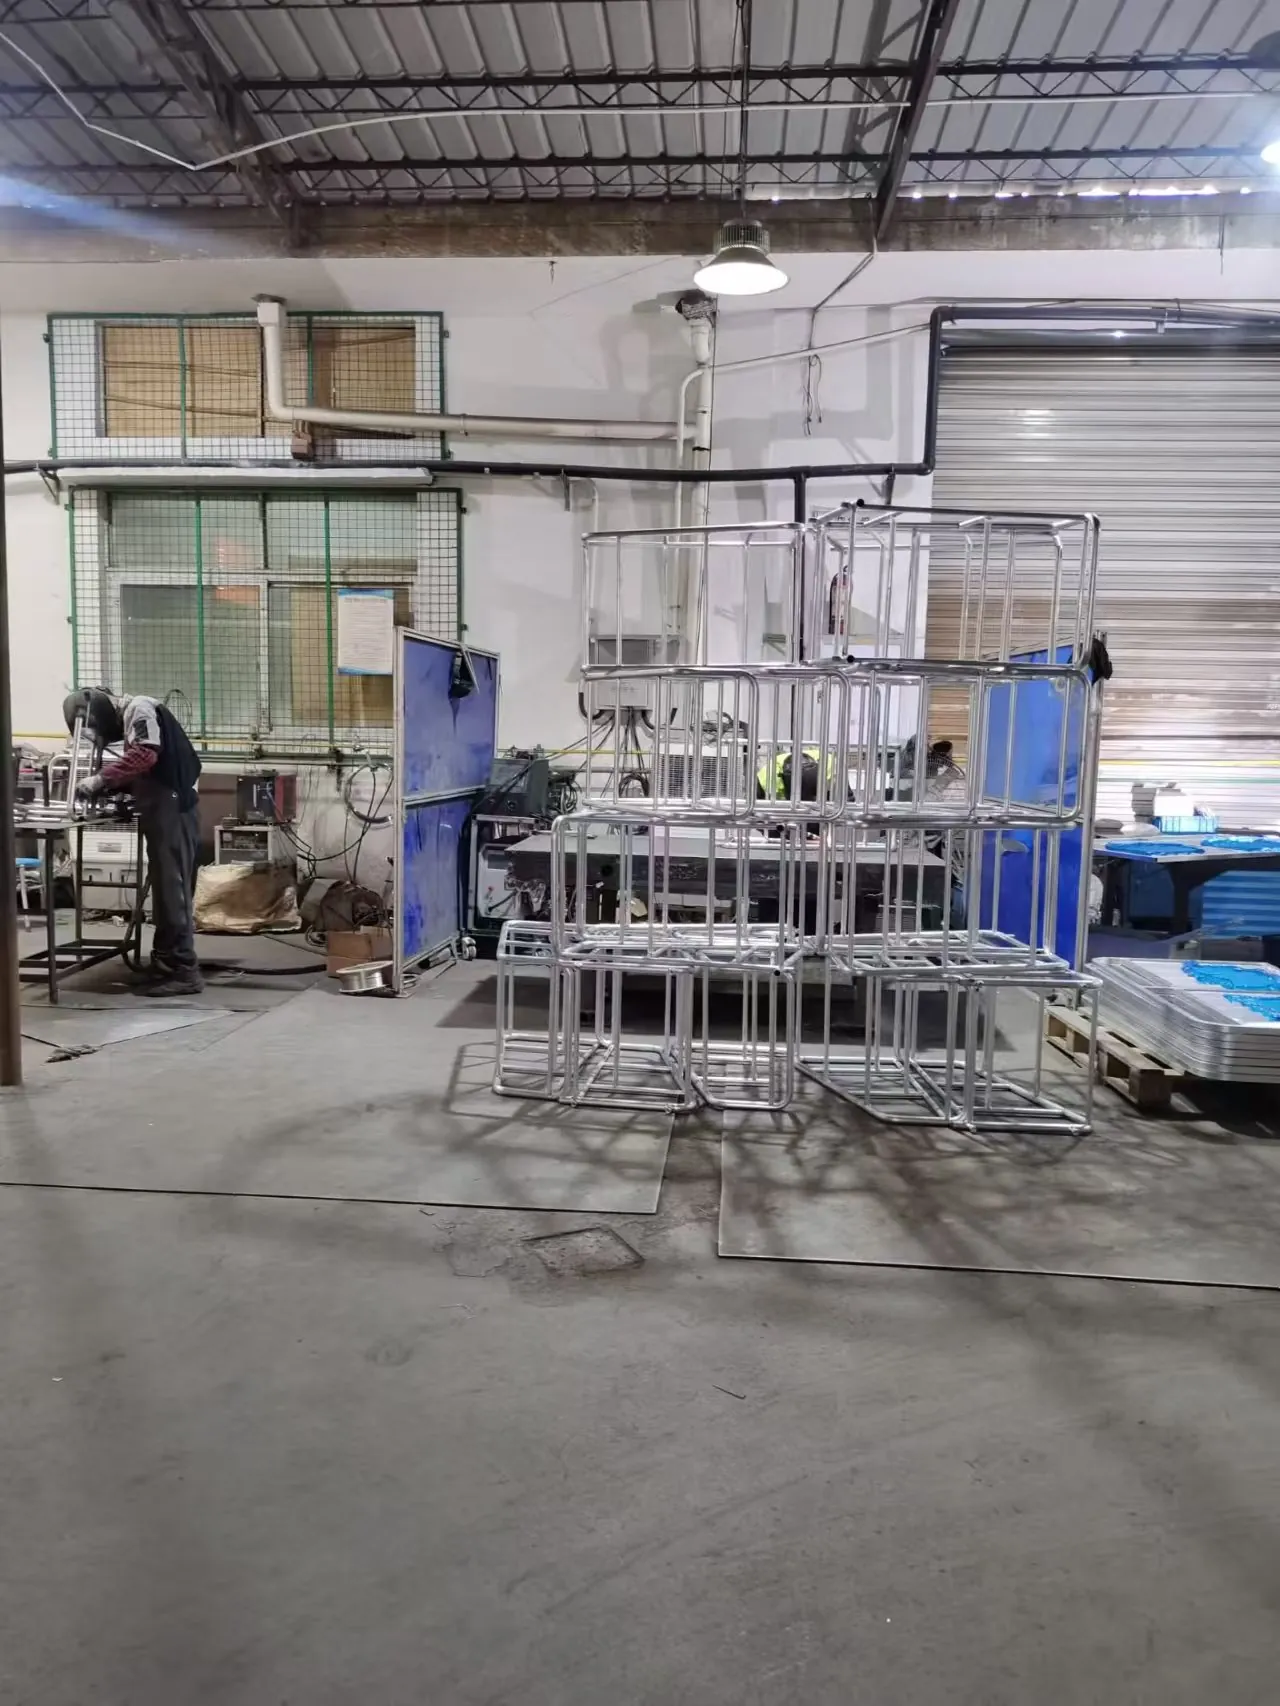
- Manufacturing since 20162,500 m² Ningbo plant — 3 laser cutting machines (including newer TRUMPF), 4 CNC press brakes and 10 welding stations.
- Shipped to more than 30 export marketsEnclosures, cabinets and formed parts supplied to OEM buyers across Europe, North America and Asia.
- 123 documented product casesMedical device housings, HVAC and heat pump enclosures, agricultural and livestock equipment, industrial hydraulics, material handling trolleys and EV charging cabinets.
- Factory evidence you can checkTUV Rheinland audit reference MIC-ASI243729 and Bureau Veritas reference MIC-ASR263630 available for buyer review under NDA.
Before you send drawings: an NDA is signed on request · first-article inspection is carried out before a batch continues · pricing is staged from prototype quantity to repeat volume · pre-shipment photos and packing records are prepared when the project needs them.