
Structural fabrication knowledge
Heavy Steel Plate Welding for Fabricated Equipment
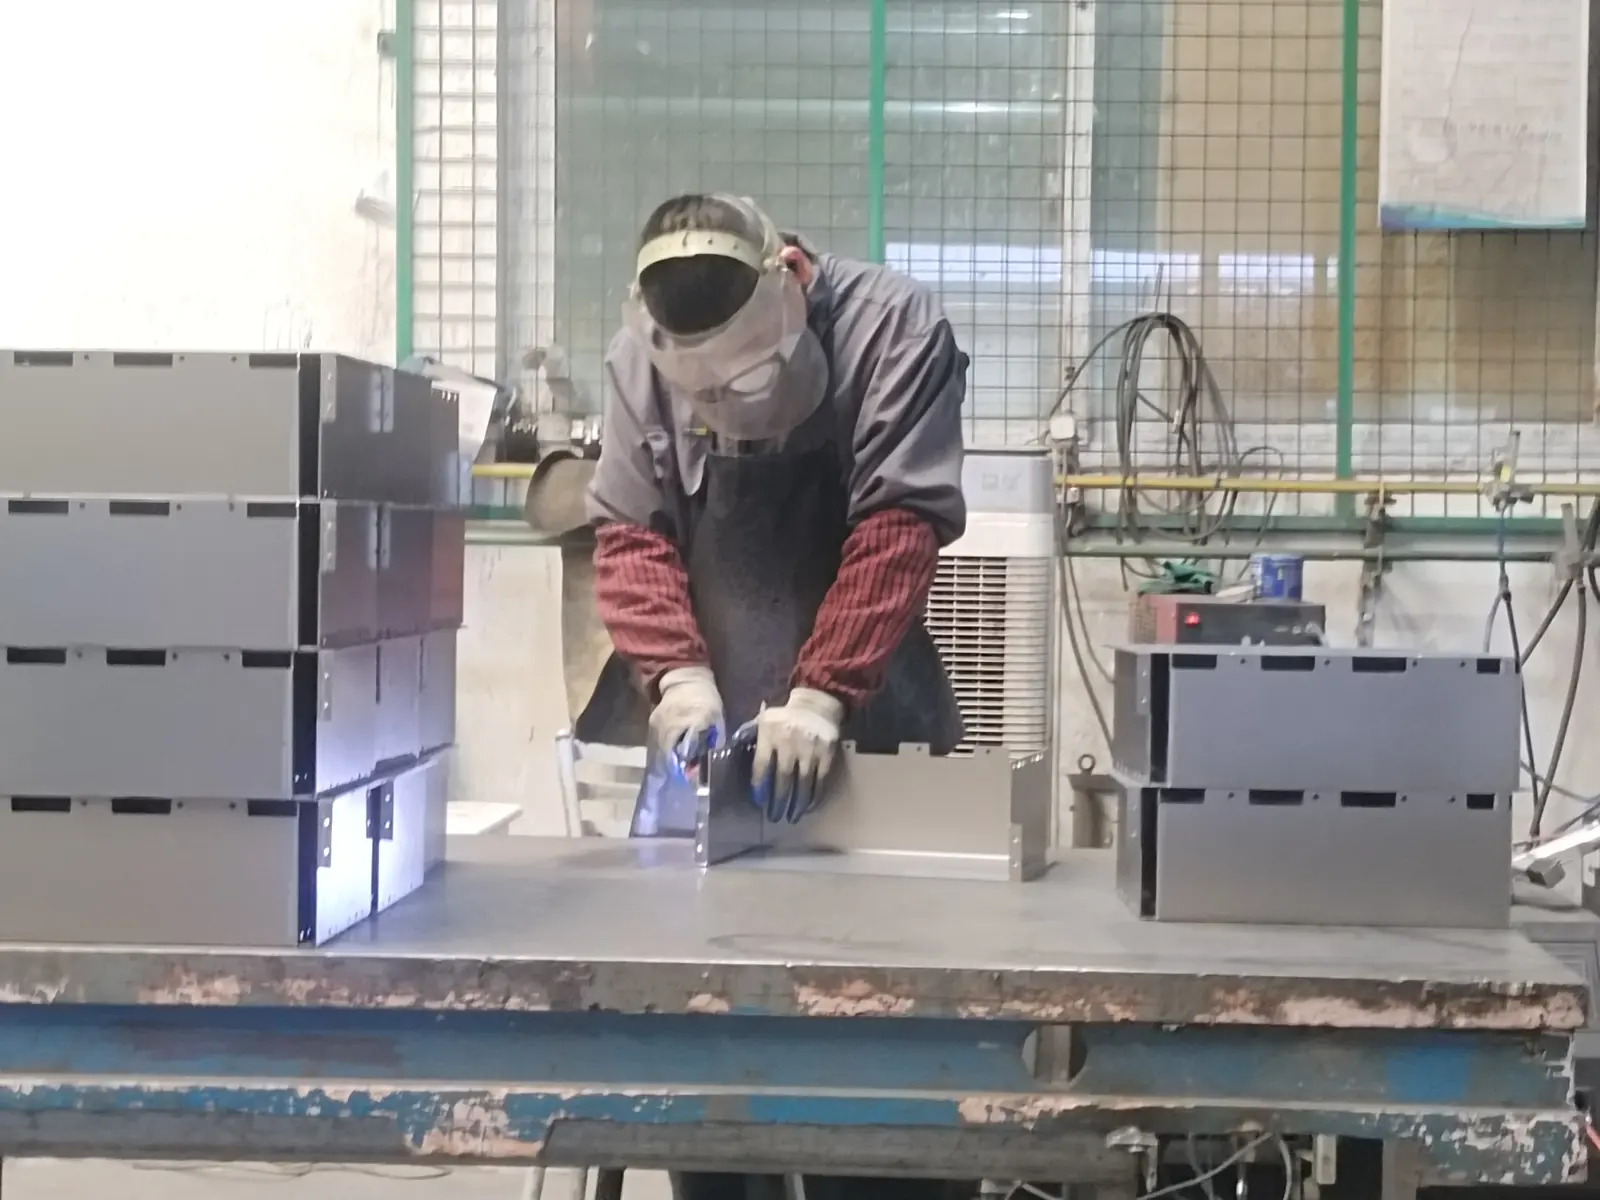
Heavy steel plate welding is controlled by joint preparation, fit-up, restraint, heat input, welding sequence and the inspection level required by the drawing. Plate thickness alone does not define the process, and structural or coded work must be quoted against the applicable specification.
Buyer summary
What to Decide Before Requesting a Quote
| Buyer application | Bases, frames, supports and heavy equipment fabrications |
|---|---|
| Drawing information | Joint geometry, weld symbols, load-critical areas and acceptance standard |
| Main production risks | Incomplete fusion, excessive distortion, residual stress and dimensional drift |
| Inspection focus | Fit-up, weld profile, drawing dimensions and specified test evidence |
Joint Preparation Determines Whether the Weld Is Accessible
Thicker material may require edge preparation and a root condition that allows the required weld to be produced. The drawing should identify joint type and accessible welding sides instead of leaving the supplier to infer a structural detail.
Prepared edges, cleanliness and root gap need to remain consistent through the batch. When a joint is hidden after assembly, the inspection hold point must occur before it becomes inaccessible.
Heat Management Must Follow the Finished Geometry
Heavy weldments can still distort. Long seams, unbalanced joints and concentrated welding around one corner can move mounting faces or create twist across the frame. Tack sequence, fixture support and alternating work are planned around the final datums.
Preheat, interpass control, filler selection and welding procedure depend on the exact steel grade, thickness and governing requirement. They should never be copied from a generic internet table into a production instruction.
Inspection Scope Comes from Risk and Specification
Visual inspection and dimensional verification are normal starting points. Additional testing or documented welding requirements are included only when the buyer specifies them and the responsible parties agree the standard and acceptance criteria.
For equipment builders, the most useful drawing information is often the location of machined or mounted interfaces after welding. Those faces determine fixture strategy, correction allowance and the point at which the assembly should be measured.
Buyer questions
Questions Procurement and Engineering Teams Usually Ask
These answers define the discussion points. Final values and acceptance criteria are confirmed against the project drawing and purchase requirements.
What information is needed for a heavy welded frame quote?
Provide material grade and thickness, weld symbols, joint preparation, load-critical features, key datums, required inspection and the finished assembly drawing.
Can a thick weldment be held to sheet-metal tolerances?
Not by assumption. Heat input, restraint, weld sequence and machining or straightening allowance must be reviewed around the functional interfaces.
When are additional weld tests required?
The buyer or responsible engineer should define any project-specific NDT, procedure qualification or acceptance standard before quotation.
RFQ checklist
Information That Makes the Technical Reply Useful
- Provide steel grade, thickness and material-document needs
- Define joint geometry and weld symbols
- Identify load-critical and machined interfaces
- State applicable welding or inspection standard
- Share batch quantity and finished assembly drawing
Thickness Drives Preheat, Pass Count and Inspection Scope
Above roughly 6 mm the governing variable is not the welding technique but thermal management: how much preheat is needed to avoid hydrogen cracking, how many passes the joint needs, and what inspection method can actually see into the finished weld.
| Plate thickness | Groove and passes | Preheat guidance | Heat input window | Inspection that suits it |
|---|---|---|---|---|
| 6-12 mm | Single V or bevel, 2-4 passes | Usually ambient for low-carbon steel; confirm against carbon equivalent | 0.8-2.0 kJ/mm | Visual plus surface crack detection |
| 12-25 mm | Double V or X, 5-12 passes | Commonly 50-100 C for carbon steel | 1.0-2.5 kJ/mm | Visual plus ultrasonic examination |
| 25-50 mm | X or U, 12-30 passes | Commonly 100-150 C, with interpass controlled | 1.5-3.5 kJ/mm | Volumetric examination plus surface crack detection |
| Above 50 mm | Double U or J, many passes | 150-200 C, often followed by post-weld heat treatment | Controlled by the qualified procedure | Full volumetric examination, plus post-weld heat treatment records |
Preheat is not a number to be guessed. The usual basis is carbon equivalent, calculated as C plus Mn/6 plus (Cr + Mo + V)/5 plus (Ni + Cu)/15. Below about 0.40 the steel is generally weldable without preheat; between 0.40 and 0.60 preheat in the 50-150 C range with low-hydrogen consumables is the normal response; above 0.60 the joint needs preheat, low-hydrogen practice and usually post-weld heat treatment. Consumables matter as much as the plate: electrodes that have absorbed moisture put hydrogen into the weld regardless of how carefully the plate was preheated.
From research to RFQ
Apply the Guidance to Your Actual Drawing
Send the current files, quantity, material, finish and assembly context. We will identify the questions needed for a practical manufacturing review.
What stands behind this quotation
- Manufacturing since 20162,500 m² Ningbo plant — 3 laser cutting machines (including newer TRUMPF), 4 CNC press brakes and 10 welding stations.
- Shipped to more than 30 export marketsEnclosures, cabinets and formed parts supplied to OEM buyers across Europe, North America and Asia.
- 123 documented product casesMedical device housings, HVAC and heat pump enclosures, agricultural and livestock equipment, industrial hydraulics, material handling trolleys and EV charging cabinets.
- Factory evidence you can checkTUV Rheinland audit reference MIC-ASI243729 and Bureau Veritas reference MIC-ASR263630 available for buyer review on request.
Before you send drawings: project confidentiality is default · first-article inspection is carried out before a batch continues · pricing is staged from prototype quantity to repeat volume · pre-shipment photos and packing records are prepared when the project needs them.