
Most weld defects are not mysterious. They fall into three groups: defects caused by settings, defects caused by preparation and discipline, and defects the design has already decided. Sorting a problem into the right group is what makes the fix permanent instead of a repeat visit.
Where Weld Defects Actually Come From
Porosity, cracking, undercut and the rest are symptoms. The cause behind them falls into one of three groups, and the group determines who can fix it.
| Group | What it covers | Who can fix it |
|---|---|---|
| Setting-driven | Current, voltage, travel speed, torch angle, wire feed, gas flow rate | The welder, at the machine, on the next part |
| Preparation-driven | Cleanliness, joint fit-up, root gap, interpass cleaning, consumable storage, draughts | Whoever prepares the joint — and no parameter change will cure it |
| Design-driven | Weld size and count, joint accessibility, restraint, symmetry of the weld layout | Nobody at the bench; it has to be corrected on the drawing |
The second group is where most defects live and where most money is lost, because a preparation failure is invisible until inspection. The third group is the one buyers most often miss: a part that distorts on every run, no matter who welds it, is usually telling you something about the weld layout rather than the welder.
Porosity: Gas Entrapped in the Weld
Gas trapped as the weld pool freezes. On the surface it appears as pits; inside it forms the elongated voids known as worm tracks. It is the most common defect in sheet metal work, and the least often caused by the settings.
The gas has to come from somewhere. The usual sources are oil, paint, rust, moisture, a galvanised or plated surface, damp filler wire, or a shielding problem — flow rate too low to cover the pool, flow rate so high that it becomes turbulent and draws air in, a blocked nozzle, a draught crossing the arc, or the wrong gas for the process.
Two consequences are worth knowing. Porosity reduces the load-bearing section and is a fatigue initiation site, so it matters most on parts that see cyclic loading. And if the part will be powder coated, gas trapped in surface porosity can escape during the curing bake and blister the coating, which turns a weld problem into a finishing rework.
Detection: visual inspection finds surface porosity; radiography or ultrasonic testing is needed for what sits inside.
Cracking: Hot, Cold and Hydrogen-Induced
Cracking is treated as the most serious defect because, unlike porosity, a crack propagates. It also splits into two mechanisms that behave completely differently, and confusing them leads to the wrong fix.
Solidification cracking (hot cracking)
Occurs while the weld is still freezing. Low-melting-point impurities — sulphur and phosphorus in steel, and their equivalents in other alloys — segregate to the centre of the bead as it solidifies. Welds with a high depth-to-width ratio concentrate that segregation on the centreline, which is why a deep, narrow bead is more crack-prone than a wider one at the same heat input. The crater at the end of a run is a common starting point, because it freezes last and is often left concave.
Hydrogen-induced cracking (cold or delayed cracking)
Occurs after the weld has cooled, sometimes hours or days later. Three conditions have to line up: hydrogen present in the weld, a hard brittle microstructure in the heat-affected zone, and tensile restraint. Remove any one of the three and the crack does not form. That is why prevention is about consumable handling, preheat matched to the material, and restraint — not about welding technique alone.
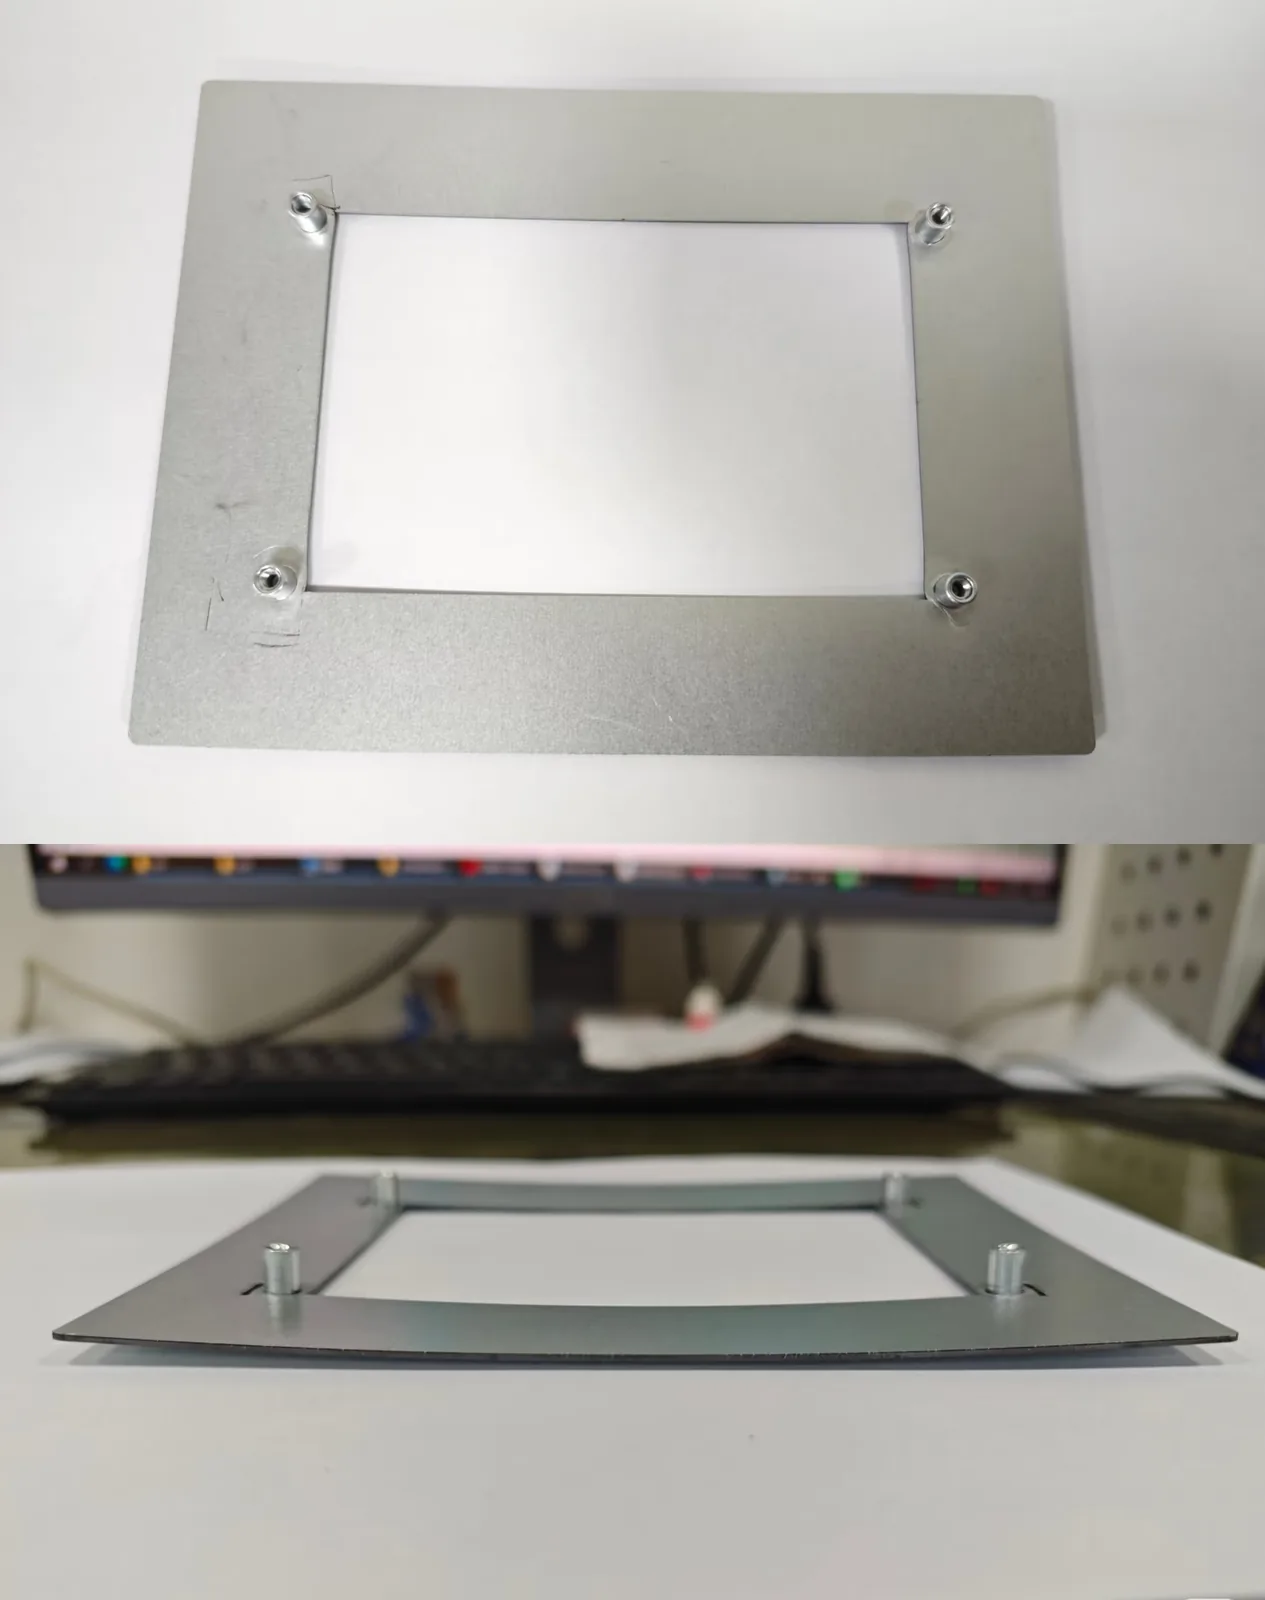
The delay is the practical problem. A weld that looks sound at the end of a shift can crack overnight in a hard, restrained joint, which is why inspection timing belongs in the plan for crack-sensitive work rather than being left to whenever the inspector is free.
Detection: dye penetrant or magnetic particle for surface-breaking cracks, ultrasonic testing for what lies beneath.
Undercut: the Notch at the Weld Toe
Undercut is a groove melted into the parent metal along the edge of the weld, left unfilled. It reduces the cross-section and, more importantly, creates a sharp notch exactly where the stress concentrates — so it behaves as a fatigue crack starter even when the depth looks small.
The causes are setting-driven: current too high, travel speed too high, torch angle wrong, or arc length too long. It shows up most in vertical and overhead positions, where the operator is fighting gravity for control of the pool.
The procurement point: undercut is frequently rejectable on its own in cyclic-loading service, even at a depth that would be acceptable on a static part. If the drawing does not state an acceptance level, that conversation happens at inspection instead of at quotation.
Incomplete Fusion: When the Bead Does Not Bond
Weld metal sits against the parent metal or a previous pass without fusing to it. Because it is a planar defect rather than a rounded void, it concentrates stress in much the same way a crack does, which is why it is treated more seriously than gas porosity of equivalent size.
Typical causes: heat input too low for the joint volume, travel too fast, an oxide or oil film on the joint face, slag left between passes, or a work angle that points the arc away from the root. If the fusion line is at the root, there is an additional cause: the operator simply could not see it.
Incomplete fusion at the start of a run is a well-known pattern, because the joint has not yet reached temperature. Grinding the starts, or using run-on and run-off tabs, removes it as a category rather than reducing it.
Incomplete Penetration: When the Root Is Not Reached
The weld fails to reach through the full joint thickness. Unlike most defects on this page, the root cause is often in the weld design rather than the welding: an excessive root face, too narrow a groove angle, or a root gap that was specified but not achieved in fit-up.
Setting-driven causes overlap with incomplete fusion — current too low, travel too fast — and a wrong bead sequence can leave the root unfused on a multi-pass joint. The distinction matters if the part is to be repaired: correcting a groove dimension is a different job from correcting a parameter.
Spatter: Beyond the Cosmetic Problem
Spatter is molten metal thrown clear of the pool and adhering to the surrounding surface. It is usually dismissed as cosmetic. In a sheet metal shop it is a cost and a finishing risk.
Every spatter particle is a manual removal task, and cleaning time is a line item on fabricated assemblies. More serious is what happens when it is not fully removed. Under powder coating or paint, a spatter particle can create a pinhole, a blister at the bake, or a local adhesion failure that only appears after the part has been in service. On parts with threads, sliding surfaces or mating faces, spatter is a fit problem rather than an appearance problem.
Causes are almost entirely setting-driven: a mismatch between voltage and wire-feed speed, wrong polarity, the wrong gas mixture, damp wire, or a worn contact tip. Pulse transfer substantially reduces it where the process allows.
Overlap: Metal That Sits Without Bonding
Overlap is weld metal that flows over the parent surface and freezes there without fusing to it — the mirror image of undercut, where material sits above the surface instead of being missing below it. It leaves a step at the fusion line.
It is setting-driven: current too low, travel too slow, torch angle too flat, or deposition rate above what the pool can absorb. The consequence is a stress concentration and, in a corrosive environment, a crevice at the overlap edge that will not be reached by a coating. On stainless and galvanised work that crevice is a corrosion site, not just a cosmetic flaw.
Distortion: the Defect the Design Often Causes
Distortion is not a defect of the weld itself, but on sheet metal assemblies it is often the one that decides whether the part fits. It appears as angular change along a fillet, longitudinal shrinkage that shortens a frame, bowed panels, or rippling in thin sheet.
Causes split across all three groups. Heat input and welding sequence are setting and preparation issues, and they respond to interleaved or backstep sequences and to rigid clamping. But weld size and weld layout are design issues, and they are the ones that are missed. A fillet specified larger than required does not add useful strength — it only adds heat, and roughly doubles the distortion for the same joint. Two small welds placed far apart distort less than one large weld, and a weld placed asymmetrically on a section will always bend the part.
The practical rule: if a part distorts consistently, look at how many welds it has, how large they are and where they sit before changing anything about how they are made.

Which Detection Method Finds What
No single inspection method covers every defect type. Each one has a blind spot, and choosing the wrong one is how a defect survives to the customer.
| Method | Finds | Blind spot |
|---|---|---|
| Visual (VT) | Undercut, overlap, surface porosity, bead profile, dimensional error | Anything below the surface; results depend on the inspector |
| Dye penetrant (PT) | Surface-breaking cracks, pores and lack of fusion | The indication must be open to the surface; rough or porous surfaces are unsuitable |
| Magnetic particle (MT) | Surface and near-surface cracks | Ferromagnetic materials only — not applicable to austenitic stainless steel or aluminium |
| Ultrasonic (UT) | Internal planar defects: cracks, lack of fusion, incomplete penetration | Poor at detecting rounded porosity; needs access and a suitable surface |
| Radiography (RT) | Internal volumetric defects: gas porosity, slag inclusions | A planar defect that is not aligned with the beam can pass undetected |
That last row is the one that surprises buyers. Radiography is an excellent tool for porosity and slag, and a poor one for a tight crack running parallel to the beam. If a drawing calls for radiographic testing on a joint where the real risk is lack of fusion, the inspection method and the risk do not match.
First Root Cause to Check, and the Preventive Action
Most weld defects have one dominant cause and several minor ones. Working through the dominant cause first is what keeps repair time down.
| Defect | How it presents | First thing to check | Preventive action |
|---|---|---|---|
| Porosity | Surface pits or internal worm tracks | Gas coverage and contamination | Shield flow in range, no draught across the arc, joint faces free of oil, paint, rust and moisture, wire dry |
| Lack of fusion | Linear indication along the fusion line | Heat input and torch angle | Raise current or slow travel, grind starts and previous beads, correct the work angle so the arc points at the root |
| Slag inclusion | Elongated indication between passes | Interpass cleaning | Chip and grind between passes; the defect is almost always cleaning discipline rather than a setting |
| Undercut | Notch along the weld toe | Voltage and travel speed | Reduce voltage, moderate travel speed, limit weave width; the notch is a stress raiser and is often rejectable on its own |
| Centreline cracking | Crack along the weld centre | Restraint, bead profile and filler choice | Use a crack-resistant filler, fill the crater at the end of the run, keep the bead slightly convex, reduce restraint where the design allows |
| Hydrogen cracking | Crack in the heat-affected zone, often delayed | Hydrogen source, hardness and restraint | Preheat to the level the carbon equivalent calls for, use low-hydrogen consumables held in a heated quiver, control interpass temperature |
| Burn-through | Hole or excessive penetration on thin sheet | Heat input versus section thickness | Pulse transfer, copper backing, higher travel speed, or a smaller root gap |
| Excessive spatter | Metal droplets around the weld | Voltage to wire-feed mismatch, stick-out | Retune the arc, shorten stick-out, clean or replace the contact tip |
The distinction worth holding onto is between defects caused by settings and defects caused by preparation or discipline. Slag inclusion, porosity from contamination and lack of fusion at a start are preparation failures and no amount of parameter tuning will cure them.
Repair or Reject?
Repair follows a fixed sequence: locate the full extent of the defect, remove it completely by grinding or gouging, clean the excavation, re-weld to the original procedure, re-inspect, and record what was done. The step that gets shortened under schedule pressure is the first one. Removing only the visible part of a defect leaves the root of it behind, and the repair fails in the same place.
Whether a defect is rejectable or repairable is not a shop-floor opinion. It is set by the acceptance level named in the drawing or contract — for steel, ISO 5817 defines quality levels B, C and D, and the same indication can be acceptable at one level and rejectable at another. That is why the acceptance level belongs on the drawing. Without it, a perfectly reasonable weld can be rejected against an unstated expectation, or a marginal one accepted on a part that needed better.
There are cases where repair is not the right answer at all: when the defect is widespread enough that the repair heat would degrade the surrounding material, when there is no access to excavate properly, or when the part is cheap enough that remaking it is faster and more reliable than a repair that will be inspected twice.
FAQ on Common Welding Defects
Can porosity be repaired by welding over it?
Sometimes, but it is the wrong default. Grinding out to sound metal and re-welding is reliable; welding over porosity frequently re-forms it because the source, usually gas coverage or contamination, has not changed.
Which defects are rejectable rather than repairable?
That is set by the acceptance level in the applicable standard, most commonly ISO 5817 for steel, with quality levels B, C and D. A defect that is acceptable at level D can be rejectable at level B, so the level needs to be on the drawing rather than assumed.
Why do cracks sometimes appear hours after welding?
Hydrogen induced cracking is delayed by nature: hydrogen diffuses to the hard heat-affected zone over time. That is why inspection timing matters, and why a weld that looked sound at the end of the shift should still be re-checked later on crack-sensitive material.
Which defects matter most on a structural part?
Planar defects — cracks, lack of fusion, incomplete penetration — because they concentrate stress and can propagate. Gas porosity of the same measured size is usually less severe, which is why inspection methods are chosen by the defect type expected rather than by convenience.
Can distortion be corrected after welding?
It can often be straightened, by pressing or by local heat, but every correction adds stress and can leave the part dimensionally unstable. Preventing distortion through weld size and sequence is more reliable than correcting it afterwards, and on a formed enclosure panel it also preserves the surface.
Questions about a specific part are usually faster to answer against the drawing — send it through the route below.
Next step. Send the drawing for a sheet metal welding service. We confirm the process route and the achievable dimension before quoting, so the numbers describe this part rather than an average. Useful background: welding inspection methods, weld quality standards and inspection, distortion control techniques and weld groove design and preparation.
What stands behind this quotation
- Manufacturing since 20162,500 m² Ningbo plant — 3 laser cutting machines (including newer TRUMPF), 4 CNC press brakes and 10 welding stations.
- Shipped to more than 30 export marketsEnclosures, cabinets and formed parts supplied to OEM buyers across Europe, North America and Asia.
- 123 documented product casesMedical device housings, HVAC and heat pump enclosures, agricultural and livestock equipment, industrial hydraulics, material handling trolleys and EV charging cabinets.
- Factory evidence you can checkTUV Rheinland audit reference MIC-ASI243729 and Bureau Veritas reference MIC-ASR263630 available for buyer review on request.
Before you send drawings: project confidentiality is default · first-article inspection is carried out before a batch continues · pricing is staged from prototype quantity to repeat volume · pre-shipment photos and packing records are prepared when the project needs them.